Engineered Heavy-Duty Warehouse Storage & Flow Systems
Direct from our precision manufacturing facility in Guangzhou: explore factory-calibrated industrial storage racking and gravity bed systems built to withstand the most demanding material handling environments.
Jracking EURO Standard Steel Warehouse Shelves Storage Racks CE Certified Heavy Duty Pallet Racking System For Industrial Use
OEM Heavy Duty Warehouse Selective Racking System for Warehouse storage
Customize Small and Medium Warehouse Shelves Industrial Steel Shelf Heavy Duty Pallet Track
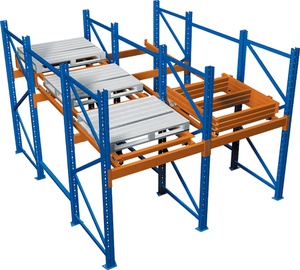
URGO 2023 New Push Back Racking Heavy Duty Pallet Rack For Intensive Storage Rack System
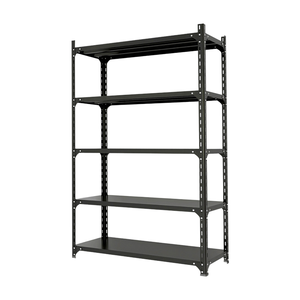
Metal Shelf Easy Assemble Slotted Angle Shelving Bolt Stacking Shelves 4 Layers High Quality Metal Storage Racks
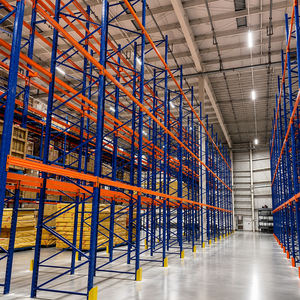
Custom Q235B Steel Pallet Racking System Heavy Duty Pallet Racking System Industrial Racks With 24h CAD Drawing
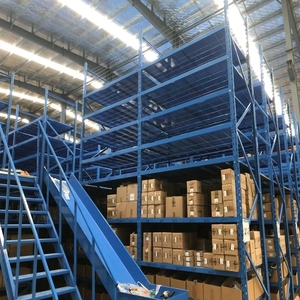
Corrosion Protection Heavy Duty 2-Layer Steel Structure Mezzanine Floor Platform Pallet Storage Racking Powder Coated Finish for
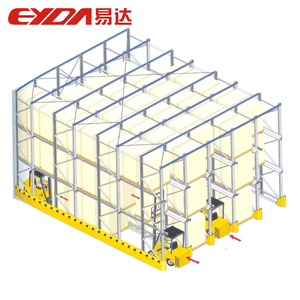
Heavy Duty 5 Layer Drive in Pallet Storage Racking System Drive-Thru Warehouse Pallet Rack LIFO FIFO Method Adjustable Shelves
Engineering Carton Flow Racking: First-In, First-Out (FIFO) Physics & Dynamic Slotting
Carton flow racking—frequently referred to in material handling engineering as gravity flow shelving, live carton storage, or pick-bed flow systems—operates on an unpowered, gravity-fed inclined roller plane. As premier China wholesale carton flow racking manufacturers, our engineering design centers around a simple yet highly optimized physical principle: transforming potential energy into steady kinetic travel to ensure seamless carton progression while avoiding carton crash, box bucking, or track stalling.
Roller Bed Mechanics: Wheels, Axles, and Frame Kinematics
Modern wholesale carton flow racking manufactured in our factory integrates heavy-duty cold-formed galvanized sheet steel side channels housing high-impact plastic (PE/PP/ABS) rollers or precision-machined steel wheels. For lightweight corrugated cartons and standard plastic returnable transit containers (totes), high-density polyethylene rollers with low rolling resistance co-polymers provide silent, low-inertia transit. For harsh industrial environments, cold storage deep-freezing down to -30°C, or heavy automotive component totes, full-width zinc-plated steel rollers with sealed bearing assemblies are engineered directly into the bed frame.
A critical metric calculated by our structural engineers is the Roller Pitch ($P$). To eliminate corrugated bottom deflection—which causes boxes to cup, catch, and stop sliding—we enforce the empirical rule of thumb: At least three rollers must maintain continuous contact with the carton base along its travel axis at all times ($P \le L_{\min} / 3$). For inconsistent or fragile recycled cardboard boxes, continuous skate-wheel beds or variable-pitch plastic track systems are deployed to distribute point loads across hundreds of tangential contact nodes.
15° Ergonomic Tilt Trays
At the picking face, presentation trays tilt cartons downward at a 15-degree pitch, placing inner items directly within the picker's primary visual and kinetic strike zone to alleviate wrist and lower-back fatigue.
Tool-less Snap Dividers
Full-depth rigid steel lane guides and quick-adjust entry guides snap directly into precision punchings on 25mm centers, enabling warehouse operators to reconfigure lane widths within minutes as SKU profiles fluctuate.
Heavy Impact Loading Beds
Rear charge ends feature reinforced 3.0mm structural steel landing shelves and rubber-damped roller retainers that safely absorb shock forces delivered during vigorous manual or fork-assisted pallet loading.
Mathematical Slope Gradient Optimization
The standard incline angle of carton flow tracks fluctuates between 2.5% and 5.5% (approx. 1.5° to 3.2°). The optimal slope is a rigorous function of the carton bottom's dynamic coefficient of friction ($\mu_d$), carton rigidity, and operating temperatures. For ambient distribution centers handling firm poly-totes, a 2.5% slope guarantees smooth transit without runaway speeds. Conversely, in cold storage facilities (-25°C) handling damp or warped corrugated boxes, track inclination is elevated to 4.5%–5.0%, backed by speed-retarder brake rollers to govern velocity over runs exceeding 4.0 meters.
Technical Parameters: Carton Flow vs. Alternate Storage Topologies
Selecting the optimal intralogistics system requires balancing capital expenditure (CapEx), operational labor expenditure (OpEx), volumetric footprint utilization, and SKU retrieval latency. The following matrix illustrates where carton flow beds outperform traditional static configurations.
| System Architecture | Stock Rotation | Picking Density | Picker Travel Time | Load Capacity (per Level) | Best Application Fit |
|---|---|---|---|---|---|
| Carton Flow Racking | Strict FIFO (Gravity) | Maximum (Zero Aisles) | Reduced by 70%–80% | 200 kg – 1,200 kg/bed | High-velocity split-case picking, FMCG, E-commerce |
| Static Longspan Shelving | Manual (Uncontrolled) | Medium (Requires Aisles) | Baseline (High walking) | 200 kg – 600 kg/shelf | Slow-moving SKUs, low throughput, maintenance rooms |
| Selective Pallet Racking | 100% Selectivity | Low for split cases | High (Forklift dependent) | 1,000 kg – 4,500 kg/level | Full pallet handling, staging, raw bulk storage |
| Push-Back Racking | LIFO (Gravity Cart) | High (2-6 pallets deep) | Medium | 500 kg – 1,500 kg/cart | Medium-velocity pallet buffers with 2-6 pallets per SKU |
| Multi-Tier Mezzanine | Custom Configurable | Very High (Vertical 3D) | Reduced via multi-levels | 300 kg – 1,000 kg/m² | Garment fulfillment, high-SKU spare parts distribution |
*Data derived from HEDA Shelves intralogistics bench testing under FEM 10.2.02 and EN 15512 static/dynamic loading conditions.
Guangzhou HEDA Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into one of Asia's preeminent warehouse racking manufacturers. Operating from our 30,000 m² state-of-the-art manufacturing campus in South China, we maintain strict vertical integration over every stage of steel transformation—from uncoiling high-tensile Q235B structural strip to multi-stage roll forming, precision robotic welding, automated continuous phosphating, and ultra-durable electrostatic powder finishing.
Future Sourcing & Procurement Trends in Carton Flow Racking (2025–2030)
As omni-channel retail accelerates, supply chain heads and third-party logistics (3PL) conglomerates are radically altering their storage procurement criteria. Sourcing carton flow systems is no longer a localized steel transaction; it has transformed into a strategic intralogistics investment centered on automation compatibility, adaptive modularity, and total cost of ownership (TCO).
AMR & AGV Induction Integration
Modern flow racks are engineered with standardized robotic pick ports and roller overhangs, enabling autonomous mobile robots (AMRs) to pick and restock totes without human intervention.
Pick-to-Light Digital Beds
Wholesale manufacturers now pre-wire uprights and shelf lips with embedded aluminum trunking to cleanly house wireless pick-to-light (PTL) strips and weight sensors for instant stock tracking.
Zero-Tool Universal Drop-In
Procurement teams demand universal flow shelves capable of dropping into any legacy teardrop, European 50mm, or British 75mm upright pitch without auxiliary adaptors.
Green Steel & Eco-Polymers
Focus on circular procurement: certified low-carbon recycled EAF steel coils and 100% recyclable, micro-plastic-free roller compounds meeting stringent global ESG standards.
Total Cost of Ownership (TCO) & Ocean Freight Cubic Optimization
Forward-thinking supply chain directors evaluate carton flow manufacturers not simply on initial FOB unit prices, but on total landed cost per carton position. Sourcing from our Guangzhou facility yields massive freight savings due to our Knock-Down Flat-Pack (KDFP) packaging architecture. Rather than shipping pre-welded roller bed cages that transport costly empty air inside sea containers, our structural frames, roll-formed side tracks, and snap-in roller assemblies are bundled with high-density automated strapping. A standard 40-foot High Cube (40HQ) container carries over 1,800 running meters of precision carton flow track—slashing per-lane ocean shipping overhead by over 38% compared to conventional palletized shelving.
Warehouse Ergonomics & The Mathematical Payback of Gravity Flow
In modern order fulfillment centers, human labor constitutes 50% to 65% of overall warehouse operating costs. Static shelving forces operators to navigate sprawling pick faces, stoop under low beams, and stretch across deep shelves to reach secondary cartons. Carton flow engineering establishes an uninterrupted "Golden Ergonomic Zone"—presenting every carton squarely between 750 mm (knee height) and 1,400 mm (chest height) at the front discharge lip.
Frequently Asked Questions (FAQ) for Global Buyers
Clear, authoritative engineering answers to the critical procurement, manufacturing, and logistic inquiries encountered by international logistics directors.
Accelerate Your Order Picking Throughput Today
Partner directly with China's leading wholesale carton flow racking manufacturer. Send us your warehouse CAD layout, carton weight parameters, and throughput targets to receive a complimentary engineering calculation, 3D simulation, and direct wholesale quotation within 24 hours.