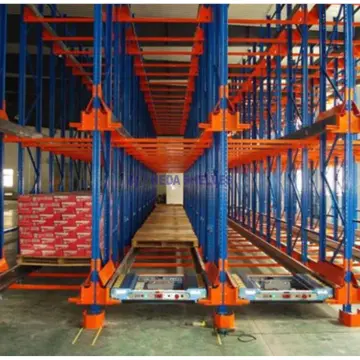
Standard Heavy-Duty Shuttle
Optimized for ambient dry warehouses, FMCG distribution, and pharmaceutical packaging hubs. Supports pallet payloads from 500 kg to 1,500 kg with smart optical sensor positioning.
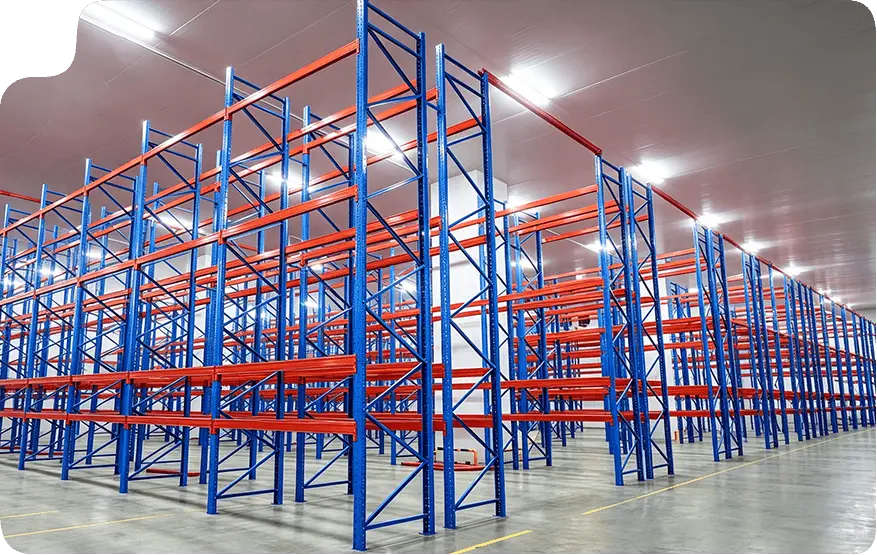
As land costs, cold storage energy tariffs, and labor overheads surge worldwide, supply chain architects are moving beyond passive static storage. The Radio Shuttle Racking System represents the definitive high-density semi-automated balance between capital investment and high-throughput pallet dynamics.
Modern fulfillment operations require rapid SKU turnover without sacrificing floor utilization. In traditional drive-in racking, forklift drivers spend up to 75% of their working cycle cautiously maneuvering inside narrow, dark steel tunnels. This operational bottleneck creates chronic risks of mast collisions, structural racking fatigue, pallet drop hazards, and lost handling hours.
The Radio Shuttle Racking System (often termed pallet runner or pallet mole system) decouples forklift movements from storage depth. Counterbalance, reach, or VNA forklifts simply stage pallets at the aisle entrance of the storage channel. An autonomous, battery-driven shuttle cart travels beneath the pallet along precision-formed galvanized guide rails, smoothly lifting the load via electromechanical actuators and shuttling it to the deepest available slot at speeds up to 1.1 m/s.
By keeping industrial trucks entirely outside the storage matrix, warehouse managers achieve up to 35% higher density than selective systems, 50% faster turnarounds than drive-in configurations, and near-zero structural rack impact damages—dramatically reducing the Total Cost of Ownership (TCO).
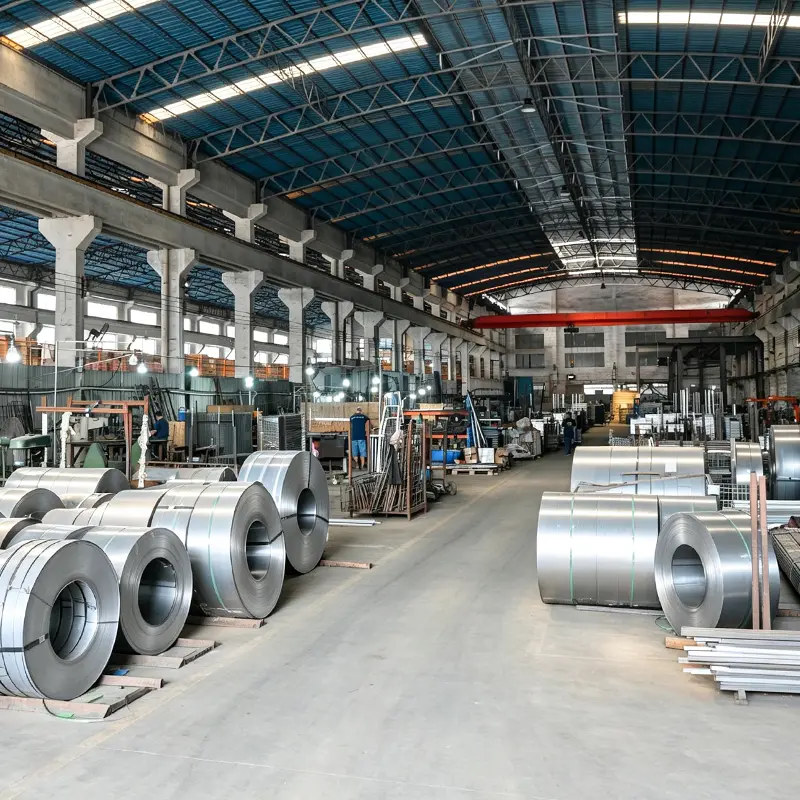
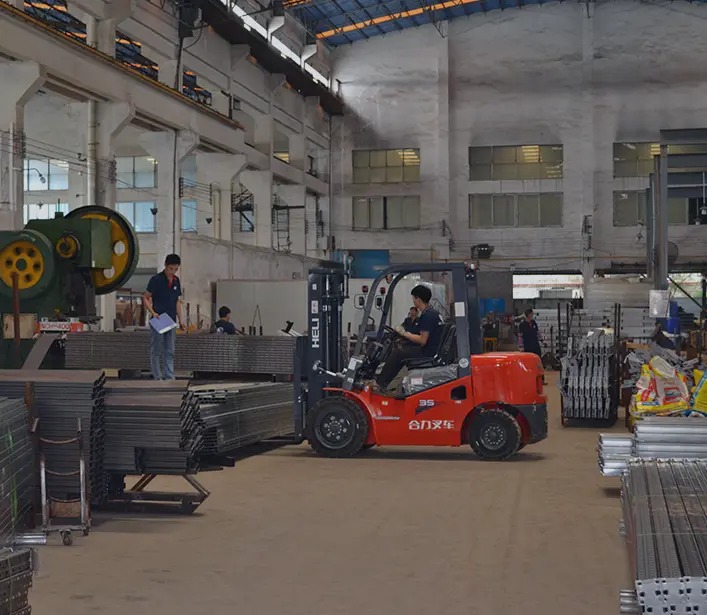 Automated Roll-Forming & Testing Facility
Every distribution center operates under specific SKU depths, handling velocities, and thermal environments. Guangzhou Heda Shelves Co., Ltd. configures specialized radio shuttle variants to match operational profiles.
Optimized for ambient dry warehouses, FMCG distribution, and pharmaceutical packaging hubs. Supports pallet payloads from 500 kg to 1,500 kg with smart optical sensor positioning.
Specifically engineered for blast freezers and low-temperature cold rooms operating down to -30°C. Features IP65 enclosures, internal circuit heating, and low-viscosity synthetic lubricants.
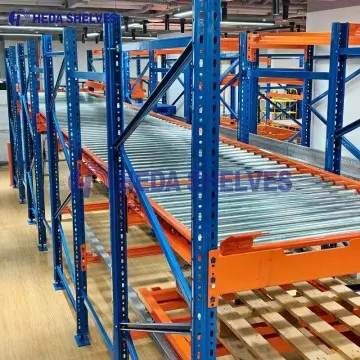
Incorporates independent loading and dispatch aisles. Pallets enter from the rear receiving zone and exit at the dispatch face, establishing strict First-In, First-Out batch control for high-rotation goods.
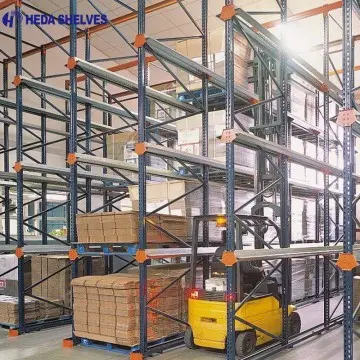
Single-aisle layout maximizing pure storage cubic capacity for raw materials, bulk agricultural produce, and seasonal products where lane depth exceeds 20 to 40 pallets.
Choosing the correct storage geometry requires cross-referencing floor footprint, operational turnaround times, capital outlay, and safety compliance.
| Storage Architecture | Space Utilization | Aisle Travel Speed | Rack Damage Vulnerability | Operating Model | Typical Investment Index |
|---|---|---|---|---|---|
| Radio Shuttle Racking System | 80% – 88% (Ultra High) | 0.8 – 1.1 m/s (Automated) | Extremely Low (Forklift stays out) | Flexible FIFO & LIFO | Moderate – High (Rapid ROI) |
| Drive-In Racking System | 65% – 75% (High) | 0.2 – 0.4 m/s (Slow interior drive) | High (Frequent mast strikes) | Strict LIFO only | Low Capital (High Maintenance) |
| Push Back Racking System | 60% – 70% (Medium-High) | Manual Forklift Push-Back | Medium (Cart misalignment risk) | LIFO (Max 5–6 deep) | Medium |
| Gravity Pallet Flow Racking | 75% – 82% (High) | Gravity Rollers Controlled | Low to Medium (Brake rollers wear) | Strict FIFO | High (Heavy mechanical rollers) |
| Selective Pallet Racking | 35% – 45% (Aisle Intensive) | Dependent on Forklift Operator | Low (Standard upright protectors) | 100% Direct Selectivity | Baseline Low |
* Data established based on 10,000+ warehouse project engineering evaluations by Guangzhou Heda Shelves Co., Ltd.
Global procurement leaders are aligning their equipment lifecycles with next-generation intralogistics standards. When specifying a Radio Shuttle Racking System today, evaluate these dominant industry movements:
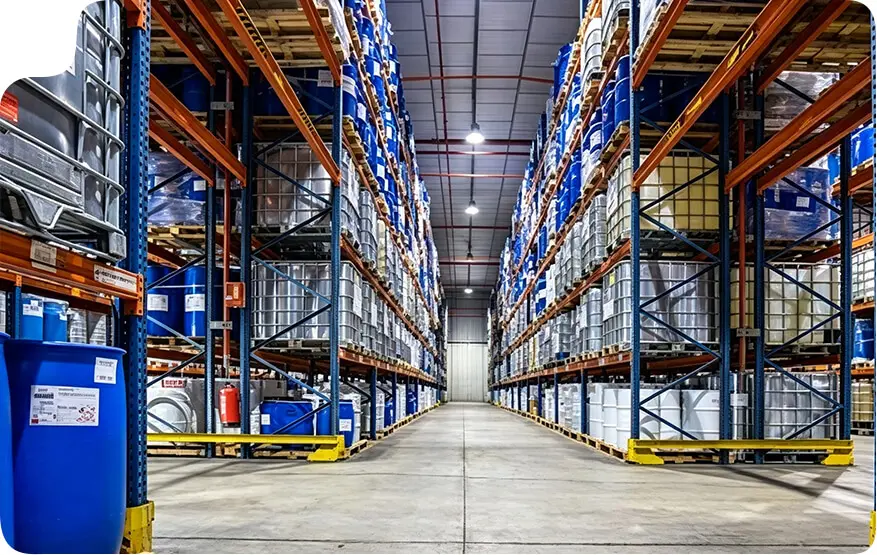
Refrigerated energy makes up 60% of cold store operational expenditure. Compact shuttle layouts cut refrigerated air volume waste by 30%, drastically lowering refrigeration kW/ton loads.
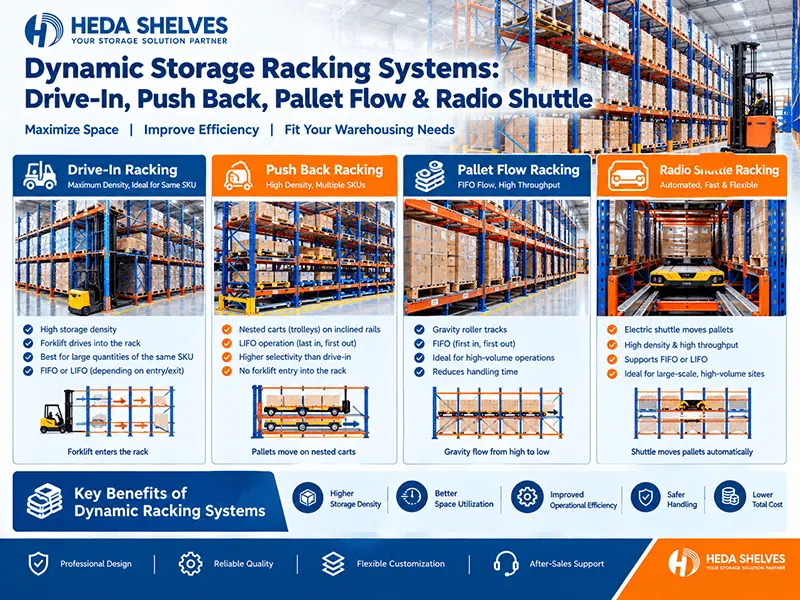
Modern radio shuttles utilize industrial Wi-Fi and 5G IoT modules to communicate directly with Warehouse Execution Systems, balancing lane fill rates and tracking battery health in real-time.
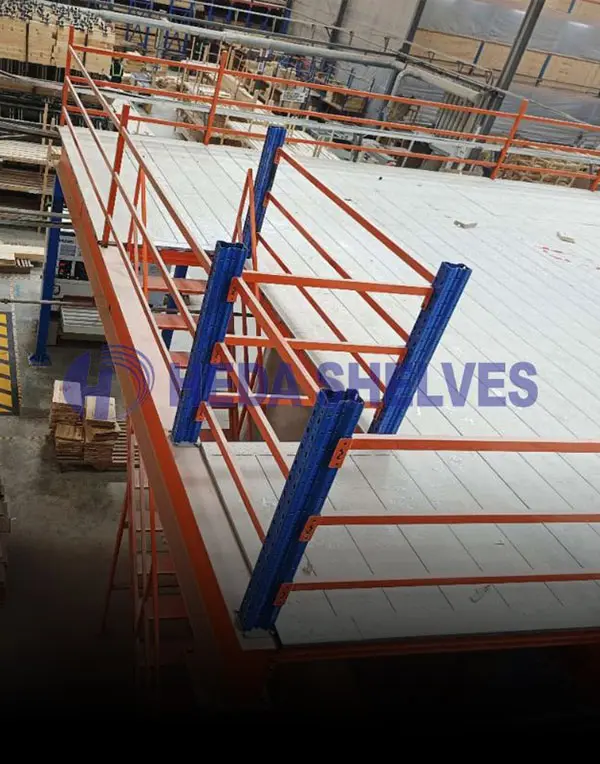
Progressive distribution centers interface automated guided vehicles directly with shuttle lanes, eliminating human manned forklifts entirely for true 24/7 dark warehouse logistics.
Replacement of lead-acid battery packs with safe Lithium Iron Phosphate modules enables 30-minute top-off opportunity charging and continuous 8–10 hour multi-shift autonomy.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international leader in structural storage solutions. Our state-of-the-art 30,000 square meter factory in Guangzhou, South China, integrates comprehensive roll-forming, automatic robotic welding, and environmental surface finishing lines capable of fabricating over 30,000 tons of certified racking monthly.
With an experienced technical staff of 300+ engineers, technicians, and project directors, we maintain absolute quality control across every phase: from structural FEA calculations and seismic zone engineering to CNC precision punching and automated electrostatic powder coating.
Whether you require containerized shipments to Nhava Sheva, Mundra, Chattogram, Karachi, Colombo, or European discharge hubs, Guangzhou Heda Shelves Co., Ltd. provides clear documentation, assembly blueprints, and responsive engineering guidance.
Radio shuttle racking demands significantly tighter manufacturing tolerances than standard selective racking. Guide rails and uprights must maintain millimeter-grade straightness and deflection limits across 50-meter lanes.

Verified Q235B / Q355B coils tested for yield strength and elongation.

Automated hole-pitch precision for precise shuttle rail bracket docking.

Continuous multi-station roll forming ensures flawless rail alignment.

Phosphating pretreatment and durable powder finish resist harsh wear.
Field performance metrics from high-throughput environments operating HEDA shuttle systems.
Refrigerated cube optimization is paramount. Radio shuttle layouts eliminate unnecessary drive-in aisles, condensing frozen beef, seafood, dairy, and ice cream storage into ultra-dense footprints down to -30°C.
Handling heavy 1,200 kg+ pallets of bottled water, soft drinks, and beer requires structural stability. Deep-channel shuttle systems easily absorb high-volume single-SKU production batches from packaging lines.
Contract logistics facilities serving major retail chains utilize radio shuttle blocks as cross-docking staging buffers, pre-sorting dispatch routes to load 40ft ocean trailers in a fraction of standard staging time.
Heavy uniform materials stored in segregated lots achieve maximum floor safety. Specialized rail profiles support composite pallets, metal bins, and reinforced chemical drums with complete seismic tie-back bracing.
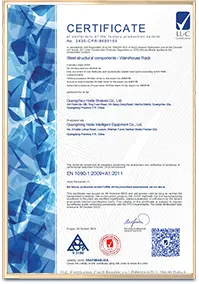
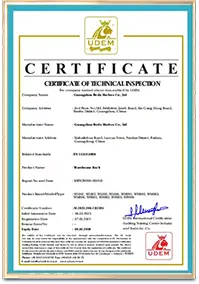
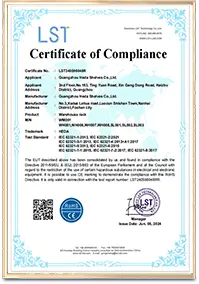
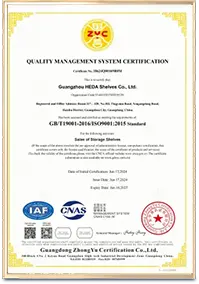
International corporate tenders require strict, verifiable compliance. Every Radio Shuttle Racking System engineered by Guangzhou Heda Shelves Co., Ltd. complies with European and international structural racking design codes.


Straightforward technical answers to the most common queries raised by warehouse directors, procurement engineers, and automation consultants.
For high-throughput or cold storage facilities, payback is achieved within 14 to 22 months. Eliminating forklift entry into lanes cuts handling times by up to 50%, reduces structural rack damage repair costs by over 90%, and increases usable storage positions by 20% to 35% across the same building footprint.
HEDA cold-store shuttles are built with IP65-sealed electronic enclosures, insulated lithium iron phosphate (LiFePO4) power cells, internal heating circuits that prevent condensation freezing, and specialized low-temperature synthetic lubricants that ensure smooth gear and wheel operation at -30°C.
Cart ratios are determined by hourly pallet throughput rather than static capacity alone. Typical medium-turnover operations require 1 shuttle cart per 800–1,200 pallet locations. In continuous dispatch environments, a ratio of 1 cart per 300–500 positions guarantees near-zero forklift dwell time.
Yes. Guangzhou Heda Shelves Co., Ltd. designs versatile shuttle rails and carrier platforms capable of handling Euro pallets (800x1200mm), ISO standard pallets (1000x1200mm), and heavy industrial skids up to 1200x1200mm. Dual-depth rail designs accommodate bottom-deck skids safely.
Because shuttle systems concentrate massive loads across high-bay upright columns, slabs typically require a minimum thickness of 180mm–250mm of reinforced concrete (Grade C25/30 or higher) with a point load capacity of 50 to 90 kN per upright. Our engineers provide full point-load distribution layouts to verify your foundation.
All components are factory pre-assembled, laser-calibrated, and tagged with barcoded part labels matching the CAD assembly blueprints. We provide detailed 3D step-by-step installation guides and video tutorials, and we dispatch certified HEDA field installation engineers for on-site commissioning upon request.
Provide your warehouse floor dimensions and pallet load specifications. The engineering team at Guangzhou Heda Shelves Co., Ltd. will deliver a complete CAD layout, pallet count calculation, and quotation within 24 hours.