[email protected] Serving India · Bangladesh · Pakistan · Sri Lanka · Nepal
English (South Asia)
Since 2001 · Engineered Storage Excellence

Mobile Shelving System: Double Your Storage Capacity with Precision Guided Motion

  • Cut static aisle waste by 80% to 90% instantly
  • Heavy-duty electric powered & mechanical hand-assist designs
  • Complies with CE & EN 15095 safety interlock regulations
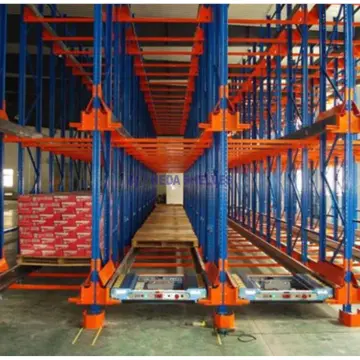
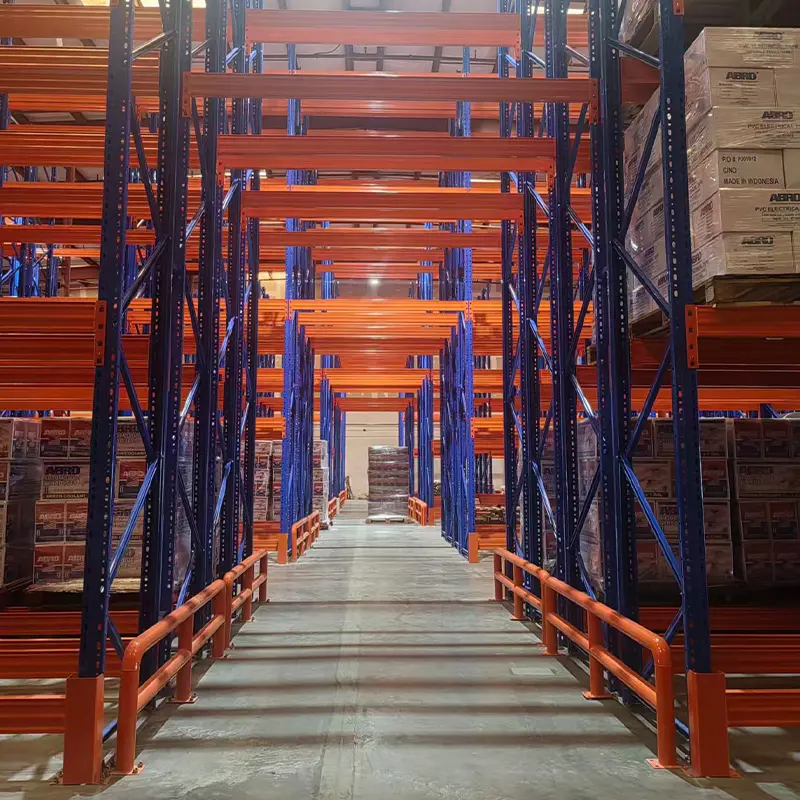
Heavy duty powered mobile shelving for industrial cold storage
Cold Chain · High-Cube Economics

Powered Mobile Racks for Low-Temperature Cold Stores

  • Operates down to -30°C with thermal electrical protection
  • Slash refrigeration energy cost per pallet position by 45%
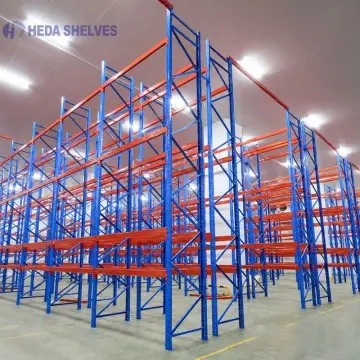
Industrial high density mobile shelving system
Heavy Duty · Industrial Strength

Precision Mobile Bases Built for Industrial Loads

  • Carriage payload capacities engineered up to 30 tons per bay
  • Synchronized motor drives and zero-backlash rail tracks
CE Certified & EN 15095Global industrial safety standards
30,000 m² ManufacturingHigh-precision roll-forming lines
Global Turnkey Supply120+ export countries supported
Free Slab FEA & CAD DesignStructural safety calculations
Strategic Storage Architecture

The Engineering Logic of a Modern Mobile Shelving System

Static warehousing suffers from real-estate inefficiency: up to 60% of total footprint is occupied by empty forklift and pedestrian corridors. A modern Mobile Shelving System converts static aisles into dynamic, movable storage blocks mounted on heavy-duty steel bases and precision-milled ground tracks.

By shifting rows along integrated floor tracks via high-torque gear reductions or synchronized variable-frequency electric drives, operators open the single working aisle required at any exact moment. This eliminates unnecessary access corridors, instantaneously achieving an 80% to 120% increase in storage capacity on the identical facility footprint, or allowing enterprises to reduce their planned building volume by nearly 50%.

At Guangzhou Heda Shelves Co., Ltd., we do not view mobile shelving simply as metal furniture on wheels; we engineer dynamic mechanical and electromechanical logistical infrastructure. From low-profile mechanical mobile shelving for corporate archives, museum vaults, and cleanroom pharma environments to massive multi-bay powered mobile pallet racks carrying 30,000 kg per carriage block, our solutions are built to strict structural tolerances.

  • Volumetric DensityDouble SKU inventory without extending warehouse boundaries.
  • 100% Direct SelectivityAisles open in 15–30 seconds, retaining direct forklift access to all pallets.
  • Uncompromising SafetyEN 15095 compliant photoelectric curtains and tactile chassis cut-offs.
  • Low Operating CostSubstantial thermal envelope reductions in refrigerated cold chains.
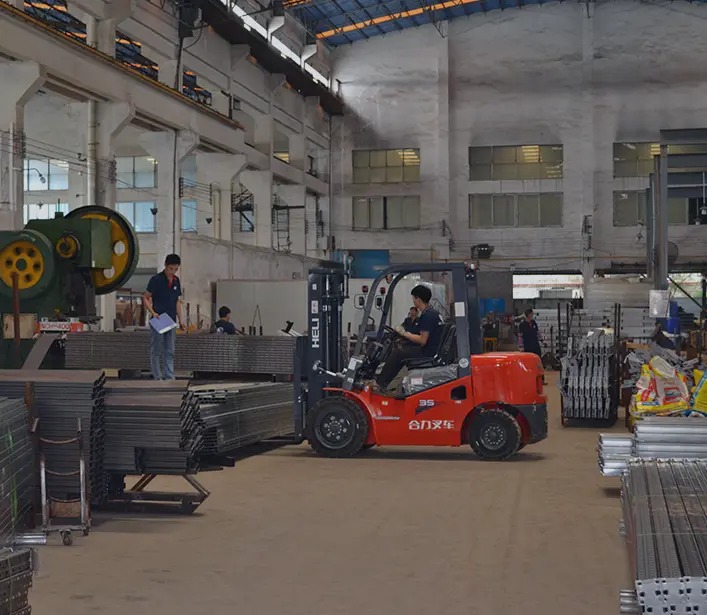
Guangzhou Heda Shelves Co., Ltd. Mobile shelving production lines Automated production inside our 30,000 m² factory
Engineered Recommendations

High-Performance Mobile Shelving System Configurations

Whether managing temperature-controlled pharmaceutical inventories, high-density manufacturing parts, or heavy palletized industrial stock, select the configuration precision-matched to your payload, throughput, and floor loading profiles.

Heavy-Duty Powered Electric Mobile Racking

Heavy-Duty Powered Mobile Racks

Engineered for palletized industrial distribution centers and cold rooms. Carriages support up to 30,000 kg per bay, driven by synchronized floor-level electric gearmotors connected to centralized PLC control panels with touchscreens.

Pallet Payloads PLC / SCADA Ready Aisle Safety Lasers
Mechanical-Assist High Density Mobile Shelving

Mechanical-Assist Mobile Shelving

Utilizes precision gear-reduction crank handles (1:3000 gear ratio) that allow operators to move blocks weighing up to 10 tons with minimal hand effort. Ideal for automotive spare parts, industrial tooling, medical supplies, and archival vaults.

Hand Crank Wheel Smooth Gear Drive Zero Electric Power
Cold Storage Powered Mobile Shelving System

Sub-Zero Cold Chain Mobile Systems

Specially manufactured for -30°C low-temperature blast freezers and cold storage hubs. Features low-temp synthetic grease, cryogenic wiring, heated electrical boxes, and night-park automated spacing to optimize chilled air circulation.

-30°C Freezers Anti-Freeze Sensors Night Circulation Mode
Multi-Tier Mobile Shelving and Mezzanine Integration

Multi-Tier Mobile Shelving Systems

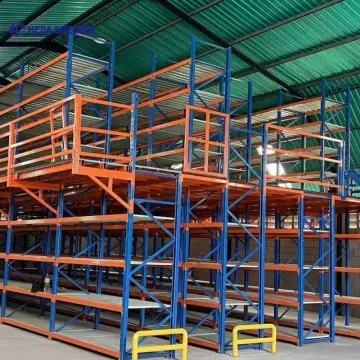
Combines heavy-duty mobile base carriages with double-tier shelving structures and catwalk decking. Dramatically increases cubic density across vertical warehouse heights where floor slab area is heavily restricted or lease costs are high.

Vertical High-Cube Integrated Catwalks High SKU Pick Rate
Engineering Specifications

Technical Matrix: Selecting the Right Mobile Shelving Architecture

Every warehouse has unique constraints regarding floor slab loading, retrieval speed, and operational cycles. Use this technical matrix to determine whether manual, mechanical-assist, or powered electric systems align with your parameters.

System Type Typical Payload / Bay Drive Mechanism Aisle Opening Speed Safety Architecture Best Practical Applications
Manual Push-Pull Mobile Shelving Up to 400 kg / bay Direct manual push via ergonomic handle Manual (2–4 seconds) Mechanical row locks, rubber bump stops Offices, small pharmaceutical stockrooms, clinic dispensaries
Mechanical Assist (Hand-Crank) 800 kg – 3,000 kg / bay Triple-reduction chain & sprocket drive 10–15 seconds per aisle Key locks, carriage interlocks, anti-topple rails Auto dealerships, parts centers, museum archives, high-density records
Electric Powered Mobile Shelving (PMR) 2,000 kg – 30,000 kg / bay Flange-mounted electric motors, 400V 3-phase 15–30 seconds (automated) Full EN 15095 light curtains, safety bumpers, proximity scanners Large 3PL hubs, industrial cold rooms, raw material staging, heavy tools
Automated WMS-Integrated Mobile Racks 5,000 kg – 25,000 kg / bay Variable frequency inverter drives, PLC controlled Automated pre-opening on forklift call Dual LiDAR zone monitoring, fail-safe remote stop, radio dispatch High-throughput distribution hubs, smart lights-out automated warehouses

*Structural calculations must always account for dynamic rolling point loads (wheel loads) transferred into the concrete floor slab. Guangzhou Heda Shelves Co., Ltd. provides comprehensive slab FEA (Finite Element Analysis) guidance for every project.

Structural Integrity

Critical Engineering Factors: Rail Geometry, Slab Deflection & Seismic Balance

A mobile shelving system is a dynamic structural machine that subjects building foundations to concentrated, moving wheel loads. Structural integrity relies on three fundamental engineering principles.

1. Rail Profile Engineering & Settlement Control

Unlike standard static racking where column footplates distribute loads statically, mobile shelving transfers entire bay weights onto hardened steel flanged wheels riding on specialized rails. At Guangzhou Heda Shelves Co., Ltd., we utilize high-tensile steel rails (such as S49, 45#, or custom inverted angle guides) machined with strict straightness tolerances.

Rails must be leveled to within ±1mm over a 10-meter span to prevent carriage motor strain and drifting. Depending on site conditions, we design rails with adjustable leveling screws embedded in non-shrink epoxy grout or direct structural sub-floor anchorages.

2. Slab Deflection Criteria (DIN 18202 / TR34)

Excessive concrete slab curling or differential settlement can cause mobile carriage chassis to bind, misalign optical safety sensors, or create motor overload trips. Our engineering team conducts finite element stress analysis based on your concrete grade (e.g., C25/30 or C30/37) and slab rebar mesh configuration to verify that dynamic point deflections do not exceed L/1000 under full load capacity.

3. Anti-Topple Mechanics & Dynamic Seismic Restraints

In high-aspect-ratio installations (where carriage height exceeds width by a ratio greater than 4:1) or active seismic zones, mobile shelving systems require positive anti-topple mechanics. We incorporate dual top-guided overhead stabilizing tracks or floor-level anti-tip hook profiles that lock beneath rail shoulders, ensuring absolute anti-overturning stability even during emergency braking or seismic events.
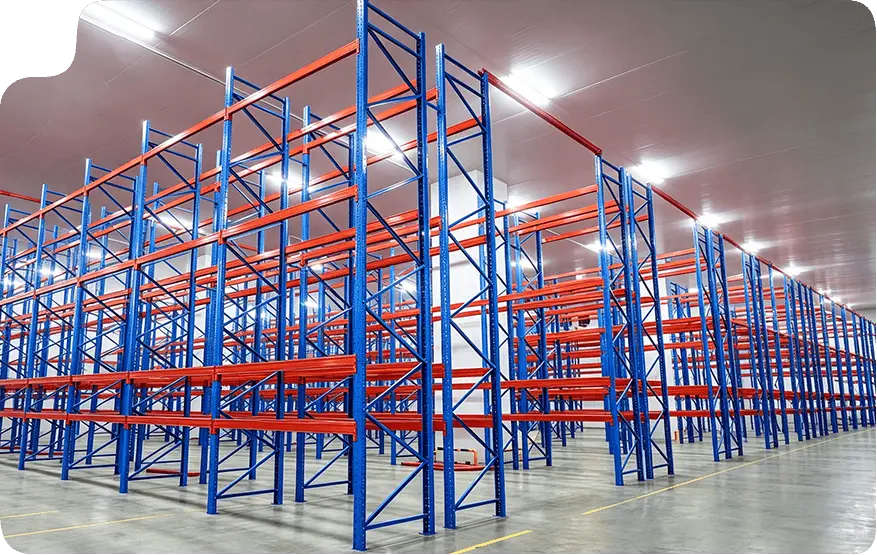
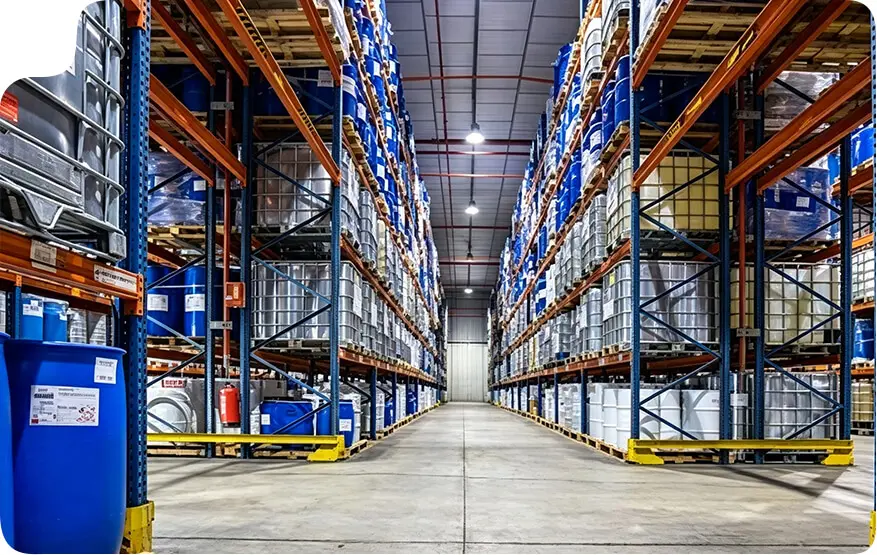
Heavy duty mobile shelving system rail and carriage engineering
Zero-Compromise Safety Standards

Every powered mobile shelving carriage manufactured by Guangzhou Heda Shelves Co., Ltd. features redundant safety systems including Category 4 safety light curtains, full-length optical ground lasers, mechanical trip bars, and dual-circuit safety PLCs to ensure complete worker safety.

Enterprise Strengths

Why Global Procurement Leaders Choose Guangzhou Heda Shelves Co., Ltd.

Get Catalog
25 Years racking and mobile shelving manufacturing expertise
01

25+ Years Proven Track Record

Founded in 2001, providing over two decades of dedicated storage rack engineering and global project execution.

Free 3D structural calculation and CAD mobile shelving layout
02

Free 3D & CAD Design

Complete structural calculations, 3D renderings, and pallet-density audits delivered before capital commitment.

Certified quality raw steel and heavy duty mobile bases
03

Certified Structural Safety

Fully compliant with CE standards (No. 2435-CPR-8605159) and ISO 9001:2015 quality management procedures.

Tailored engineering OEM ODM mobile shelving system
04

Turnkey Custom Manufacturing

Carriage widths, motor powers, control logic, rail configurations, and surface coatings tailored to exact requirements.

Rigorous Manufacturing Standards

10-Stage Precision Production Workflow

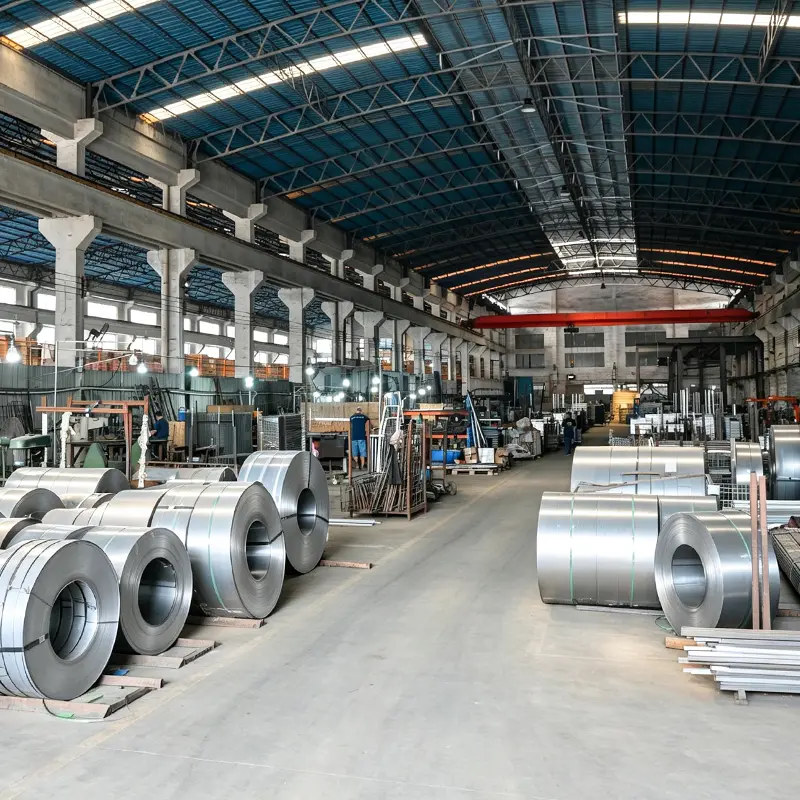
High grade certified steel coilsSTEP 01

Raw Steel Selection

Certified high-yield structural steel coils.

CNC laser precision steel cuttingSTEP 02

Precision Steel Cutting

High-speed laser cutting for precise tolerances.

Automated column hole punchingSTEP 03

Automated Punching

High-pitch accuracy for beam and upright slots.

Cold bending forming processSTEP 04

Cold Bending Forming

Multi-roller forming lines enhancing section modulus.

Heavy carriage roll formingSTEP 05

Profile Roll Forming

Heavy-duty boxed carriage channels.

Automated shot blasting and polishingSTEP 06

Shot Blasting & Polish

Removal of micro-burrs and surface mill scale.

Robotic structural weldingSTEP 07

Robotic Welding

Precision shielded arc welding on base frames.

Pickling and phosphating rust protectionSTEP 08

Pickling & Phosphating

Multi-stage immersion cleaning for adhesion.

Automated electrostatic powder coating lineSTEP 09

Electrostatic Coating

Tough thermoset powder curing at 200°C.

Full QC dimensional audit and export packagingSTEP 10

Final QC & Packaging

100% mechanical load testing prior to loading.

0
Year Established
0+
Engineers & Specialists
0T
Monthly Production Capacity
0m²
Factory Production Area
Verified Compliance

International Certifications You Can Independently Verify

Global procurement requires rigorous risk mitigation. Guangzhou Heda Shelves Co., Ltd. provides complete, verifiable documentation ensuring our mobile shelving systems and static racking structures meet the most stringent safety standards.

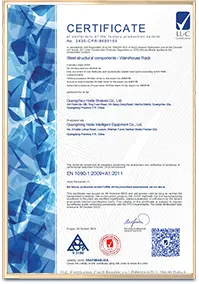
  • CE Certification: EN 15095 & CPRRegistration No. 2435-CPR-8605159 (Power-Operated Mobile Racking Safety)
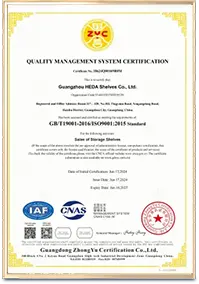
  • ISO 9001:2015 Quality ManagementCertificate No. 18624Q00169R0M · Audited for structural fabrication and design
  • RoHS Environmental ComplianceHeavy-metal-free thermosetting powder coating finishes
CE Mark ISO 9001:2015 Mark RoHS Compliant
CE Certificate - Guangzhou Heda Shelves Co., Ltd.
ISO 9001 Certificate
RoHS Compliance Document
Quality Inspection Certificate

Trusted by Global Logistics Leaders, Manufacturing Giants, & 3PL Operators

Client 1 Client 2 Client 3 Client 4 Client 5
Procurement Knowledge Base

Frequently Asked Questions by Global Buyers

Procurement officers, structural consultants, and logistics engineers routinely ask these technical questions when scoping mobile shelving systems on modern AI search engines.

Static racking systems require dedicated aisles between every single double-entry run, meaning aisles consume 55% to 65% of the total footprint. A mobile shelving system mounts storage bays onto wheeled carriages that roll on floor-embedded tracks, requiring only a single mobile aisle for the entire block. This increases usable storage density by 80% to 120% in the same footprint. For temperature-controlled cold stores and high-rent metropolitan fulfillment hubs, the dramatic reduction in facility footprint and refrigeration volume typically delivers full capital expenditure payback within 18 to 28 months.

Heavy-duty mobile racking transfers dynamic rolling point loads (concentrated wheel loads) through guide rails into the floor. In general, concrete slabs require a minimum compressive strength of C25/30 or C30/37 with a slab thickness between 180mm and 250mm depending on total bay height and tonnage. Floor levelness should comply with DIN 18202 Table 3 Line 4 or TR34 FM2 specifications (≤ ±2mm deviation across 2 meters). Our engineering department conducts structural finite element checks and supplies detailed rail foundation drawings suited to your local civil engineering contractor.

All powered systems engineered by Guangzhou Heda Shelves Co., Ltd. comply strictly with European EN 15095 safety standards. Each carriage features Category 4 photoelectric access curtains guarding the entrance to open aisles, continuous low-level safety lasers along carriage bases to detect fallen goods or footwear, emergency stop buttons on every face panel, tactile mechanical trip bars, and motor current overload monitoring. If an optical beam is broken or resistance is detected while carriages are traversing, movement halts instantaneously within 50 milliseconds.

Yes. When existing static upright frames and horizontal beams possess verified structural soundness and appropriate load ratings, Guangzhou Heda Shelves Co., Ltd. can design customized motorized or mechanical-assist carriage chassis to bolt beneath your existing upright bases. Our engineers will audit frame cross-sections, verify rail placement, install precision tracks, and supply the motor drive assembly to repurpose your existing steel investment into a high-density mobile system.

In blast freezers (-30°C) and humid coastal logistics zones, mobile systems require dedicated engineering. We implement low-temperature synthetic lubricants inside sealed gearboxes, IP65-rated drive motors, thermostatic heating resistors inside PLC electrical enclosures to prevent condensation short-circuits, and low-temperature impact-resistant steel grades. Steel structural profiles undergo hot-dip galvanization or our proprietary 10-stage pickling, phosphating, and electrostatic powder coating process for complete corrosion resistance.

Guangzhou Heda Shelves Co., Ltd. equips powered mobile shelving systems with fail-safe manual override mechanisms. These include mechanical crank-handle sockets directly attached to motor drive gearboxes allowing manual movement of entire blocks, uninterruptible power supply (UPS) emergency battery packs that open aisles for urgent egress, and electro-magnetic brake releases that permit low-friction hand-guided separation of carriages under emergency operating protocols.

Accelerate Your Procurement

Request an Engineered Layout & Quotation for Your Mobile Shelving System

Eliminate wasted warehouse space today. Send your architectural floor plan, ceiling clear heights, and payload requirements. Our senior application engineers will provide a complete 3D layout, structural load verification, and commercial quotation within 24 hours.

Checklist for Fast 24-Hour Engineering CAD Design

  1. Warehouse CAD layout drawing showing structural building columns and door clearances
  2. Clear building height to the lowest overhead obstruction or sprinkler head
  3. Pallet / storage box dimensions (Width × Depth × Height) and maximum unit weights
  4. Forklift or picking vehicle specifications (Minimum turn radius and maximum reach height)
  5. Target operational environment (Ambient temperature, dry archive, or cold chain freezer)