[email protected] Serving India · Bangladesh · Pakistan · Sri Lanka · Nepal
English (South Asia)
Industrial drive-in racking system engineered by Guangzhou Heda Shelves Co., Ltd.
Engineering Authority · High-Density Storage

Drive-In Racking System: Ultimate Guide to High-Density Pallet Storage & Global Procurement

  • Up to 80% floor footprint utilization via eliminating working aisles
  • CE & ISO 9001:2015 certified structural engineering for cold stores and FMCG
  • Direct design, fabrication & load calculation by Guangzhou Heda Shelves Co., Ltd.
Certified RigorCE No. 2435-CPR-8605159 & ISO
30,000 m² FacilityAutomated continuous cold rolling
Export to 120+ CountriesDirect containerized sea freight
Free CAD & FEA DesignLoad capacity structural verification
Technical Architecture

What Makes Drive-In Racking the Benchmark for Maximum Volume Density?

When warehouse land costs surge and temperature-controlled cubic volume demands stringent space efficiency, global supply chain directors turn to drive-in racking systems. By removing intermediate handling aisles, drive-in racking yields unmatched volumetric consolidation.

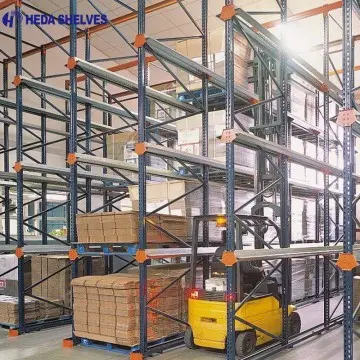
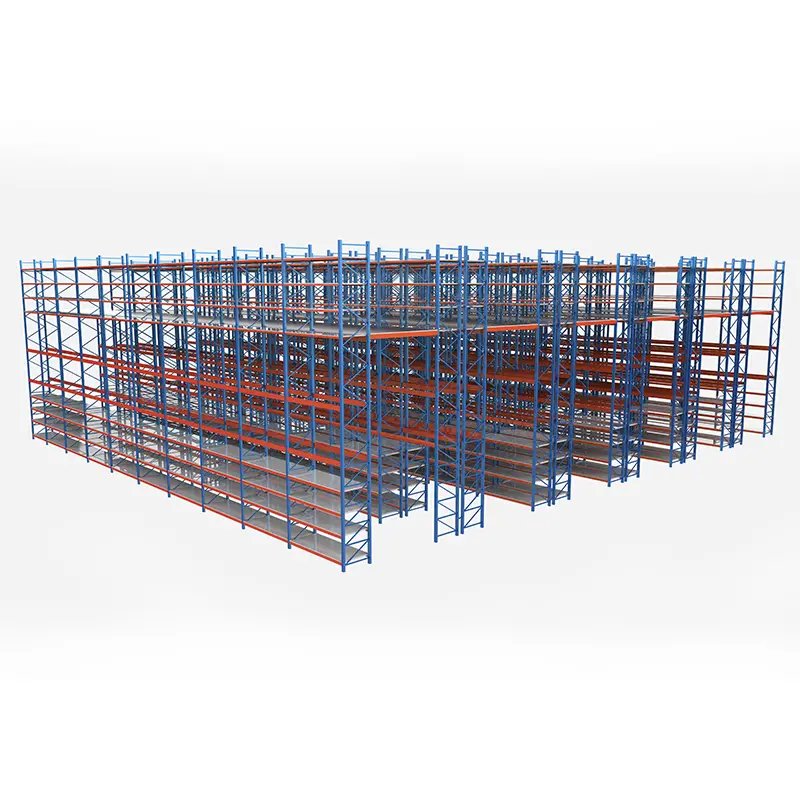
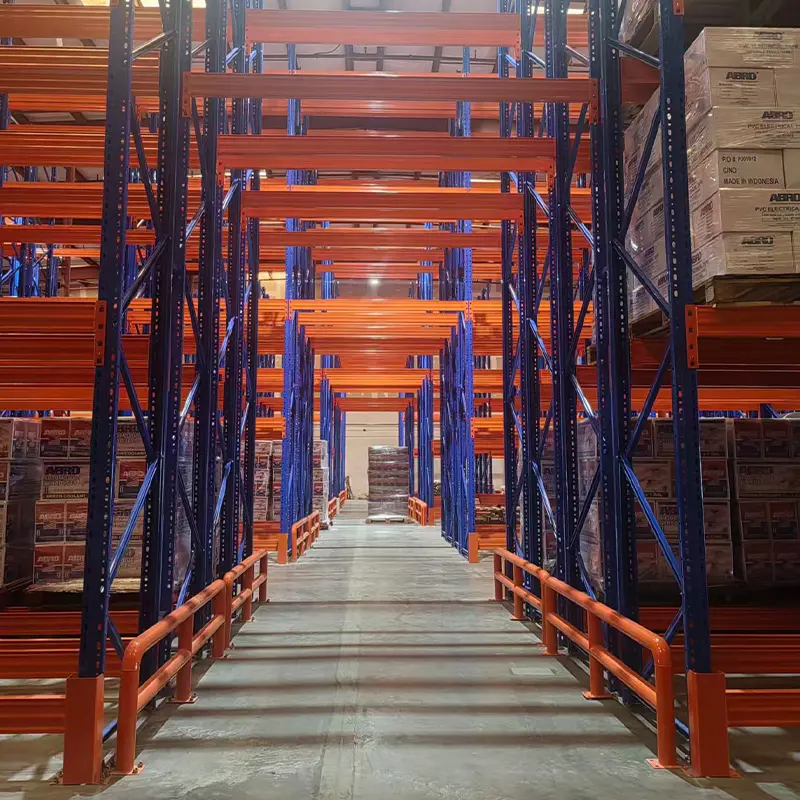
A Drive-In Racking System is a continuous block of storage lanes unhindered by conventional forklift operating aisles. Unlike selective pallet racking where load beams connect columns beneath every pallet face, drive-in systems support pallets on continuous heavy-gauge side cantilever rails. Forklift trucks physically enter the rack structure's internal bays to deposit or retrieve loads from floor to ceiling.

Operating primarily under the Last-In, First-Out (LIFO) inventory management protocol, drive-in racking converts up to 80% of open warehouse footprint into net storage capacity. For operations handling uniform stock with massive turnover per Stock Keeping Unit (SKU)—such as raw ingredient bulk stores, beverage distribution hubs, seasonal agricultural crops, and commercial cold storage—the system delivers the lowest capital equipment cost per cubic pallet footprint of any high-density solution.

  • Eliminate AislesRecover 35% to 50% wasted transit floor area
  • Thermal OptimizationReduce refrigerated refrigeration volume loss
  • Heavy Load ProfilesEngineered up to 1,500 kg per pallet position
  • Turnkey EngineeringCustom rail cantilever brackets and top portal ties
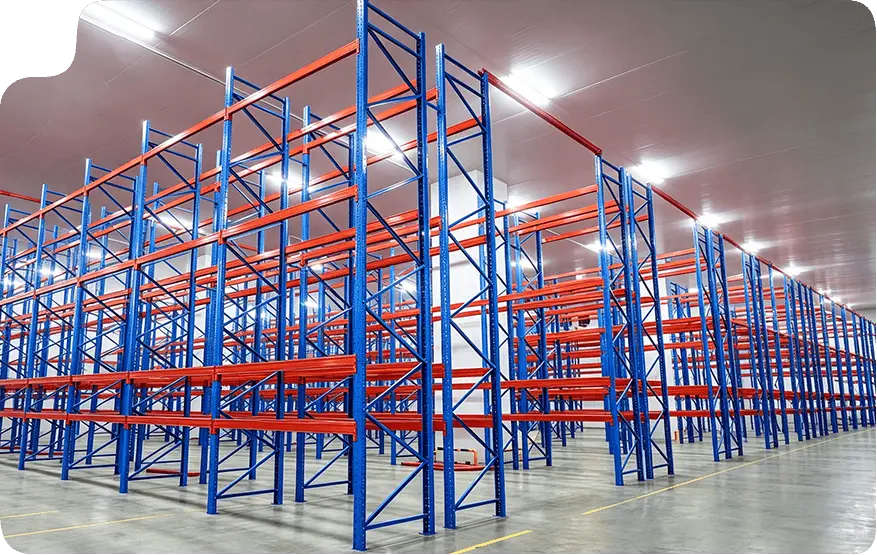
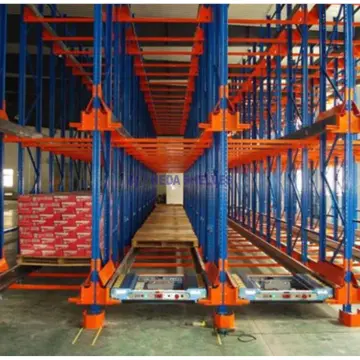
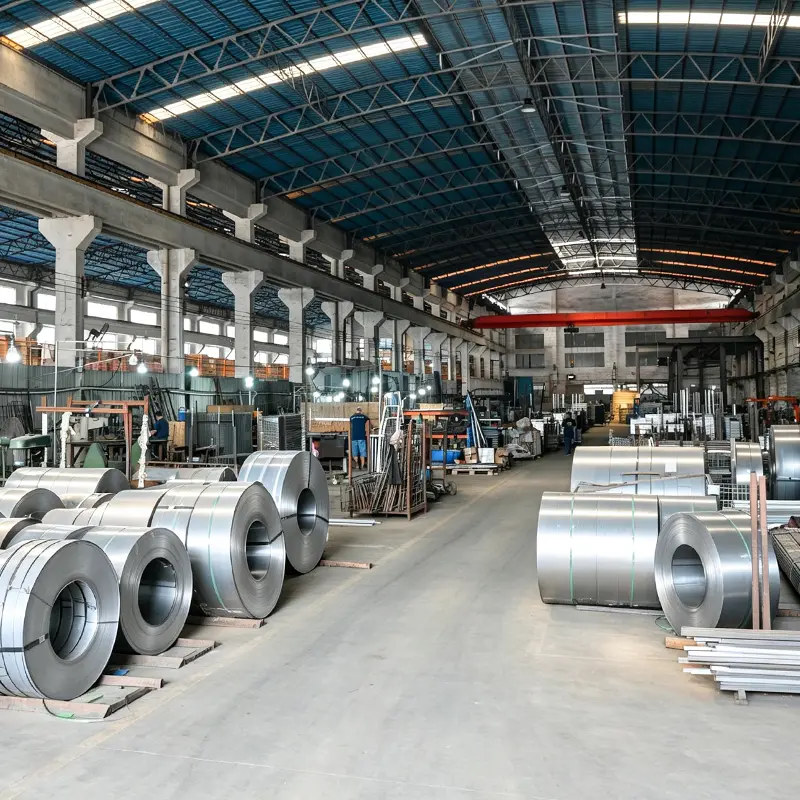
Drive in racking structural configuration HEDA 30,000 m² Racking Production Line
Engineered Configurations

Drive-In Racking Configurations Recommended for Industrial Facilities

Every facility encounters distinct floor slabs, seasonal turnover velocities, and material handling equipment. Guangzhou Heda Shelves Co., Ltd. engineers three targeted variants of high-density drive-in systems.

Single-Entry Classic Drive-In Pallet Racking

Single-Entry LIFO Drive-In

Backed against solid warehouse perimeter walls or boundary fences. Pallets enter and exit from the single front operating corridor. Delivers peak volumetric efficiency when managing deep lanes (6 to 12 pallets deep) of uniform SKUs.

LIFO RotationDeep Lane StorageWall Boundary
Drive-Through Double-Sided Pallet Racking System

Drive-Through FIFO Racking

Configured with open aisles at both ends of the storage lane block. Material enters via the loading face and exits from the opposing picking face, enabling pure First-In, First-Out throughput for perishable goods.

Strict FIFOPerishable HubsDual Corridors
Heavy Cold Storage Drive-In Pallet Racking

Sub-Zero Cold Chain Drive-In

Custom-engineered with low-temperature cold-formed structural steel and galvanized or blast-resistant coating. Integrated heavy floor guide tracks ensure fork masts avoid upright contact under frost conditions.

-30°C Cold RoomAnti-CorrosionImpact Guiding
Hazardous & Heavy Chemical Drive-In Pallet Storage

Heavy Bulk Chemical Drive-In

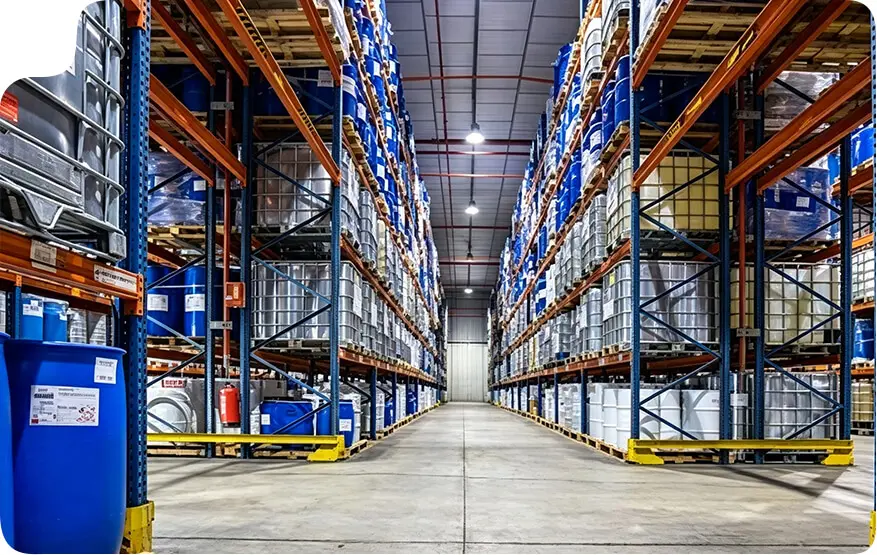
Engineered with reinforced column profiles up to 120mm cross-sections, specialized pallet support brackets, and overhead horizontal truss ties designed for dense liquids, chemical totes, and resin drums.

High Load LimitPortal Structural TiesChemical Ready
Structural Deep-Dive

The Engineering Anatomy of a Resilient Drive-In Racking System

Because forklifts drive inside the structural matrix where transverse cross-beams cannot be installed at lower pallet levels, drive-in systems demand advanced static and dynamic engineering to resist lateral sway and equipment impact.

Top & Back Portal Bracing

Without intermediate aisle beams, lateral stability is achieved through top cross-horizontal portal trusses and high-tensile diagonal rear bracing frames that anchor the system into a monolithic rigid block.

Continuous Heavy-Gauge Pallet Rails

One-piece cold-rolled steel rails with flared lead-in entry bevels support pallet runners smoothly. Stamped bracket arms welded or bolted to uprights ensure uniform distribution of concentrated point loads.

Floor-Anchored Forklift Guide Rails

Heavy structural angle or channel steel runs down the concrete floor inside each lane. These rails physically direct forklift wheels, preventing erratic tracking, mast swerve, and upright impact.

Reinforced Upright Bull-Nose Guards

Front-facing entrance uprights endure recurring forklift brush contact. Guangzhou Heda Shelves Co., Ltd. integrates 8mm thick curved steel bull-nose guards anchored directly to the concrete floor slab.

Engineering Selection

Drive-In Racking vs. Alternative High-Density Systems

Compare critical engineering metrics to determine whether a Drive-In Racking System fits your warehouse material flow better than shuttle, push-back, or selective setups.

System Architecture Pallet Density Index Inventory Turnover Forklift Enters Rack Capital Cost / Pallet Position Recommended Applications
Drive-In Racking (80%) LIFO Yes (Direct entry) Lowest Capital Outlay Cold storage, bulk food, beverage, seasonal crops
Radio Shuttle Racking (85%) FIFO or LIFO No (Shuttle carrier) Moderate to High (Automated) Massive throughput, automated distribution hubs
Push-Back Pallet Rack (70%) LIFO No (Gravity carts) Moderate 2–6 pallet lanes, medium batch SKUs
Pallet Flow Racking (75%) Strict FIFO No (Gravity rollers) High (Mechanical rollers) High turnover perishables, strict shelf-life control
Selective Pallet Racking (40%) FIFO / 100% Direct No (Aisle access) Low baseline Multi-SKU eCommerce, 3PL logistics facilities

*Density index represents practical warehouse cubic footprint utilization. Full structural simulations are engineered based on specific facility heights.

Manufacturing Authority

Why Global Importers Source From Guangzhou Heda Shelves Co., Ltd.

Send an Inquiry
20+ Years Racking Industry Expertise Guangzhou Heda Shelves Co., Ltd.
01

25+ Years Industrial Expertise

Established in 2001, we bring over two decades of structural engineering across global manufacturing, cold storage, and 3PL warehousing.

Free 3D and CAD Warehouse Layout Design
02

Free CAD & 3D Modeling

Our engineering office prepares full layout drawings, aisle clearances, and 3D renderings within 24 hours of receiving site schematics.

Safe durable quality racking components
03

Audited International Quality

Certified under CE No. 2435-CPR-8605159, ISO 9001:2015, and RoHS standards. Fully monitored quality control from coil slitting to shipment loading.

Fully Customized Warehouse Racking Solution
04

30,000 Ton Monthly Capacity

Our 30,000 m² Guangzhou production facility operates continuous roll-forming lines, automated punching, and powder-coating systems for fast lead times.

2001
Year Founded
300+
Skilled Engineers & Workers
30000T
Monthly Steel Output
30000m²
Modern Production Base
Factory Traceability

Strict 10-Stage Drive-In Racking Manufacturing Quality Control

From raw certified steel coils to sea-container bundle packing, every drive-in component is produced under strict ISO 9001:2015 traceability.

Traceable Precision

Integrated Production Line

Raw steel coils inspectionSTEP 01

Raw Material Verification

Certified mill steel coils inspected for chemical composition and yield strength.

Precision steel slitting and cuttingSTEP 02

High-Precision Slitting

Computerized longitudinal slitting to exact coil strip dimensions.

Automated column punching for drive-in uprightsSTEP 03

Automated Punching

High-speed CNC stamping creates exact 50mm or 75mm teardrop and diamond pitches.

Cold bending and section formingSTEP 04

Cold Profile Forming

Multi-roller continuous profiling builds rigidity into column flanges.

Pallet rail roll formingSTEP 05

Rail Roll Forming

Specialized tooling rolls one-piece drive-in pallet support rails.

Polishing and deburring steel edgesSTEP 06

Precision Deburring

Beveling and polishing eliminate sharp edges for safe handling.

Robot bracket weldingSTEP 07

Robotic Welding

Shielded automatic arc welding fuses bracket arms to structural brackets.

Pickling and phosphating tank lineSTEP 08

Pickling & Phosphating

Multi-bath chemical immersion removes oil and rust to bond powder coat.

Electrostatic powder coating applicationSTEP 09

Powder Coating

Thermoset epoxy polyester curing provides durable impact resistance.

Packaging and container shippingSTEP 10

Container Bundling

High-density strapping with edge protectors for damage-free ocean freight.

Search Intent & FAQ

Critical Questions Global Buyers Ask About Drive-In Racks

Answers to key technical, structural, and procurement questions raised by warehouse engineers, 3PL managers, and sourcing teams worldwide.

The primary distinction lies in operating aisles and stock rotation. A Drive-In Racking System features a single entrance and exit aisle for each storage lane, operating strictly under Last-In, First-Out (LIFO). It rests against building walls or back-to-back blocks for higher structural rigidity. Conversely, Drive-Through Racking provides open entry points at both the front and rear faces of the bay block, allowing material to be deposited at one end and retrieved from the other under First-In, First-Out (FIFO) turnover. Drive-through systems require additional overhead portal bracing and tie structures to maintain structural stability without back cross-braces.

Guangzhou Heda Shelves Co., Ltd. uses a 3-layer protection protocol: First, continuous heavy-duty structural steel floor guide channels run the entire depth of the bay, physically guiding forklift steer tires inside the safe envelope. Second, entrance uprights feature heavy 8mm wrap-around steel bull-nose guards anchored directly into the slab. Third, high-visibility hazard warning yellow and signal orange electrostatic finishes provide clear visual targeting for operators.

Drive-in systems require high-integrity pallets with solid timber runners or heavy-gauge plastic frames. Because pallets rest on side cantilever rails rather than full transverse beams, pallets must not have cracked skids, missing bottom boards, or weakened center blocks. Common configurations fit ISO 1200x1000mm, Euro 1200x800mm, or custom GMA 48x40-inch pallets. Pallet side overhang beyond the rail bracket should not exceed 25mm to avoid horizontal interference during lift cycles, while maintaining at least 50mm to 75mm of contact seating on each rail.

For seismic locations, our structural engineers evaluate ground peak acceleration according to local building codes. We engineer heavier base plate dimensions, dual heavy wedge anchors per upright column, and multidirectional overhead sway trusses. In sub-zero cold storage facilities down to -30°C, we specify ductile certified structural steel grades that resist low-temperature embrittlement, paired with hot-dip galvanizing or cold-resistant powder finishes that stop moisture cracking and thermal delamination.

To produce an optimized CAD layout and load matrix, share: 1) Architectural CAD or PDF drawings showing wall clearances, column grid locations, and overhead obstructions (sprinklers, HVAC ducts, lighting); 2) Clear warehouse ceiling height and concrete slab thickness/grade; 3) Exact pallet specifications including length, width, overall height including cargo, and maximum gross loaded weight; 4) Forklift specifications including overall width, chassis wheel width, mast closed collapsed height, and maximum lift elevation; 5) Operational temperature profiles and project port of discharge.

Direct Factory Engineering

Maximize Your Warehouse Storage Density with Drive-In Racking

Partner directly with Guangzhou Heda Shelves Co., Ltd. Send your warehouse floor drawing and pallet specifications to receive a free CAD layout, 3D structural model, and export proposal within 24 hours.

Send an Inquiry

Layout Checklist for Fast Turnaround

  1. Facility layout drawing (CAD / DWG or PDF) with building column grids
  2. Clear warehouse height to lowest sprinkler, lighting, or roof beam obstruction
  3. Pallet dimension, cargo overhang limits, and gross weight per unit load
  4. Forklift truck mast closed height, maximum reach, and outer chassis width
  5. Target destination city and preferred seaport of discharge for freight calculation