Engineered Extra Heavy Duty Pallet Racks & Systems
Custom-calibrated load capabilities spanning 1,000 kg to over 5,000 kg per tier. Manufactured in accordance with rigorous CE, ISO 9001:2015, and FEM/RMI international storage rack safety design standards.
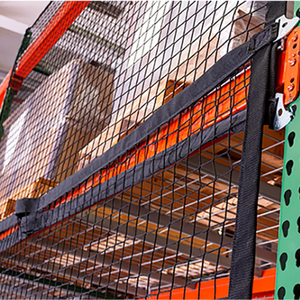
Heavy-duty containment mesh engineered to avert rear aisle fall hazard in high-bay double-entry racks. High-tenacity polyester woven netting.
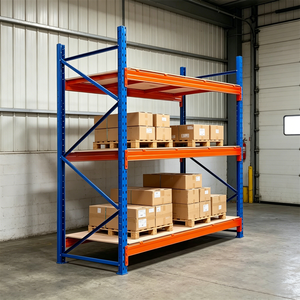
Continuous roll-formed box beams paired with 75mm/50mm adjustment pitch uprights. 100% direct access layout suited for fast-moving multi-SKU hubs.
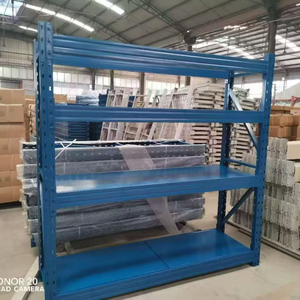
Heavy duty hybrid workshop shelving accommodating heavy tool fixtures, CNC dyes, and raw casting blocks. Modular deck inserts with steel panels.
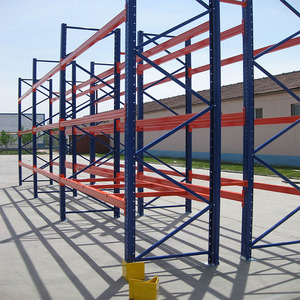
Grade 304/316 stainless configuration tailored for sterile pharmaceutical facilities, sub-zero cold chain blast freezers, and maritime chemical stores.
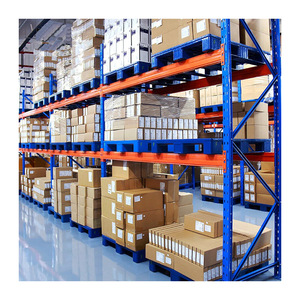
Reinforced column web thickness up to 2.5mm with multi-claw connector pins. Engineered specifically for automotive castings, stamping dies, and machinery.
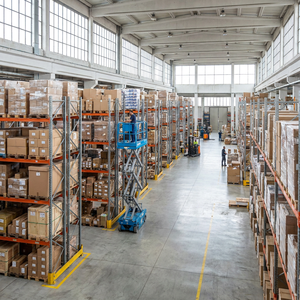
Turnkey enterprise high-bay structural frameworks. Fully integrated with automated reach trucks, VNA systems, and seismic tie-back dynamic bracings.
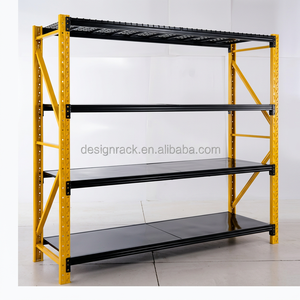
Heavy duty mobile-base mounted wide-span storage racks. Designed for dense hardware, building profiles, and multi-tier picking aisles with effortless track motion.
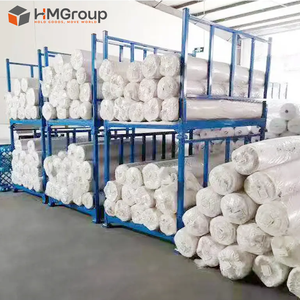
Engineered saddle arms and nested post-pallet frames tailored for heavy textile rolls, coiled copper wire, and cylindrical industrial cylinders.
Engineering Benchmark: Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates an advanced 30,000 square meter standardized manufacturing facility equipped with automated roll-forming lines, automated continuous punching machines, robotic MIG welding units, and an integrated electrostatic powder coating plant. Producing over 30,000 tons of structural steel storage systems each month, we manage total fabrication integrity entirely in-house.
Certified Metallurgy
Every structural profile originates from certified prime Baosteel and Shougang Q235B/Q355B coils with strict mill test certificates, guaranteeing tensile stability under dynamic forklift loading.
Pretreatment Excellence
Components undergo an automated 10-stage chemical pickling and phosphating process, shielding inner and outer surfaces against tropical humidity, maritime rust, and chemical vapors.
Free CAD & Structural Feasibility
Our 30+ project engineers provide complimentary CAD layout drafting, 3D parametric warehouse simulations, and comprehensive static/dynamic finite element load verifications within 24 hours.
Global Direct Sea Logistics
High-cube container-maximized bundle nesting eliminates wasted shipping cubic space, shipping factory-direct to Nhava Sheva, Mundra, Chattogram, Colombo, Rotterdam, Los Angeles, and Jebel Ali.
Extra Heavy Duty Pallet Rack Structural Engineering Matrix
When specifying extra heavy duty racking systems (exceeding 2,500 kg per beam level), traditional safety assumptions do not suffice. Structural deflection criteria (FEM 10.2.02 standard limiting deflection to L/200) and beam connector notch tear-out values must be calculated based on concrete slab compressive thresholds.
| Racking Architecture | Typical Beam Section (mm) | Max Load / Bay (kg) | Handling Equipment Required | Floor Slab Minimum (Concrete) | Ideal Industry Utilization |
|---|---|---|---|---|---|
| Extra Heavy Selective | 120×50×1.5 to 160×50×2.0 Box | 16,000 – 24,000 | Standard Counterbalance / Reach | 200mm C25/30 Reinforced | Automotive, Paper Mills, FMCG High-Bay |
| Drive-In / Drive-Thru | Custom Cantilever Rails 2.5mm | 14,000 – 20,000 | Narrow Counterbalance Truck | 220mm C30 Double Rebar | Cold Storage (-25°C), Bulk Raw Ingredients |
| Radio Shuttle Automation | Galvanized Omega Rail Profiles | 25,000 – 35,000 | Lithium Battery Radio Shuttle + Forklift | 200mm Flatness Superflat Slab | Food Production Buffers, Meat Cold Chain |
| Heavy Duty Cantilever | 250UB to 400UB Welded I-Beams | 15,000 – 30,000 | Side Loader / Four-Directional Truck | 250mm C35 Isolated Footings | Steel Pipe Bundles, Heavy Timber, Billets |
| Rack-Supported Mezzanine | 100×70×2.5 Uprights + C-Purlins | 800 – 1,500 kg/m² | Pallet Jacks, Goods Lifts, Manual Carts | 200mm C25 Slab | E-commerce Sortation, Spare Parts Warehouses |
Future Procurement & Technological Trends in Heavy Storage (2026–2030)
Supply chain infrastructure is experiencing unprecedented capital transformation. Modern procurement leaders must align warehouse racking investments with structural longevity, decarbonization compliance, and automated warehouse convergence.
IoT Seismic & Load Deflection Sensors
Future extra heavy-duty installations increasingly specify strain-gauge upright monitoring modules. Real-time telemetry detects forklift impact micro-fractures, beam overloading, and foundation settling before catastrophic rack failure occurs.
Cold-Formed High-Tensile Micro-Alloy Steel
Procurement is pivoting away from heavy standard mild steels toward thinner yet stronger micro-alloy grades (such as Q355MC and DOMEX). This cuts total structural weight by 18%, reducing maritime container freight charges while elevating ultimate yield point strength.
Hybrid AMR & Shuttle-Ready Architecture
Fixed selective layouts are being superseded by flexible shuttle-integrated racks engineered to interface seamlessly with Autonomous Mobile Robots (AMRs) and automated automated storage and retrieval system (ASRS) crane units, eliminating human transit in high-density rack lanes.
Frequently Asked Questions by Industrial Sourcing Directors
Direct technical answers addressing slab capacity calculations, anti-corrosion finishes, international code compliance, and global logistical clearance.
How do we calculate if our concrete slab can support extra heavy racking?
Extra heavy racks transfer massive point loads through baseplates to the floor (often exceeding 60 to 100 kN per column foot). Sizing requires calculating baseplate dimension distribution (e.g., 200×200×10mm plates with twin high-tensile wedge anchors) against concrete compressive strength (typically C25/30 or 3,000 PSI) and slab thickness. We provide slab loading reports alongside preliminary CAD submittals.
What is the difference between electrostatic powder coating vs. hot-dip galvanization?
Thermoset polyester powder coating (60–80 microns) provides superb abrasion resistance, impact buffering, and custom color coding for ambient dry warehouses. Hot-dip galvanization (ISO 1461, 70–100 microns metallurgical zinc alloy) is imperative for outdoor lumber/steel storage yards, highly corrosive fertilizer/chemical sheds, and blast chillers with extreme humidity cycles.
Which international manufacturing & design standards do HEDA racks comply with?
Our heavy-duty racking engineering complies with European standard EN 15512 (Steel static storage systems – Racking design), EN 15620 (Tolerances, deformations and clearances), American RMI MH16.1 specifications, Australian Standard AS 4084-2012, and verified CE certificate (No. 2435-CPR-8605159) alongside ISO 9001:2015 quality management.
How does HEDA prevent upright damage from heavy forklift impacts?
In extra heavy storage, forklift impact is the primary cause of upright bucking. We engineer three lines of defense: 1) Formed wraparound steel column protectors anchored directly to the slab; 2) Heavy-gauge tubular end-of-row crash barriers; and 3) Custom reinforcing structural channel inserts welded inside the lower 1,000mm of the upright frame.
Can your factory support OEM customized upright hole punching and beam profiles?
Yes. With extensive tool design and mold fabrication capabilities, we manufacture 50mm, 75mm, 76.2mm (3 inches), and tear-drop connector configurations. Private branding, customized beam stamping, bespoke paint matching (RAL standard), and bespoke deck accessories can be configured for distributors and regional integrators.
What technical documentation is provided with international shipments?
Every export container leaves our facility with numbered packaging checklists, mill test reports verifying raw steel chemical compositions, weld quality certificates, CAD assembly elevations, load capacity bay plates, and step-by-step installation manuals accompanied by high-definition video walkthroughs.
Request an Engineered Layout & Quotation for Your Warehouse
Send your building dimensions, clear height, pallet loading specifications, and forklift parameters. Our technical engineering division will generate a detailed 2D CAD blueprint, 3D visualization, and FOB/CIF commercial proposal within 24 hours.