Featured Warehouse Storage & Heavy-Duty Racking Solutions
Engineered from certified Q235B/Q355B structural steel, our precision roll-formed storage configurations optimize warehouse footprint, improve picking throughput, and guarantee structural reliability under rigorous loading criteria.
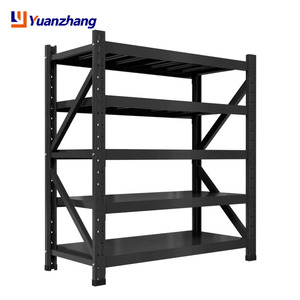
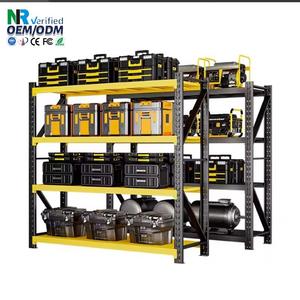
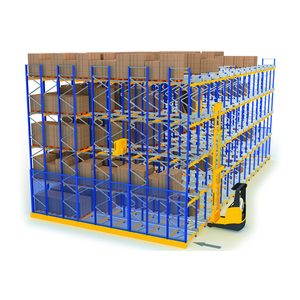
The Definitive Engineering Perspective: Procurement & Manufacturing Excellence
As logistics operations evolve globally, procurement executives face intense challenges: skyrocketing industrial land lease costs, stringent workplace safety regulations, and the operational demands of high-velocity omni-channel distribution. Selecting a qualified China warehouse storage shelving systems supplier requires looking beyond raw steel weight. Engineering teams must evaluate load deflection tolerances under dynamic stress, raw material metallography, anti-seismic anchoring designs, and automated surface treatment longevity.
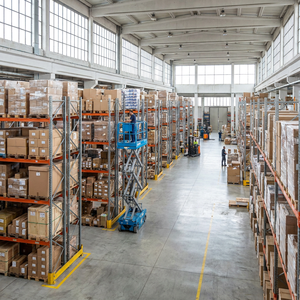
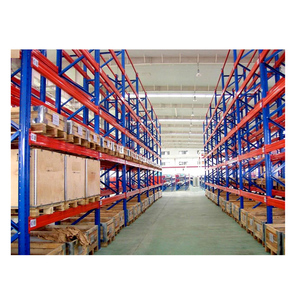
Modern warehouse logistics can no longer rely on single-tier static shelving. Supply chain directors must maximize vertical clear height through selective pallet racking, multi-tier rack-supported mezzanines, narrow-aisle (VNA) systems, and semi-automated high-density radio shuttle configurations. Each system requires precise calculation of live and dead loads, pallet run-out clearance, and forklift corridor aerodynamics. Partnering directly with an established original equipment manufacturer (OEM) provides direct structural engineering support, full traceability of steel coils, and customized production tailored to international norms such as EN 15512, RMI, and AS 4084.
Future Warehouse Storage Shelving Procurement Trends
How corporate supply chains are shifting capital expenditures toward resilient, modular, and container-optimized logistics infrastructure.
High-Density Volumetric Scaling
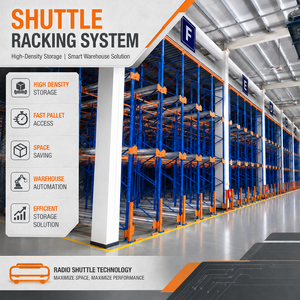
Industrial land scarcity has caused a structural shift from wide-aisle storage to high-bay vertical configurations. Procurement managers increasingly specify Drive-In, Push-Back, and 4-Way Radio Shuttle racking systems to achieve up to 80% spatial cube utilization compared to 40% in conventional setups.
Total Landed Cost & Packing Engineering
B2B buyers evaluate suppliers based on container packaging engineering. Precision nested roll-formed profiles maximize 40HQ ocean container volume, protect pre-treated powder coatings from maritime salt spray, and dramatically reduce freight costs per pallet location.
Decoupled Automation Integration
Rather than committing immediately to rigid, multi-million-dollar automated cranes, warehouses now choose semi-automated radio shuttle pallet racking. This modular step-up path preserves capital, supports FIFO and LIFO dispatching, and allows easy scale-up as volumes grow.
Engineering & Manufacturing Development Trends
Breakthroughs in structural steel metallurgy, surface anti-corrosion, and intelligent robotics are reshaping storage system durability.
High-Yield Ultra-Thin Profiles
Through advanced cold-roll continuous forming, column uprights achieve higher yield strengths (up to 355-420 MPa) while reducing gross steel weight. Multi-bend profile geometry adds torsional stiffness under severe axial dynamic loads.
Sub-Zero & Coastal Pretreatment
Advanced 10-stage automated surface preparation—including degreasing, ultrasonic acid pickling, and micro-crystalline phosphating—ensures 80-120 micron thermosetting epoxy-polyester coatings bond firmly to resist delamination down to -30°C in cold-chain logistics.
Digital Twin & Smart Sensors
Heavy-duty storage systems are integrating IoT strain gauges and deflection sensors within load beams. Real-time seismic vibration monitoring and structural balance tracking warn facility operators of accidental forklift impact damage before structural failures can occur.
Why Industry Leaders Partner with HEDA Shelves
Guangzhou Heda Shelves Co., Ltd. delivers direct factory capabilities, strict quality controls, and custom engineering support to logistics projects worldwide.
25+ Years Industrial Expertise
Founded in 2001, we deliver mature design, roll-forming, and system fabrication across FMCG, pharmaceutical, automotive, and cold-storage distribution sectors.
30,000 m² Production Base
Equipped with automated continuous roll-forming lines, laser profiling cutters, robotic welders, and Swiss powder coating lines producing 30,000 metric tons monthly.
Free 3D & CAD Design
Senior structural engineers deliver warehouse layouts, pallet positioning plans, and dynamic structural calculations within 24 hours of your initial request.
Verified Global Compliance
Production facilities are fully certified to CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Quality Management System No. 18624Q00169R0M, and RoHS standards.
Frequently Asked Questions (FAQ)
Clear, technical answers to common questions about cross-border shipping, steel performance, installation, and custom system engineering.
All HEDA pallet racking systems are engineered according to FEM 10.2.02 and EN 15512 standards. Beam deflection under full safe working load (SWL) is held to less than 1/200th of the clear span length (L/200), ensuring safety and protecting against permanent yield deformation during forklift cycles.
To produce an engineering CAD layout, please share: your warehouse architectural drawing (showing columns, fire escapes, and clear ceiling heights), pallet dimensions (Width x Depth x Height including load), maximum pallet weight, forklift model and mast lift height, and your warehouse operating temperature.
Components undergo an automated chemical wash, acid rust removal, and phosphating pretreatment followed by thermosetting electrostatic polyester-epoxy powder coating cured at 180°C–200°C. For sub-zero freezers, wet processing plants, or coastal operations, we offer hot-dip galvanizing per ISO 1461.
Every export container includes tagged components, bill-of-materials manifests, 3D exploded assembly diagrams, and step-by-step video walk-throughs. For large automated rack projects or multi-tier mezzanines, we dispatch experienced installation engineers on-site to direct local labor teams.
Transform Your Warehouse Storage Efficiency
Contact our structural engineering team today to receive a free, comprehensive CAD warehouse layout, structural calculation report, and factory-direct pricing for your project.
Inquire Now