High Bay Heavy Duty Pallet Storage Systems
Engineered cold-formed steel high bay racks certified to EN 15512 and RMI specifications. These 8 systems represent industry benchmarks for vertical storage density up to 40 meters.
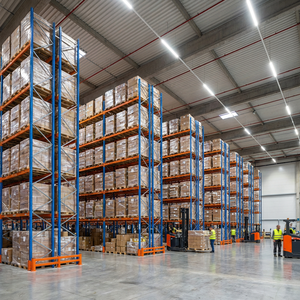
Heavy Duty Selective Pallet Racking System
- 100% Pallet Accessibility
- Up to 5,000 kg Bay Capacity
- Standard & Narrow Aisle (VNA)
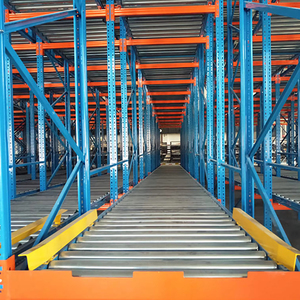
Heavy Duty Live Pallet Gravity Flow Rack
- Strict FIFO Expiry Control
- Speed Controllers & End Separators
- 1,000kg/layer Heavy Live Lanes
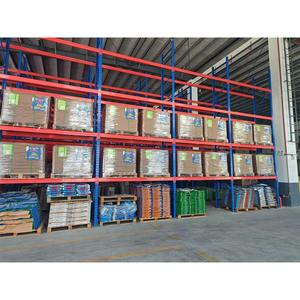
High Bay Heavy Duty Steel Pallet Racking
- Vertical Clears Over 15 Meters
- Q235B / Q355B Structural Steel
- Reinforced Base Plates & Portals
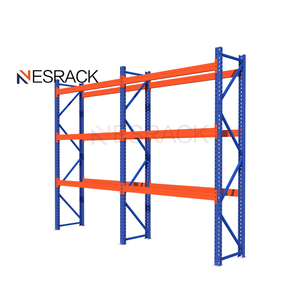
Multi-Level High Density Pallet Racking
- Custom Hole Pitch (50mm/75mm)
- Multi-Tier Order Picking Integration
- High-Tonnage Seismic Uprights
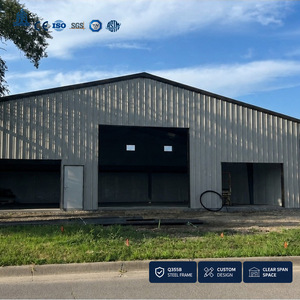
Prefabricated High Bay Storage System
- Distribution Facility Space Planning
- Turnkey Prefabricated Structural Frame
- Optimized Column Bay Footprint
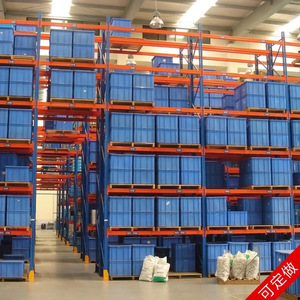
Cold Rolled Multi-Layer Pallet Racking
- Epoxy Powder Coating (Pickled/Phosphated)
- Anti-Monsoon & Salt-Spray Resistance
- Continuous Cold Roll-Formed Profiles
Industrial Multi-Tier High Bay Shelves
- Integrated Upright Splice Sockets
- Heavy Wire Mesh & Pallet Support Bars
- Versatile SKU Profile Support
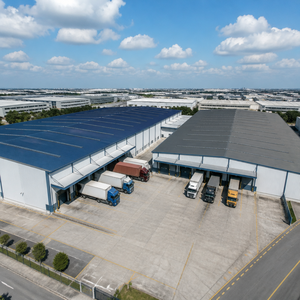
Large Scale High Bay Steel Frame Design
- Rack-Clad Building Structural Design
- AS/RS Crane Rail & Mast Tie-Ins
- Wind, Snow & Seismic Load Engineered
The Engineering Evolution of High Bay Pallet Racking in Modern Intralogistics
Top 10 High Bay Pallet Racking Manufacturers & Suppliers
A rigorous industrial analysis evaluating engineering capability, manufacturing footprint, seismic design compliance, and vertical high-density racking execution across the world's premier suppliers.
Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves)
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has developed into a premier global manufacturing powerhouse for heavy duty high bay pallet racking, industrial automated shuttle racks, and rack-supported structures. With a modern 30,000 m² production facility and an output exceeding 30,000 metric tons per month, HEDA maintains full vertical control across cutting, CNC punching, continuous cold roll-forming, automated robotic welding, and a state-of-the-art 10-stage pickling and phosphating pre-treatment powder coating line.
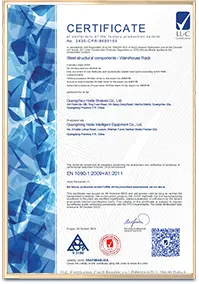
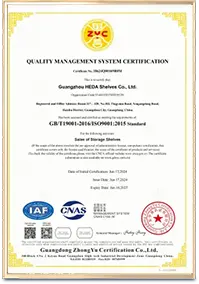
HEDA's core competitive advantage lies in custom structural engineering for international buyers across Europe, South America, and South Asia. Specializing in high-humidity monsoon resilience, seismic floor-slab engineering adaptations, and containerized transport volume optimization, HEDA provides complimentary structural CAD layouts and 3D FEA simulations within 24 hours. The company holds valid CE Certification (No. 2435-CPR-8605159) and ISO 9001:2015 registration.
SSI Schaefer Group
SSI Schaefer is a titan in automated intralogistics and high bay rack-clad warehouse construction. Renowned for multi-tier channel storage, complex crane-based high bay distribution facilities, and fully integrated automated software-to-steel solutions. Schaefer excels in massive distribution mega-hubs reaching up to 45 meters in height.
Daifuku Co., Ltd.
As one of the world's largest automated material handling equipment providers, Daifuku provides turnkey automated high bay racking frameworks designed specifically for ultra-precise stacker crane travel and semiconductor / cold chain environments. Their structural frameworks emphasize extreme seismic shock dissipation developed for earthquake-prone geographies.
Mecalux S.A.
Mecalux is a leading European and North American supplier of selective, drive-in, high bay, and automated pallet storage systems. Their proprietary Easy WMS software seamlessly complements their steel high bay profiles. Mecalux has constructed hundreds of self-supporting rack-clad buildings worldwide, utilizing the racking uprights to carry roof trusses and side wall cladding.
Dematic (KION Group)
Part of the international KION Group, Dematic supplies comprehensive automated high bay racking modules paired with high-velocity automated storage systems. Dematic's engineering emphasizes continuous automated carton and pallet handling across high-throughput omni-channel retail distribution and grocery fulfillment hubs.
Jungheinrich AG
Jungheinrich bridges the gap between forklift material handling equipment and high bay static steel structures. Offering unified solutions that include narrow-aisle VNA trucks, optical wire-guided turret trucks, and high bay pallet racking systems up to 18 meters, Jungheinrich guarantees precise mechanical tolerance coordination between trucks and racks.
Stow Group (stow Robotics)
Stow Group is one of the premier pallet racking manufacturers in Europe, operating numerous advanced production plants. With their "stow Robotics" division, they have established benchmarks in high bay pallet shuttle systems (stow Atlas) and automated high-density radio shuttle matrix configurations engineered for extreme cold and high-tonnage storage.
Dexion (Gonvarri Material Handling)
With historical roots dating back to the invention of slotted angle steel, Dexion is an iconic brand under the Gonvarri Material Handling umbrella. Dexion provides high-precision high bay pallet racks, multi-tier platforms, and mobile high bay systems (MOVO) engineered to reduce footprint while maintaining high pallet selectivity.
BITO-Lagertechnik Bittmann GmbH
BITO is celebrated for precision German engineering in heavy pallet racking and small-parts multi-tier shelving systems. Their high bay installations focus on modular boltless beam connections, proprietary profile cold roll-forming that reduces upright twisting under eccentric loads, and robust end-of-aisle safety hardware.
Nedcon B.V. (MiTek)
Operating as part of MiTek (a Berkshire Hathaway company), Nedcon is an engineering-first manufacturer focusing on custom structural frameworks for automated system integrators. They excel at producing bespoke high bay racking that accommodates automated stacker cranes, micro-load shuttles, and specialized mezzanines with non-standard deflection requirements.
High Bay System Technical Comparison Matrix
A side-by-side engineering breakdown comparing structural clear heights, maximum bay loads, deflection tolerances, seismic compliance, and capital investment intensity across high bay configurations.
| System Architecture | Operating Height | Max Bay Capacity | Deflection Limit | Aisle Width Req. | Handling Equipment | Relative Cost Factor |
|---|---|---|---|---|---|---|
| Standard Wide Aisle High Bay | Up to 12.0 Meters | 12,000 – 16,000 kg | L / 200 | 3.2m – 3.8m | Standard Reach Truck / Counterbalance | Baseline (1.0x) |
| Very Narrow Aisle (VNA) High Bay | 12.0m – 18.0 Meters | 16,000 – 24,000 kg | L / 300 to L / 400 | 1.6m – 1.9m | Man-Up / Man-Down Turret Truck (Wire Guided) | Moderate (1.4x – 1.8x) |
| Radio Shuttle High Bay Channel | Up to 22.0 Meters | 20,000 – 28,000 kg | L / 350 | Variable / Lane Access | Semi-Automated Battery Shuttle + Forklift | High (2.2x – 2.8x) |
| Automated Stacker Crane (ASRS) | 18.0m – 35.0 Meters | 24,000 – 40,000 kg | L / 500 | 1.4m – 1.6m | Rail-Guided Stacker Crane (SRM) | Intensive (3.5x – 5.0x) |
| Rack-Clad Self-Supporting Building | 25.0m – 45.0+ Meters | Custom Engineered | L / 600 (Dynamic) | 1.4m – 1.5m | High-Speed Automated Crane + Monorail | High Capital (Comprehensive) |
Future Procurement Trends in High Bay Storage Systems (2025–2030)
How supply chain executives, global procurement directors, and EPC logistics engineers are navigating carbon-neutral steel, raw material price hedging, and modular scalability.
Decoupling Land Value via Cubic Volume Optimization
With prime logistics land values in major port cities and distribution corridors climbing annually, procurement executives are standardizing on 15m+ vertical profiles over expansive single-story horizontal footprints. The objective is to maximize cubic meter storage efficiency, slashing warehouse per-pallet square footage overhead by up to 55%.
Total Cost of Ownership (TCO) Shift to Factory-Direct Sourcing
Procurement teams are bypassing regional distributors and middlemen in favor of certified Tier-1 factory-direct manufacturers like HEDA Shelves. Direct supplier relationships eliminate 20%–35% distributor markups, enable custom profile tooling, ensure direct mill test certificates (MTC), and provide dedicated project engineering support from design to installation.
Steel Price Hedging & Contractual Escalation Clauses
Due to steel coil volatility, large-scale high bay procurement contracts increasingly employ dynamic indexation models tied to Shanghai Steelhome or London Metal Exchange (LME) raw coil spot benchmarks. Phased batch manufacturing schedules allow procurement officers to lock in raw steel pricing in rolling tranches.
Stringent Life-Cycle Carbon & Eco-Pretreatment Standards
Multinational sustainability mandates and ESG scoring require lower embodied carbon in cold-formed structural members. Sourcing criteria now heavily penalize volatile solvent paints, favoring automated closed-loop powder coating with non-toxic chemical pickling and phosphating pre-treatments that deliver zero volatile organic compound (VOC) emissions.
Technological Innovations Reshaping High Bay Pallet Racking
From embedded structural telemetry and IoT load-cell sensors to autonomous forklift LiDAR navigation, high bay racking has become a digital, sensor-augmented asset.
IoT Upright Strain & Impact Telemetry
Piezoelectric impact sensors and wireless strain gauges embedded directly into vulnerable upright base profiles monitor accidental forklift collisions and real-time live structural loading. These telemetry nodes stream telemetry to warehouse facility management software, alerting engineers to localized structural yields before catastrophic collapse occurs.
Automated Pallet Shuttle Matrix Fleets
The transition from legacy drive-in racking to automated multi-directional 2D and 4D radio shuttles has revolutionized deep-lane high bay storage. Shuttles traverse channels autonomously at speeds exceeding 1.5 m/s, using integrated optical barcoding to position pallets without human forklift ingress, virtually eliminating frame impact damages.
BIM (Building Information Modeling) Digital Twins
High bay installations are now engineered as complete structural BIM objects. Incorporating structural thermal expansion coefficients, anchor pullout vectors, fire protection ESFR sprinkler feed clearance, and lighting duct geometries, the BIM digital twin guarantees millimeter-accurate cross-trade collision avoidance before steel erection begins.
Why Logistics Leaders Choose Guangzhou Heda Shelves
Combining 25+ years of structural fabrication heritage with comprehensive automated roll-forming lines, HEDA Shelves provides dependable factory-direct high bay solutions worldwide.
Turnkey Industrial Racking Engineering from China's Foremost Manufacturing Hub
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a sprawling 30,000 square meter modern manufacturing complex in Guangzhou, China. Staffed by over 300 experienced engineers, structural technicians, and skilled fabricators, HEDA maintains a robust 30,000-ton monthly production capacity, reliably fulfilling multinational supply chain and high bay infrastructure projects.
Every upright profile, step beam, diagonal bracing member, and connector claw undergoes rigorous internal quality management adhering strictly to ISO 9001:2015 and European CE structural certification standards (No. 2435-CPR-8605159). HEDA specializes in container-nesting optimization, packaging steel profiles to maximize 40HQ container cube utilization and lower CIF landed freight costs to major international ports across Europe, South Asia, and the Americas.
Auditable Quality & Compliance Credentials
In-House 10-Stage Heavy Duty Manufacturing Workflow
End-to-end quality assurance from prime steel coil slitting to corrosion-resistant electrostatic baking.
 01
Prime Raw Steel
Certified Q235B / Q355B coils tested for yield strength.
 02
Precision Slitting
High-speed slitting to exact dimensional widths.
 03
CNC Punching
Automated multi-head 50/75mm hole pitch punching.
 04
Cold Bending
Multi-angle bending to maximize sectional inertia.
 05
Continuous Forming
Multi-station roll-forming for seamless uprights.
 06
De-burring & Polish
Edge smoothing to eliminate burrs and sharp stress points.
 07
Robotic Welding
Automated beam connector welding under argon shielding.
 08
Pickling & Phosphating
Multi-tank chemical treatment eliminating oxide scale.
 09
Powder Coating
High-voltage electrostatic polymer epoxy powder curing.
 10
QC & Bundling
100% inspection, numbered tagging, and export packing.
High Bay Pallet Racking Procurement FAQ
In-depth structural engineering answers to the primary technical and commercial queries raised by warehouse developers, procurement managers, and operations consultants.
For high bay installations reaching 12 to 18 meters, concrete floor slabs must possess a minimum compressive strength of 25 to 30 MPa (C25/30 to C30/37). Slab thickness generally ranges between 200mm and 250mm with double-layer steel rebar reinforcement. More critically, floor flatness must conform to DIN 18202 Table 3 Line 3 or 4, or VDMA guidance for VNA operations to prevent reach truck mast sway.
HEDA utilizes a multi-stage pre-treatment wash including chemical acid pickling to strip mill-scale rust and hot zinc-phosphate immersion to create a microscopic crystal barrier on cold-rolled steel. This is followed by automated electrostatic deposition of outdoor-grade thermo-setting epoxy polyester powder baked at 180°C–200°C. For coastal zones or cold stores, hot-dip galvanized uprights (EN ISO 1461) are specified.
A freestanding high bay rack sits independently inside an existing steel portal warehouse shed, supporting only pallet dead-weights and dynamic live loads. A Rack-Clad (self-supporting) building uses the pallet racking upright columns as the primary vertical load-bearing structure for the facility itself, supporting roof trusses, insulated sandwich wall cladding, and resisting dynamic regional wind and seismic shear forces.
Standard roll-forming lines produce continuous upright profiles up to 12 or 15 meters. When high bay installations extend beyond this length, precision heavy-gauge internal steel sleeve splices are utilized. These precision-punched inner sleeves fit securely within the omega-profile upright cavity and are bolted with Grade 8.8 structural bolts, ensuring full moment continuity and transfer of axial and buckling loads.
To generate a complete structural CAD drawing and quotation, please provide: (1) Warehouse building DWG or PDF layout including clear building height and internal column grid spacing; (2) Pallet dimensions (Length x Width x Height including cargo overhang); (3) Maximum load weight per pallet; (4) Total target pallet count or SKU velocity; (5) Forklift model, mast collapsed height, and maximum fork elevation.
HEDA's high bay racks are calculated according to EN 15512:2020 (European Standard for Steel Static Storage Systems) and RMI ANSI MH16.1 (North American Standard for Industrial Steel Storage Racks). Seismic performance is verified per Eurocode 8 (EN 1998) or ASCE 7 seismic hazard maps, accounting for soil classification, spectral acceleration response, and structural ductility factors.
Request Your High Bay Racking Engineering Consultation
Connect directly with Guangzhou Heda Shelves' senior structural design engineers. We prepare free 2D architectural CAD layouts, 3D structural visual simulations, and precise container-optimized price quotations tailored to your operational facility within 24 hours.