Engineered Warehouse Storage Racking Systems
Precision-manufactured with structural steel certified to ISO 9001:2015 and CE standards. Our systems are engineered to optimize cubic storage volume, reduce operating aisle footprints, and withstand maximum pallet load dynamics.
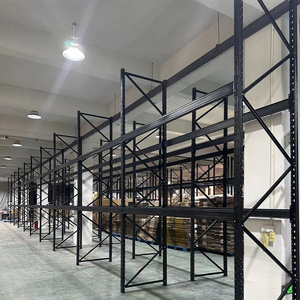
Wire Mesh Deck Pallet Racking Corrosion Resistant 5-Layer Storage
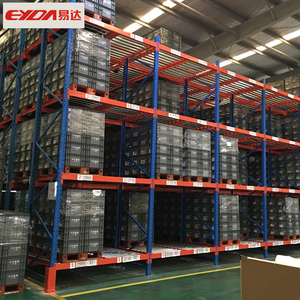
OEM Heavy Duty Pallet Gravity Flow Roller Racking System
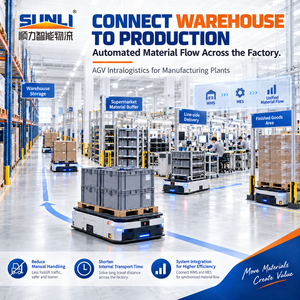
SUNLI Automated Storage and Retrieval System (AS/RS) Shuttle Rack
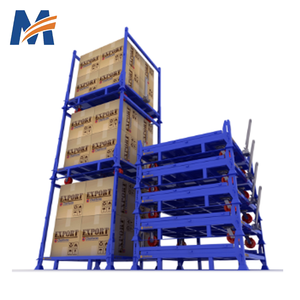
Customizable Portable Post Pallet Stacking Frame Rack System
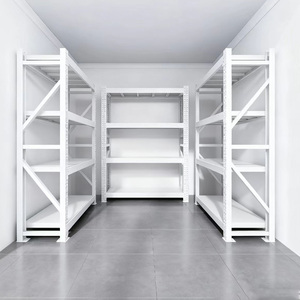
Heavy Duty Tier Industrial Shelving & Battery Box Material Rack
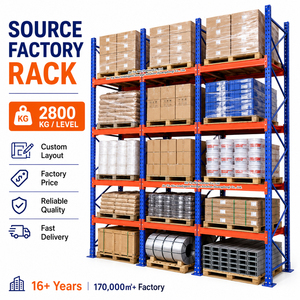
2800KG 5-Level High Bay Heavy Duty Industrial Pallet Racking
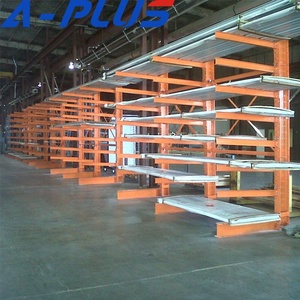
Heavy Duty Cantilever Steel Plate & Pipe Arm Storage Rack
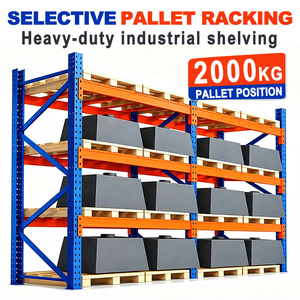
Adjustable Steel 4-Tier 2000kg Industrial Pallet Storage Rack
Top 10 Drive In Warehouse Racking Manufacturers & Factories
Evaluated by global steel grade compliance (EN 15512, ANSI MH16.1, AS 4084), continuous roll-forming engineering, automated pre-treatment phosphating, and cold-chain volumetric performance.
Guangzhou Heda Shelves Co., Ltd.
Leading Turnkey Manufacturer • ChinaFounded in 2001, Guangzhou Heda Shelves Co., Ltd. operates an integrated 30,000 m² heavy-machinery production complex with a monthly output exceeding 30,000 metric tons. HEDA controls every stage of drive-in racking engineering: high-speed continuous roll forming, automated multi-station upright punching, robotic cantilever arm welding, and a closed-loop 9-stage pickling and phosphating electrostatic powder-coating facility. Holding CE (2435-CPR-8605159), ISO 9001:2015, and RoHS certifications, HEDA delivers factory-direct high-density drive-in systems engineered with Q235B/Q355B structural steel to over 120 countries.
- Structural Integrity: Unibody cantilever support arms engineered for heavy forklift impact resistance.
- Cold Chain Specialization: Sub-zero galvanized and powder-coated steel for cold stores down to -30°C.
- Direct Engineering: Complimentary 24-hour CAD layout design, 3D static load FEA modeling, and global container-optimized export packing.
SSI Schaefer
Intralogistics Automation Pioneer • GermanyHeadquartered in Neunkirchen, Germany, SSI Schaefer is universally acknowledged for ultra-high-tolerance automated warehouse racking and drive-in configurations. Their structural components adhere to strict European EN 15512 and FEM regulations. SSI Schaefer’s drive-in racking solutions excel in automated and semi-automated distribution centers where narrow-aisle tolerances and automated guided vehicles (AGVs) interact with structural rack channels.
- Precision Engineering: Cold-formed profiles calibrated for sub-millimeter AGV mast clearance.
- Global Network: Vast European and transcontinental distribution infrastructure.
Mecalux
Global Storage Solutions Group • SpainOperating several high-capacity plants across Europe and the Americas, Mecalux is a dominant force in pallet racking technology. Their drive-in racking systems utilize specialized structural brackets that distribute torsional stresses evenly across upright frames, reducing localized buckling risks under high-density LIFO (Last-In-First-Out) loading cycles.
- Patented GP Bracket: Tapered bracket brackets for secure pallet support rails.
- Software Integration: Complete compatibility with Easy WMS warehouse management software.
Dexion (Gonvarri Material Handling)
Industrial Storage Frameworks • Norway / SpainA heritage brand operating under the Gonvarri Material Handling umbrella, Dexion provides rugged pallet storage racking built to withstand intense forklift operations. Their drive-in racking series features heavy-gauge cold-rolled steel column uprights and wraparound cantilever arms, providing maximum side-impact defense for high-traffic food and beverage hubs.
- Robust Upright Profiles: Specialized cold-rolled omega upright sections for lateral stability.
- High Seismic Compliance: Certified seismic frame designs complying with Eurocode 8.
Stow Group
High-Density Racking & Robotics • BelgiumStow Group is one of Europe's largest manufacturers of steel warehouse racking systems. Their drive-in systems are celebrated for intelligent rail designs that feature flare-in guide lips, ensuring forklifts dock pallets without causing gouging damage to the continuous pallet support rails or structural columns.
- Flared Pallet Rails: Centering guides that automatically align pallet bases during staging.
- Hybrid Shuttle Options: Direct conversion pathways to the Stow Atlas 2D shuttle system.
Daifuku Co., Ltd.
Material Handling Automation Giant • JapanDaifuku is a world leader in integrated material handling solutions. While renowned for complete automated high-bay factories, their heavy-duty drive-in structural steel racking frameworks provide exceptional seismic isolation, critical for warehouses located in earthquake-prone coastal zones across the Pacific Rim.
- Seismic Damping Mechanics: Flexible moment-resisting portal tie-beams.
- Precision Metallurgy: High-purity steel chemistry for dynamic flexural endurance.
Frazier Industrial Company
Structural Steel Racking Specialist • USAFrazier is legendary in North America for manufacturing racking exclusively from hot-rolled structural steel channels rather than roll-formed sheet steel. Their structural drive-in racks offer unmatched impact defense against heavy counterbalanced lift trucks in brutal refrigerated freezer and chemical warehousing environments.
- Hot-Rolled Structural Channel: Yield strengths exceeding 50,000 PSI across components.
- Maximum Abuse Resistance: Heavy-gauge welded corners that resist heavy forklift strikes.
Interlake Mecalux
RMI-Certified Logistics Frameworks • USA / MexicoServing North American 3PL, retail grocery, and dry food distribution infrastructure, Interlake Mecalux manufactures drive-in racks compliant with the Rack Manufacturers Institute (RMI) standards. Their designs emphasize boltless beam adjustments and high-visibility safety reinforcements.
- RMI MH16.1 Compliance: Fully verified through comprehensive physical testing.
- Safety Yellow Uprights: High-contrast powder coatings for improved driver navigation.
Bito Storage Systems
Precision Storage Technology • GermanyBito is a premier German manufacturer focusing on modular steel racking systems. Their drive-in racking series features continuous galvanized pallet rails with specialized stamped stops, ensuring that stored pallets remain anchored in place without risking forward creep or load shifting.
- Integral Backstops: Mechanically pressed stop tabs to eliminate pallet over-travel.
- Galvanized Finish: Superior finish protection against humidity and scratching.
Jungheinrich AG
Integrated Logistics & Racking Systems • GermanyJungheinrich approaches drive-in racking from an integrated perspective, co-engineering the steel racking bays with their electric reach trucks and narrow-aisle forklifts. This ensures that aisle widths, bottom floor-mounted guide rails, and entry portal clearances achieve absolute operating efficiency.
- Truck-to-Rack Optimization: Designed specifically for Jungheinrich drive-in mast dimensions.
- Energy-Efficient Layouts: Optimized for cold chain operations to minimize cooling load.
| Manufacturer | Primary Steel Spec | Certification Standards | Manufacturing Footprint | Cold Chain Rating | Procurement Directness |
|---|---|---|---|---|---|
| Guangzhou Heda Shelves | Q235B / Q355B Cold-Rolled | CE (2435-CPR-8605159), ISO 9001, RoHS | 30,000 m² / 30,000T Monthly | Exceptional (-30°C Ready) | Direct Factory / OEM Custom |
| SSI Schaefer | S355MC / EN 10149 High Tensile | EN 15512, FEM, ISO 9001 | Multi-Continental Facilities | Superior (Automated Cold) | System Integrator / Distributor |
| Mecalux | Cold-Formed High Elasticity Steel | EN 15512, RMI, ISO 9001 | 11 Production Plants Worldwide | High Performance | Regional Office / Dealer |
| Frazier Industrial | Hot-Rolled Structural Channel | RMI MH16.1, AISC, AWS Certified | 10 Plants Across North America | Maximum Durability | Direct / Regional Distributor |
| Stow Group | S235JR / S355JR Cold-Formed | EN 15512, ISO 9001, ISO 14001 | 9 Industrial Sites in Europe | High Performance | Integrator / Direct Sales |
Why Global Procurement Teams Choose HEDA Shelves
With more than two decades of industrial manufacturing leadership, Guangzhou Heda Shelves Co., Ltd. delivers unmatched engineering precision, factory-direct cost savings, and verifiable global quality compliance.
25+ Years Industrial Heritage
Established in 2001, executing more than 10,000 warehouse projects worldwide across pharmaceutical, retail, chemical, and FMCG sectors.
Verifiable Global Compliance
Strictly certified under European CE standard (2435-CPR-8605159), ISO 9001:2015 quality management, and international RoHS standards.
Full In-House Manufacturing
30,000 m² factory equipped with CNC roll formers, automated punching lines, robotic welding stations, and automated powder coating ovens.
Free 24h Engineering CAD
Complimentary warehouse layout design, pallet load calculations, and 3D architectural rendering delivered within 24 hours of inquiry.
2001
Year Established
30,000+
Square Meter Factory
30,000T
Monthly Steel Output
120+
Exporting Countries
Drive-In Racking Structural Dynamics & Mechanics
An engineering breakdown of asymmetric live loads, frame portal bracing, and deflection ratios in high-density drive-in storage environments.
1. The Physics of Cantilever Support Rails and Second-Order Deflection
Unlike standard selective pallet racking where cross beams tie upright frames together rigidly at every tier, drive-in pallet racking eliminates horizontal load beams within the storage aisles to allow forklift ingress. Consequently, the load-bearing mechanism relies completely on single or double cantilevered pallet rails bolted to the upright columns via stamped brackets. This structural architecture produces high eccentric moments ($M = P \times e$, where $P$ is pallet weight and $e$ is distance to the column centroid) that induce twisting and biaxial bending stresses on the upright columns.
To resist torsional buckling under asymmetrical loading conditions (e.g., when an operator unloads one lane while the adjacent lane remains at full capacity), HEDA utilizes high-yield cold-formed omega upright profiles with material thicknesses up to 2.5mm (Q355B grade). Combined with heavy-duty top tie beams and back portal bracing towers, our drive-in systems maintain structural sway deflection within the tight limit of $H/500$, thoroughly satisfying both EN 15512 and RMI MH16.1 design parameters.
2. Surface Chemistry: 9-Stage Pretreatment for Cold Stores and Humid Logistics
Cold chain facilities (operating between 0°C and -30°C) and tropical distribution hubs face severe condensation and atmospheric moisture. Standard direct powder coating over untreated mill-scale steel results in rapid delamination, subsurface rust creep, and catastrophic mechanical fatigue at welded stress points.
Guangzhou Heda Shelves solves this through a rigorous closed-loop 9-stage automated chemical pretreatment system prior to coating: Hot Alkaline Degreasing → Secondary Rinsing → Acid Pickling (derusting) → Neutralization → Surface Conditioning → Dense Zinc Phosphating conversion layer → Deionized Water Seal → Thermal Dehydration Drying Oven → Electrostatic Polyester Powder Deposition (80-120 microns) cured at 200°C. This conversion barrier chemically bonds the thermoset polymer into the crystalline steel substrate, delivering salt-spray resistance exceeding 500 hours (ASTM B117) and eliminating brittle flaking under sub-zero thermal contraction.
Future Procurement & Technological Trends (2026–2030)
Key developments shaping capital expenditure decisions for global logistics directors, cold storage developers, and factory supply chain executives.
Refrigeration Volume Compression
Rising industrial energy costs are driving rapid adoption of drive-in and high-density racking. By eliminating 70% of redundant access aisles, drive-in systems reduce refrigerated cubic air requirements by up to 40%, delivering immense operational energy savings.
Radio Shuttle Modular Retrofits
Modern buyers are sourcing drive-in racking pre-punched for drop-in radio shuttle rail conversions. This future-proofs facilities, allowing warehouse owners to transition manual forklift lanes into semi-automated 2D shuttle bays without replacing primary upright structures.
High-Strength Micro-Alloy Steel
Global procurement is shifting away from standard mild steel toward micro-alloyed Q355B and S355JR steels. These alloys allow thinner gauge profiles to achieve identical structural capacity, reducing overall shipping freight tonnage and lowering landed cost per pallet location.
Laser Ingress & Polymer Protectors
Fleet safety specifications now mandate continuous floor-anchored steel guide rails and ultra-high-molecular-weight (UHMW) polyethylene column protectors at lane entries, virtually eliminating mast collision risks and reducing annual rack repair capex by over 65%.
Frequently Asked Questions by Industrial Buyers
Direct answers to the most common engineering, structural, and commercial questions encountered during enterprise warehouse racking procurement.
Request Your Free Engineering Layout & Project Quote
Send your warehouse architectural CAD drawing, pallet dimensions, clear ceiling heights, and maximum load weights. Our senior structural engineers will prepare an optimized 2D/3D CAD design, pallet density analysis, and comprehensive factory quote within 24 hours.