Heavy Duty
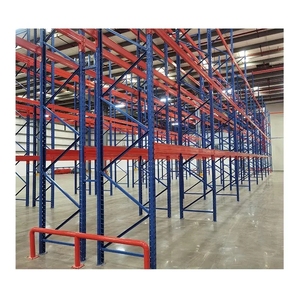
Heavy Duty Industrial Warehouse Pallet Racks
Engineered Q235B steel upright frames with 50mm-75mm adjustable connector pitches, certified for multi-tier heavy storage.
Engineered to integrate seamlessly with manual split-case picking, gravity-fed buffer lanes, and high-density industrial logistics operations worldwide.
Engineered Q235B steel upright frames with 50mm-75mm adjustable connector pitches, certified for multi-tier heavy storage.
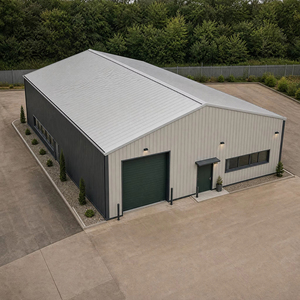
Hot-dipped galvanized or powder-coated structural steel engineered for extreme seismic stability and open-span staging.
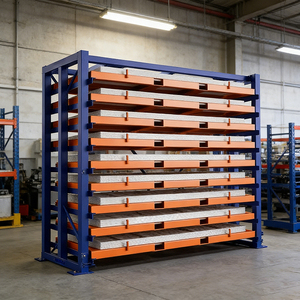
Ergonomic pull-out drawer mechanism allowing 100% overhead crane or forklift access for heavy plate materials and dies.
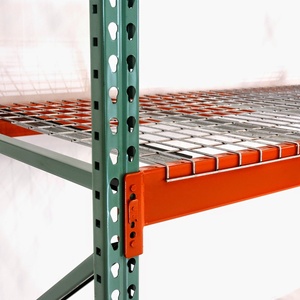
North American standard punch profile compatible with universal roll-formed components, boltless tool-free pin assembly.
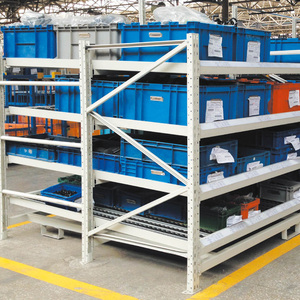
Engineered aluminum roller beds, anti-collision entry guides, and speed controllers ensuring strict first-in-first-out (FIFO) handling.
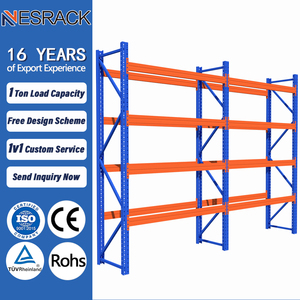
Cold-rolled steel deck panels with reinforced underlying ribs, offering 300kg-800kg distributed shelf capacity.
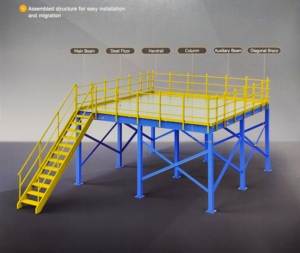
Doubles vertical cubic volume; integrates rack columns with walkable perforated or solid steel decks for order picking hubs.
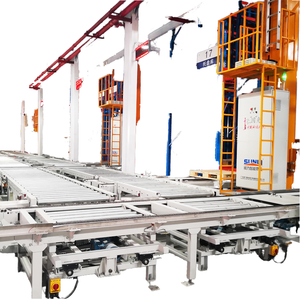
Micro-tolerance laser-welded racking structures built for robotic stacker cranes, high-speed bin shuttles, and WMS software integration.
A deep dive into structural kinematics, gravity flow mechanics, roller track engineering, and how precision-manufactured carton flow racks eliminate supply-chain bottlenecks.
Carton flow racking systems—frequently designated as dynamic pick frames or gravity carton feed systems—operate on an inclined plane utilizing low-friction roller tracks or skate-wheel tracks. By separating the replenishment aisle from the picking aisle, order selectors operate without interruption while restocking personnel continuously feed cases from the rear loading face.
The core physics revolves around the coefficient of rolling friction ($\mu_r$) balanced against gravitational slope angle ($\theta$). Standard corrugate packaging requires an inclination between 2.5% to 5% (approximately 1.5° to 3°). If the pitch is too shallow, cases experience frictional stall; if excessive, cartons accelerate uncontrollably, leading to impact crushing at the front retrieval face.
As premier OEM/ODM carton flow manufacturers, our engineering team custom-rolls high-grade steel to meet international structural integrity standards. Unlike off-the-shelf distributor offerings, OEM manufacturing enables precise steel specification, slot perforations, and protective chemical treatments adapted to specific industrial operational environments.
We utilize cold-rolled steel coils matching Q235B and Q355B structural grades. Upright frames are roll-formed through 18-stage computer-controlled forming stands, ensuring minimal torsion and micro-tolerances along multi-meter upright columns. Beams feature welded 3-claw or 4-claw connector brackets that lock into upright slots with positive-locking safety pins.
Direct physical metrics and system capabilities for warehouse project estimators, consulting engineers, and logistics procurement directors.
| System Architecture | Track Mechanism | Load Capacity (UDL) | Lane Pitch Range | Ideal Application / SKUs |
|---|---|---|---|---|
| Standard Drop-In Carton Flow | ABS or Polypropylene Skate Wheel | 50 – 150 kg / linear meter | 2.5% – 4.0% (1.5° – 2.3°) | Standard corrugated boxes, high-velocity e-commerce picking. |
| Heavy-Duty Roller Bed Flow | Continuous Steel/Aluminum Axle Rollers | 150 – 350 kg / linear meter | 3.0% – 5.5% (1.7° – 3.2°) | Heavy plastic totes, automotive engine components, industrial hardware. |
| Knock-Down Universal Track | Dual-flanged Polyethylene Wheels | 80 – 200 kg / linear meter | 2.0% – 4.5% (1.2° – 2.6°) | Third-party logistics (3PL) with rapidly shifting package dimensions. |
| Sub-Zero Cold Chain Dynamic Flow | Impact-Modified Nylon / Stainless Axles | 100 – 250 kg / linear meter | 3.5% – 6.0% (2.0° – 3.5°) | Frozen food fulfillment, pharmaceutical temperature-controlled cold vaults (-25°C). |
| ESD Safe Electronics Flow Rack | Conductive Carbon-Infused Wheels | 40 – 120 kg / linear meter | 2.0% – 3.8% (1.2° – 2.2°) | Semiconductor picking, PCBA assembly plants, cleanroom intralogistics. |
Analyzing industry transformations across automation convergence, warehouse real estate costs, and predictive replenishment technology.
Modern high-throughput distribution hubs no longer deploy static carton flow. Systems are manufactured with integral wiring raceways and pre-punched channel click-ins for Pick-to-Light (PTL) LED modules, IR presence sensors, and pick-confirmation light curtains, driving picking accuracy to 99.98%.
Procurement teams are shifting specs toward AMR (Autonomous Mobile Robot) compatibility. Rear-loading replenishment aisles are engineered with docking targets and standardized roller clearances, allowing autonomous tuggers to deliver replenishment totes directly to dynamic bed buffers without human intervention.
Rising industrial square-meter rental costs dictate vertical cubic expansion. Carton flow levels are increasingly built into the lower ground tiers of 2-tier and 3-tier rack-supported mezzanine floors, utilizing gravity for bottom-level high-velocity picking while holding bulk pallet replenishment directly overhead.
Over 25 years of relentless manufacturing rigor, certified international quality, and an integrated supply chain that delivers cost advantages straight from the factory floor.
Industrial storage systems represent substantial capital commitments where structural failure is impermissible. We operate under stringent quality management frameworks verified by international third-party certification bodies.
We believe engineering support must precede purchase contracts. Our team of in-house structural engineers works alongside your project team to calculate optimal lane density, beam deflections, and floor slab load requirements.
Essential technical queries encountered during the engineering review and purchasing stages of OEM/ODM carton flow projects.
Consult with our senior logistics structural engineering team. Submit your warehouse floor plan, SKU profiles, and required flow depths to receive an engineered layout, load calculation, and comprehensive quote package within 24 hours.