Certified Heavy-Duty Pallet & Stacking Rack Portfolio
Engineered from premium Q235B/Q355B structural steel, our export-ready rack architectures deliver load bearing capacities ranging from 400kg to over 3,000kg per storage tier, customized for distribution centers, manufacturing facilities, and automated logistics hubs.
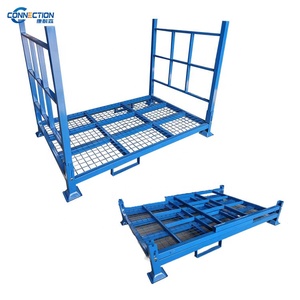
High Loading Capacity Steel Wire Mesh Pallet Foldable Stacking Rack
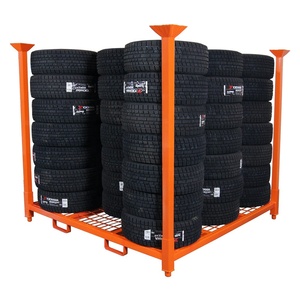
Detachable Stackable Pallet Tire Storage System 1000KG Powder
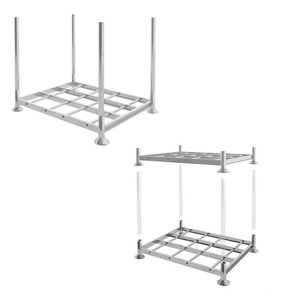
Heavy Duty Steel Pallet Racking Metal Truck Tire Pallet Rack
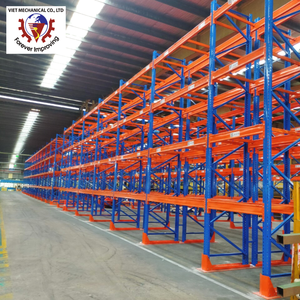
OEM Heavy Duty Steel Selective Pallet Storage Rack System
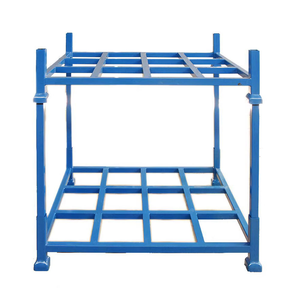
Adjustable Detachable Galvanized Post Pallet Stacking Rack
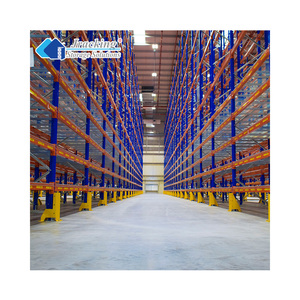
Dexion Pitch 76.2 mm Style Warehouse Beam Pallet Rack System
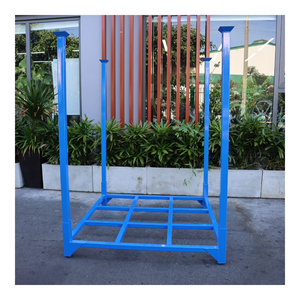
Foldable Steel Pallet With Collapsible Structure Frame
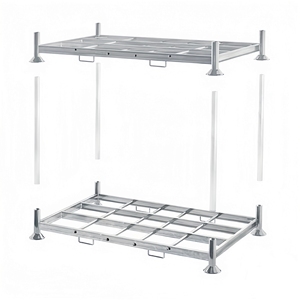
Heavy Duty Detachable Post Pallet Stacking Galvanized Rack
Structural Integrity & OEM Metallurgy in Industrial Pallet Racking
Modern warehouse logistics demands dynamic structural reliability far exceeding simple static weight accommodation. As premier custom OEM rack steel pallet rack factories and exporters, our manufacturing philosophy centers on the stringent application of structural mechanics, metallurgy control, and cold-formed profile optimization. Pallet rack failure is never a mere localized breakdown; it triggers catastrophic collapse cascades, crippling business operations and compromising personnel safety.
Our engineering division models racking arrays under multi-axial load combinations adhering to international standards including FEM 10.2.02 (European Design Code for Static Steel Pallet Racking), EN 15512:2020, ANSI/RMI MH16.1, and AS 4084-2023. Finite Element Analysis (FEA) simulates horizontal forklift impact shear forces, seismic drift, upright perforation stress concentrations, and beam deflection under asymmetrical loads. By selecting hot-rolled certified coils—primarily Q235B (Yield Strength $f_y \ge 235 \text{ MPa}$) for universal box beams and high-tensile Q355B ($f_y \ge 355 \text{ MPa}$) for deep-reach upright channels—we balance yield resilience with high ductile fracture margins.
Structural FEA Validation
Full-scale finite element stress modeling ensuring deflection does not exceed the stringent $L/200$ deflection threshold under maximum dynamic payload.
Multi-Rib Profile Geometry
Continuous roll-formed uprights incorporating 11-to-13 cold-folded bending edges to heighten post torsional rigidity against lateral torsion buckling.
Interlocking Connector Claw
Automated stamped 3-to-5 claw beam connectors fitted with spring safety locks, preventing unintentional beam dislodgement under violent upward forklift strikes.
Dual-Surface Coating
Acid pickling, zinc phosphating, and 80–120μm thermosetting epoxy-polyester powder baking, neutralizing atmospheric corrosion and saltwater mist.
Factory Direct Production Architecture: 10-Stage Precision Engineering
Unlike trading intermediaries that aggregate disparate components from disjointed workshops, our integrated Guangzhou production headquarters oversees an end-to-end quality ecosystem across a 30,000 m² footprint. Every component traces directly back to raw coil mill test certificates (MTC).
Strategic Procurement Trends: How Warehouse Operators Must Source Racks (2025–2030)
The global storage equipment supply chain is undergoing profound shifts driven by automated material handling (AMH), near-shoring strategies, volatile steel commodity indices, and rigorous ESG carbon disclosure regulations. Procurement directors moving away from commoditized "per-ton" purchasing toward total life-cycle value (TCO) are centering strategies on four primary technical transitions:
1. ASRS & Shuttle-Ready Adaptive Tolerances
Manual forklift operations allow for minor vertical and horizontal beam sags. However, the rapid ascent of automated four-way radio shuttles and Automated Guided Vehicles (AGVs) requires structural tolerances measured down to ±1.0mm. Forward-looking procurement demands racks fabricated with automated CNC laser positioning to avoid sensor misreads and optical misalignment during autonomous 24/7 pallet transfer.
2. Climatic Metallurgy & Cold-Chain Expansion
With pharmaceutical and fresh-food cold storage expanding globally, steel brittleness at sub-zero environments (-25°C to -40°C) presents severe structural safety hazards. Procurement requires Charpy V-notch impact-tested steel grades combined with pre-galvanized or hot-dip galvanized finishes (HDG) that eliminate the flaking, peeling, and thermal micro-cracking common to standard coatings.
3. CBM-Optimized Knockdown (KD) Engineering
Ocean freight fluctuations require OEM exporters to design nesting profiles and modular knockdown frameworks. By designing patented bolted upright trusses, detachable post pockets, and nesting wire-mesh decks, top-tier factories achieve up to 35% higher cubic container volume (CBM) utilization in 40HQ containers, slashing the landed shipping cost per pallet position.
4. Transparent Traceability & E-E-A-T Compliance
Tier-1 contractors and structural consultants reject unverified commodity steel. The modern procurement standard demands verifiable third-party certification: CE marking under EN 1090-1 / CPR No. 2435-CPR-8605159, ISO 9001:2015 quality frameworks, RoHS compliance, and mill-certified chemical compositional logs directly tied to every delivery lot.
Guangzhou HEDA Shelves: 25+ Years of Export Manufacturing Excellence
Operating continuously since 2001, Guangzhou HEDA Shelves Co., Ltd. has evolved from a specialized metal fabrication workshop into an international benchmark for warehouse storage solutions. With an annual steel transformation exceeding 360,000 metric tons, we bridge the gap between heavy structural engineering and precision industrial customization.
Complimentary 2D/3D CAD Engineering
Our 30+ project engineers generate complete architectural layouts, clearance audits, picking route flowcharts, and 3D architectural renders within 24–48 hours of initial enquiry.
Global Port Logistics Logistics Footprint
Routine direct export shipments to over 120 countries, with specialized routing to Nhava Sheva, Chennai, Chattogram, Karachi, Colombo, Singapore, Rotterdam, Long Beach, and Santos.
OEM & Private Label Customization
Custom perforation configurations (Dexion 76.2mm, teardrop 50.8mm, European 50mm pitch), custom RAL color powders, embossed client logos, and container loading prioritization.
Industrial Pallet Racking FAQ
In-depth technical answers addressing load calculations, seismic zones, metallurgy certifications, and containerized export procedures.
Request an Engineered Layout & Comprehensive Technical Catalog
Accelerate your warehouse throughput and square-meter ROI. Connect directly with our Guangzhou design engineering department to receive free 2D/3D CAD layouts, finite element load reports, and verified factory-direct pricing for your next project.