Strategic Engineering & High-Density Steel Storage Infrastructures
An authoritative analysis of heavy-duty cold-formed steel racking systems, load dynamics, seismic performance, and turnkey automated handling across modern manufacturing environments.
Top Heavy-Duty Racking Systems for Production Facilities
Precision-fabricated load-bearing racking lines engineered to resolve raw material staging, buffer stock balancing, automated picking, and extreme vertical density challenges.
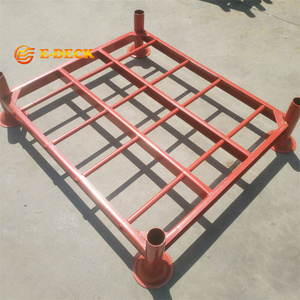
Heavy-Duty Steel Metal Logistic Stackable Storage Post Pallet Racks
Modular post-pallet units allowing free layout reconfigurations, safe dynamic stacking up to 4-tiers, and rugged transit capability for heavy raw casting parts.
View System Specs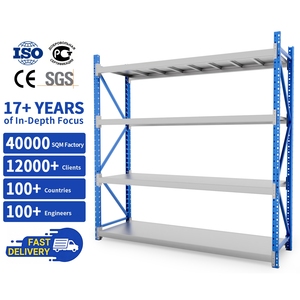
Industrial Selective Pallet Racking System for Multi-SKU Storage
Precision-punched teardrop and omega-profile uprights delivering 100% direct pallet selectivity for pharmaceutical cleanrooms, medical manufacturing, and retail hub logistics.
View System Specs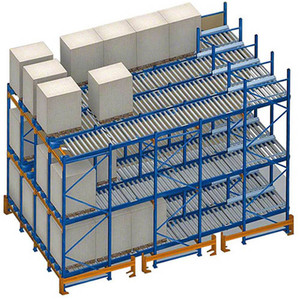
Gravity Pallet Racking Heavy-Duty Roller Dynamic Flow System
Sloped roller tracks utilizing gravitational acceleration with integrated speed controllers to maintain frictionless, automatic FIFO replenishment for high-throughput perishables.
View System Specs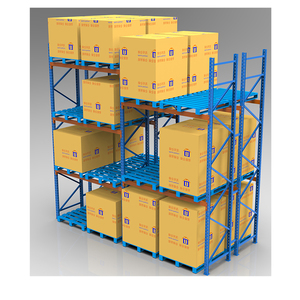
Single Deep Selective Rack Heavy-Duty Industrial Structural Framework
Heavy roll-formed continuous box beams combined with high-yield strength Q235B/Q355B steel, designed to withstand intense counterbalanced forklift traffic.
View System Specs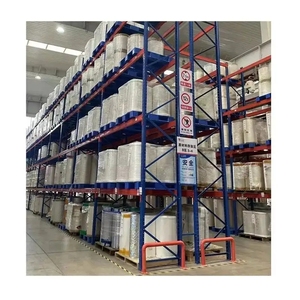
Adjustable Heavy-Duty Steel Warehouse Pallet Shelving System
Pin-point beam adjustment on 50mm/75mm hole pitches with high-load locking pins, engineered for facilities with high SKU profile variability and seasonal shifts.
View System Specs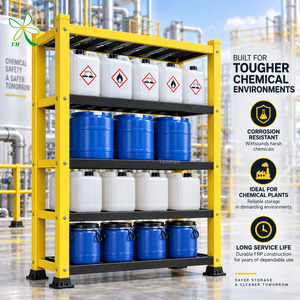
Electrical Insulation FRP Workshop Non-Conductive Storage Rack
Corrosion-proof fiber reinforced polymer composition ensuring zero electrical conductivity, spark resistance, and chemical resilience for battery plants and explosive processing bays.
View System Specs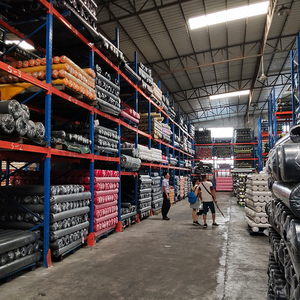
Heavy-Duty Customized 1000KG-5000KG Free Design Structural Rack
Engineered for extreme localized point-loading, integrating column footguards, guide rails, wire mesh decking, and seismic back-bracing tailored to high-density machinery dies.
View System Specs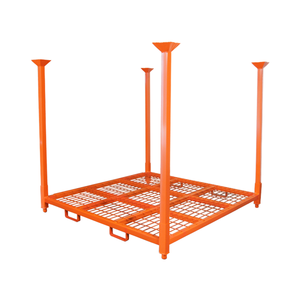
Corrosion-Protected Modular Steel Stacking Racks (Powder Coated)
Multi-stage pickling and phosphating pretreated steel frames coated in heavy-duty thermoset powder finishes to resist high moisture, salt fog, and aggressive factory atmospheres.
View System SpecsStructural Engineering Benchmarks: Cold-Formed Steel Dynamics in Production Warehousing
Modern industrial processing plants, discrete assembly facilities, and raw-material hubs cannot operate on generic storage approximations. Warehousing within large manufacturing facilities demands rigorous structural load calculation models. Racks act as unbraced or semi-braced vertical structures subject to compound mechanical forces: static dead loads, dynamic live pallet loads, forklift impact forces, and regional seismic stresses. As a top Chinese manufacturer, HEDA Shelves addresses these engineering realities through advanced finite element analysis (FEA), high-grade Q235B and Q355B cold-formed coil steels, and precision automated punch lines.
Structural reliability depends on beam-to-column connector rigidity. Unlike basic bolted joints that work loose under thermal expansion or continuous cyclic loading, our proprietary hook-in multi-prong connector brackets create an interlocking semi-rigid node with a high moment of resistance. Every upright section undergoes automated continuous roll-forming to retain high residual yield strengths, maximizing section modulus while reducing unnecessary dead weight. When designing for complex factory floor slabs where soil bearing capacities or rebar configurations are inconsistent, our engineering team tailors base plate surface areas, chemical anchor depths, and floor tie patterns to dissipate concentrated point loads safely across the slab.
Surface Protection Chemistry: Defeating Tropical Monsoons and Chemical Corrosion
A primary failure point of warehouse racking in coastal and tropical manufacturing zones (including the damp manufacturing corridors of South Asia, Southeast Asia, and maritime export zones) is premature micro-corrosion beneath the paint film. Cheap racking producers routinely apply spray paint directly over mill oil or scale. At our 30,000 m² Guangzhou production facility, every batch of steel profiles undergoes a strict 10-stage preparation sequence:
- Immersion Degreasing & Acid Pickling: Completely strips mineral scale, surface oxidation, and factory contaminants down to the virgin metallic crystal substrate.
- Micro-Crystalline Zinc Phosphating: Chemically bonds an insoluble inorganic protective film across the profiled steel surface, providing galvanic passivity and creating anchor peaks for organic coatings.
- Automated Electrostatic Thermoset Powder Deposition: Pure polyester and epoxy hybrid resin powders are uniformly atomized at 60-80 kV, forming an unbroken 60-90 micron protective shell cured in baking ovens at precise temperatures.
This rigorous chemical protocol prevents micro-cracking, under-film corrosion creep, and beam flaking even in ambient manufacturing environments with high sulfur emissions, humidity, or aggressive solvent vapors.
Future Procurement & Technological Trends in Industrial Storage
How the interplay of robotics, vertical airspace maximization, and volatile supply chains is reshaping factory racking investments globally.
1. Convergence of AS/RS & Radio Shuttle Dense Storage
The skyrocketing cost of industrial manufacturing real estate has rendered traditional wide-aisle storage financially obsolete. Factories are transitioning to semi-automated radio shuttle bays and fully automated multi-deep crane systems that operate inside tight 1,400mm lanes, boosting storage capacity by over 65% in existing envelopes.
2. Integration of Digital Twins & IoT Structural Telemetry
Next-generation racking infrastructures incorporate strain gauge telemetry and optical deflection sensors. Plant operations can monitor real-time beam sagging, dynamic overload warnings, and undocumented seismic displacements via centralized building management interfaces.
3. Modular Reconfigurability for Rapid Retooling
Modern factories face shorter product lifecycles. Racking procurement contracts now favor modular, boltless beam adjustments, demountable cantilever systems, and structural mezzanines that can be expanded horizontally or vertically without structural welding or facility shutdowns.
4. Decarbonized Steel Metallurgy & Circular Supply Chains
Corporate ESG obligations are reshaping vendor qualification. Tier-1 manufacturers require certified high-strength, low-carbon cold-formed alloys. Higher tensile strengths reduce total structural steel tonnage while fulfilling strict European FEM and American RMI structural design criteria.
5. Strict Hybrid Protection for Multi-Climate Cold Stores
With pharmaceutical manufacturing and frozen food processing expanding in developing countries, cold-store racking specifications are shifting from purely painted components to hybrid hot-dip galvanized uprights combined with cold-temperature resilient low-alloy steels down to -30°C.
6. Turnkey Single-Source Supply Chain Accountability
Industrial procurement directors no longer divide layout design, steel fabrication, logistics dispatch, and local assembly between multiple sub-contractors. Sourcing directly from comprehensive manufacturers eliminates interface errors and guarantees end-to-end load ratings.
Enterprise Production Strengths & Engineering Credibility
Direct manufacturer capabilities supporting industrial procurement, multi-national distribution hubs, and heavy industrial plants worldwide.
Direct Manufacturer Control Since 2001
Over two decades of engineering excellence. We manage raw coil sourcing, high-speed automated roll-forming, precision robotic welding, and multi-stage pretreated powder coating inside our 30,000 m² factory footprint, producing over 30,000 tons every month with zero sub-contracting loopholes.
Documented International Certifications
Trust built on auditable compliance. Guangzhou Heda Shelves Co., Ltd. holds CE certification No. 2435-CPR-8605159, ISO 9001:2015 quality management system approval No. 18624Q00169R0M (verified through June 2027), and strict RoHS non-toxicity compliance for automated industrial warehouses.
Free Structural CAD & 3D Modeling
Eliminate project guesswork before committing capital. Our team of senior structural engineers reviews your architectural columns, slab capacities, and forklift specs to issue comprehensive 2D CAD floor plans, complete 3D structural renderings, and load stress safety calculations within 24 hours.
Container-Optimized Logistics & Fast Overseas Dispatch
We provide purpose-engineered, protective timber-free steel bundling that maximizes internal 40HQ ocean container volume, cutting landed freight costs per pallet position. Fast shipping options connect directly to major hubs: Nhava Sheva, Mundra, Chennai, Kolkata, Chattogram, Karachi, Colombo, Southeast Asia, the Middle East, and beyond.
Frequently Asked Questions on Factory Racking Procurement
Direct engineering answers addressing steel certifications, customized beam loading, seismic floor conditions, and export shipping procedures.
What exact architectural data is required to generate a valid CAD layout?
To produce an actionable layout and structural bill of quantities, our design engineering team requires your warehouse architectural drawing (AutoCAD DWG or scaled PDF) indicating clear ceiling heights, floor obstacles, overhead sprinkler clearances, concrete slab load limits, pallet footprint dimensions (width × depth × height including cargo overhang), gross pallet weights, and your forklift mast lift limits and turning radii.
How do HEDA Shelves systems withstand high-humidity, marine, or monsoon environments?
All fabricated structural steel profiles pass through a thorough chemical degreasing, ultrasonic acid pickling, and micro-crystalline zinc phosphating wash prior to electrostatic thermoset polyester powder coating. For exterior covered bays, open-sided factory sheds, or cold storage facilities, we offer hot-dip galvanized finishes certified to deliver extended service life without red rust formation.
Can your engineering team calculate structural racks for severe seismic zones?
Yes. Our engineering department applies international structural design codes (including European FEM 10.2.02 and US RMI guidelines). By analyzing your facility's local seismic coefficient, peak ground acceleration, and floor anchor tensile limits, we size the upright gauge, horizontal cross-bracing profiles, and heavy welded base plates to absorb lateral seismic shocks safely.
How do you verify load capacities and beam deflection limits prior to shipping?
Every beam-upright profile configuration is designed around a maximum deflection limit of L/200 under full design load conditions, backed by a safety factor of 1.5 to 1.8. Physical destructive testing and computer FEA simulations are conducted on our continuous cold-formed profiles to ensure zero non-elastic deformation occurs when operating under designated factory capacities.
What is the lead time for standard versus fully custom industrial racking orders?
Standard selective pallet racking and industrial longspan systems are typically manufactured, inspected, and bundled for export within 12 to 18 working days. Highly engineered structural mezzanine systems, automated radio shuttle bays, or custom high-capacity die storage racking (1,000kg to 5,000kg per shelf) typically require 20 to 28 days depending on total project tonnage.
Do you supply complete installation documentation and on-site assembly guidance?
Yes. Every overseas shipment is supported with detailed 3D exploded assembly diagrams, piece-by-piece numbered components, bolt torque schedules, and high-definition video walkthroughs. For large-scale manufacturing projects, HEDA Shelves can dispatch bilingual structural installation engineers to oversee on-site erection, anchoring, and final safety sign-off.
Transform Your Factory Storage Density Today
Connect directly with our engineering department. Share your warehouse floor plan, ceiling heights, and payload targets to receive an optimized 2D/3D CAD design layout, comprehensive load matrix, and competitive factory-direct quote.
Send an Inquiry