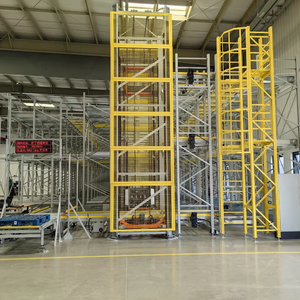
Intelligent Selective Pallet Rack With Conveying System
Integrated inline track guidance and automated pallet conveyor interface for high-frequency distribution centers.
Select from factory-calibrated mobile on-track systems, dynamic roller rail lines, and high-density push-back configurations built from certified Q235 structural steel.
Integrated inline track guidance and automated pallet conveyor interface for high-frequency distribution centers.
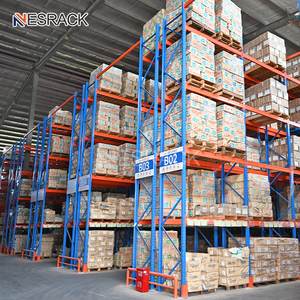
Adjustable multi-tier pallet storage with rapid beam locking mechanisms and floor guide rails for material handling vehicles.
Motorized rolling bases traversing embedded steel floor tracks, compacting footprint by eliminating fixed gangways.
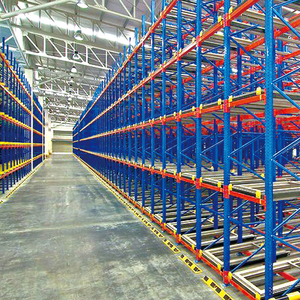
Inclined nested roller channels for deep lane LIFO picking, supporting loads up to 1,500 kg per pallet placement.
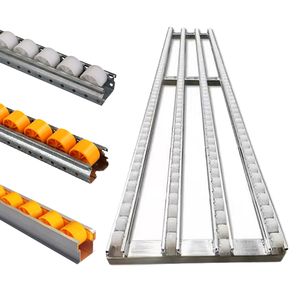
Reinforced aluminum sheet strip flow rails with heavy-duty roller wheels for continuous gravity-fed stock displacement.
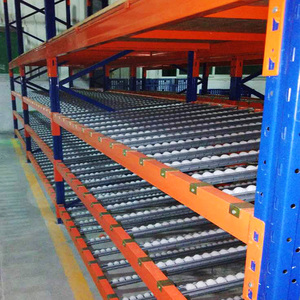
First-In First-Out (FIFO) gravity lane storage featuring centrifugal speed brakes and heavy structural guide stops.
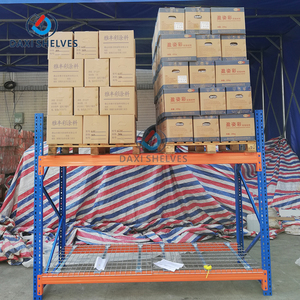
Cost-engineered mobile carriage designs built for rugged commercial cold storage, retail backrooms, and industrial logistics.
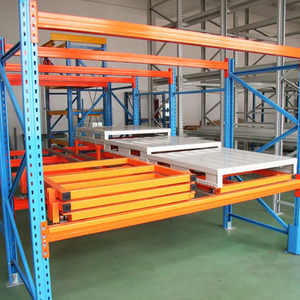
Certified Q235 structural steel push-back carriage system engineered for severe industrial payloads and zero maintenance down-time.
Discover why leading global supply chains transition from static selective frames to mechanically driven and gravity-operated track-guided racking systems.
Conventional selective storage commits upwards of 60% of slab area to forklift aisles. By mounting multi-tier upright assemblies onto mechanized bogie carriages traversing embedded or surface floor tracks, mobile on-track pallet systems compress access aisles into a single dynamically opened corridor. This instantly increases SKU storage capacity by 80% to 120% without acquiring additional industrial real estate.
Track systems demand uncompromising engineering tolerances. Heda Shelves fabricates precision cold-rolled profile guide rails embedded flush into warehouse slab toppings or secured via heavy chemical anchors. Featuring dual-flanged forged steel wheels, high-torque planetary geared motors, and synchronized drive shafts, our mobile bases eliminate skew and racking distortion under severe 30-ton bay loads.
Worker and cargo protection are prioritized in all dynamic track operations. Our on-track installations feature dual-channel photoelectric perimeter optical curtains, integrated infrared optical sweep sensors at chassis foot-level, emergency kick-plates, and collision-avoidance logic integrated directly into the master PLC switchgear cabinet, complying rigorously with EN 15095 and CE safety mandates.
| System Category | Track Mechanism | Stock Rotation Strategy | Payload Rating | Optimal Deployment |
|---|---|---|---|---|
| Track-Guided Mobile Racking | Motorized Bogie / In-Slab Guide Rails | 100% Direct Selective Access | Up to 30,000 kg / Mobile Block | Cold Storage Facilities, Pharmaceutical Hubs, High Land-Cost Warehouses |
| Dynamic Pallet Flow Racking | Gravity Roller Tracks with Speed Brakes | Strict First-In First-Out (FIFO) | 500 - 1,800 kg / Pallet Position | Fast-Moving Consumer Goods (FMCG), Perishable Food, High-Velocity Buffers |
| Nested Push-Back On Tracks | Telescopic Rolling Rail Carts | Last-In First-Out (LIFO) | Up to 1,500 kg / Position (2-6 Deep) | Medium SKU Diversity, Bulk Pallet Inbound Buffers, Floor Optimization |
| Conveyor-Integrated Selective | Inline Rail Transfer & AGV Floor Guides | System-Driven Dynamic Routing | Custom Heavy Engineering | Automated Logistics Hubs, Cross-Docking Terminals, E-Commerce Centers |
Strategic considerations for warehouse directors, supply chain managers, and 3PL procurement executives planning multi-decade storage infrastructure.
With industrial refrigeration accounting for substantial utility overheads, modern cold storage operations are rapidly adopting high-density mobile pallet racks on tracks. Maximizing the pallet positions per cubic meter of cooled air reduces per-pallet power consumption by up to 45%. Future procurement will heavily favor low-temperature-grade steel alloys and sealed drive mechanisms engineered specifically for sub-zero (-30°C) endurance.
Standalone mechanical push-button racking is transitioning into fully connected digital nodes. Procurement pipelines increasingly specify mobile racking controls that interface through standard Modbus, OPC-UA, or Industrial Ethernet directly with Warehouse Management Systems (WMS). Aisles automatically pre-open based on scheduled reach truck pick paths or Automated Guided Vehicle (AGV) routing protocols.
Historically, installing mobile track systems required casting specialized floor pits during initial construction. Future procurement trends demonstrate immense demand for surface-mounted low-profile rail systems and rapidly cut structural concrete recesses with micro-leveling leveling shims. This allows enterprises to convert existing leased warehouses into high-density track-based facilities with minimal disruption.
How advanced metallurgy, precision manufacturing automation, and integrated sensing are reshaping the capabilities of industrial racking platforms.
Transitioning from standard hot-rolled structural steel to ultra-high-yield cold-formed Q235 and Q355 micro-alloy steel configurations ensures optimal strength-to-weight ratios, reducing static deadweight on concrete floor foundations.
Advanced VFD smooth start-and-stop control algorithms eliminate abrupt carriage vibration on track rails, mitigating structural joint fatigue and preventing precarious stacked pallet loads from dislodging during high-speed transit cycles.
Continuous roll-forming lines with synchronized computerized punching deliver hole pitch accuracies down to ±0.1mm, ensuring effortless beam connector engagement, structural parallelism, and minimal rolling resistance across extended rails.
Rigorous 10-step pickling, surface phosphating, and heavy-duty thermosetting electrostatic powder coating protect upright columns and base bogies against aggressive industrial moisture, battery vapors, and coastal ocean air.
Clear, engineering-backed answers addressing the most common technical and operational considerations raised by international warehouse planners.
Mobile on-track systems transfer concentrated wheel loads to the concrete foundation. Warehouses typically require a floor slab meeting DIN 18202 or ASTM E1155 flat floor ratings (FF/FL values). Heda Shelves supplies specialized leveling shims and embedded rail anchoring fixtures to account for slight slab variances during our precision laser-guided track alignment process.
Our engineering division runs detailed seismic finite-element analyses (FEA) compliant with RMI, FEM 10.2.07, and local building codes. Track carriages are equipped with mechanical anti-tip clamps that hook directly under the flange of the embedded guide rail, physically restraining high-bay frames from tipping during ground acceleration events.
In many instances, high-grade uprights and load beams can be salvaged and integrated into newly manufactured motorized bogies, provided the upright section profiles and weld details satisfy dynamic load ratings. Our structural engineering department reviews your existing fabrication blueprints and performs load-validation prior to re-engineering.
Gravity pallet flow tracks and push-back rail systems require minimal routine operational maintenance. We recommend quarterly visual inspections of roller bearing dust covers, clearance of floor debris from carriage channels, and annual torque checks on brake roller retention brackets to ensure uniform braking deceleration across deep lanes.
Roller and cart systems depend on consistent bottom board geometry. Defective, fractured, or excessively sagging wooden pallets can hang up on roller tracks. For operations handling mixed or non-standard pallets, we integrate continuous full-width steel rollers or equip push-back carts with multi-point support grilles to ensure consistent travel.
Standard project cycles from structural CAD final approval to port container dispatch span 20 to 35 business days. We coordinate complete sea-freight bundling directly from our factory loading bays in Guangzhou to major worldwide seaports, optimizing container cube utilization to lower landed unit costs.
Founded in 2001, Heda Shelves represents an internationally proven tier-one manufacturer of advanced warehouse racking, heavy industrial shelving, and multi-tier structural mezzanines.
We control every phase from certified steel coil slitting, cold roll-forming, computerized column punching, robotic welding to industrial automated powder coating, ensuring total traceability and dimensional consistency.
Our manufacturing infrastructure is accredited under CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Quality Management System No. 18624Q00169R0M, guaranteeing strict compliance with international structural standards.
With over 10,000 projects completed across Southeast Asia, the Middle East, Europe, the Americas, and Africa, our logistic specialists pack and bundle components for safe long-distance multimodal sea voyages.
Send us your warehouse slab schematics, forklift fleet specs, and SKU profiles. Our engineering team returns fully detailed, optimized 2D CAD architectural plans and 3D visual renderings within 24 to 48 hours.
Connect directly with Guangzhou Heda Shelves factory engineers to evaluate your storage footprint, verify floor slab suitability, and receive an engineering proposal with complete structural calculations.