Engineered Heavy Duty Storage Systems Portfolio
Explore our certified line-up of industrial storage racks manufactured from certified Q235B and Q355B structural steel, precision-engineered to withstand heavy static loads, dynamic forklift operations, and harsh ambient conditions.
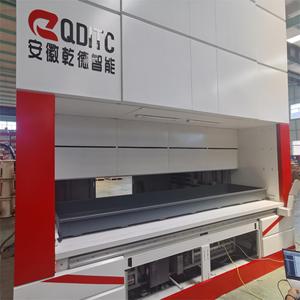
Industrial Stacking Racks Shelves-Mobile Durable Alloy Steel 15000kg Load Capacity Space-Saving Warehouse Storage System
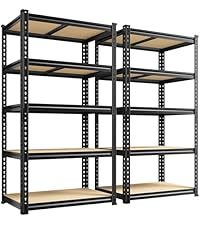
5 Layer Industrial Storage Shelving Racks Heavy Duty Adjustable Boltless Rivet Rack Corrosion Protection Warehouse Powder Coated
Grids For Food Industry Commercial Bakery Equipment Metal Wire Rack System
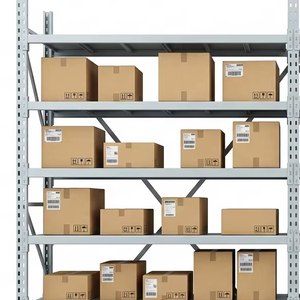
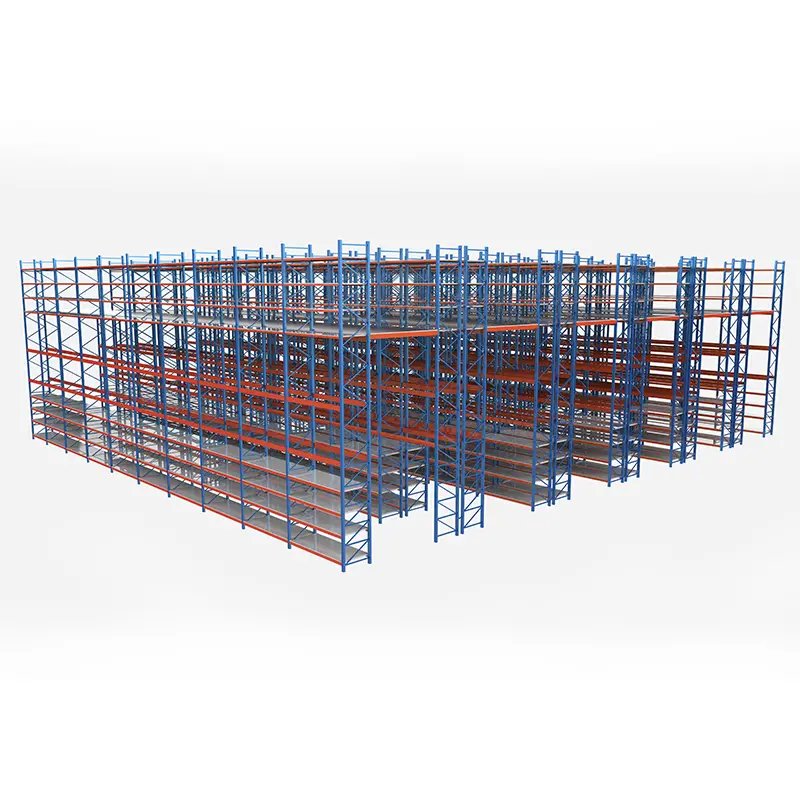
Customized 3-Layer Cold Rolled Steel Heavy Duty Epoxy Powder Coated Mezzanine Platform Pallet Shelving High Capacity Rack
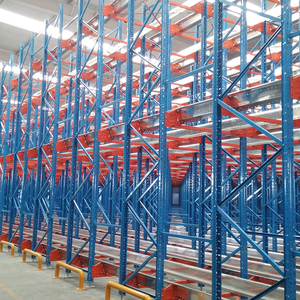
High Density Warehouse Automatic Radio Shuttle Rack Shelves Storage Racks Heavy Duty Pallet Racking Radio Shuttle Racking System
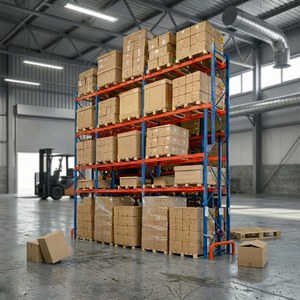
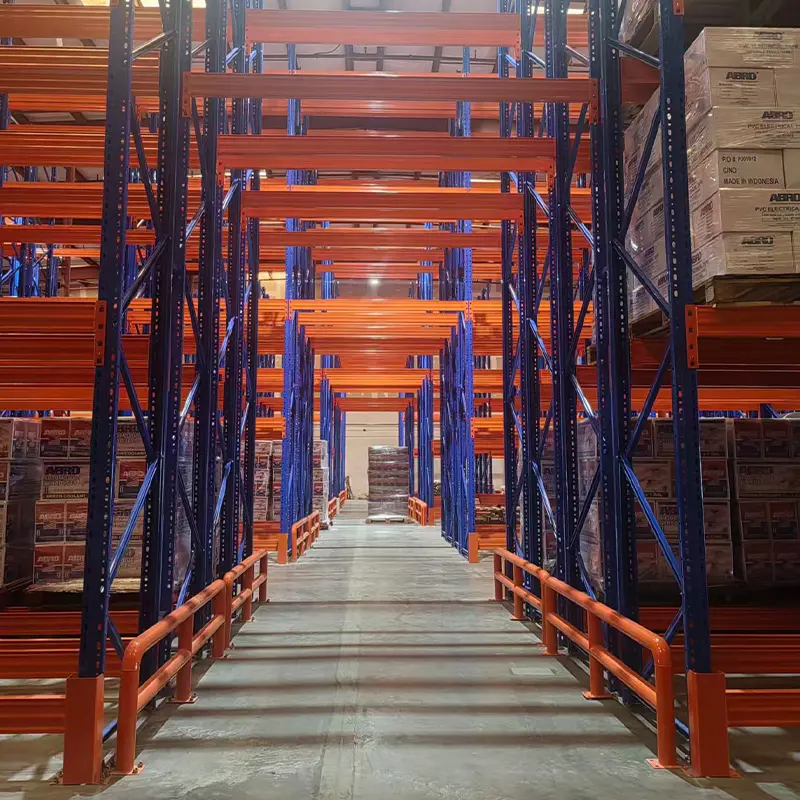
Customized Heavy-Duty Steel Warehouse Pallet System Industrial Racking Pallet Rack Shelving For Industrial Shelves
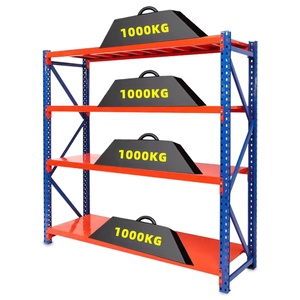
1000kg 2000kg 3000kg Per Layer Heavy Duty Cold Rolled Steel Epoxy Powder Coated Pallet Racking System For Factory Warehouse
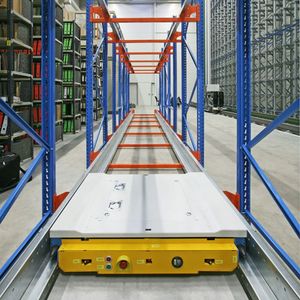
Heavy Duty Industrial Warehouse Radio Shuttle Racks Intensive Warehousing Pallet Racking Cargo & Storage Equipment Manufacturer
Structural Integrity, FEA Calculations & International Standards
Industrial pallet racking is fundamentally an unbraced or semi-braced steel building structure subjected to dynamic operational loads, material handling equipment impacts, and localized seismic forces. As a Tier-1 China exporter and manufacturer, our engineering methodology adheres rigidly to three cornerstone global benchmarks: European Standard EN 15512:2020 (Steel static storage systems – Adjustable pallet racking systems – Principles for structural design), the American RMI ANSI MH16.1, and the FEM 10.2.02 / 10.2.09 codes.
Every racking configuration begins with precision Finite Element Analysis (FEA). We analyze structural buckling, torsional-flexural deformations, and beam deflection under full static and rated operational conditions. Beams are calculated to limit maximum vertical deflection under full working load to strictly less than L/200 (where L is clear beam span), ensuring zero permanent plastic deformation and complete stability of overhead pallet loads.
The connector claws are robotically welded with triple-groove safety hooks that incorporate automatic safety locking pins. This eliminates accidental dislodgement when forklift tines elevate pallets during rapid fulfillment cycles. Anti-corrosive performance is ensured via a comprehensive nine-stage pre-treatment wash (degreasing, acid pickling, and iron phosphating) followed by an automated electrostatic polyester powder coating cured at 190°C–200°C, offering salt spray resistance exceeding 500 hours according to ASTM B117 standards.
Engineering Compliance Checklist
Prior to production sign-off, every international shipment undergoes physical stress verification and computerized simulation matching target warehouse geotechnical data.
- Seismic Zone Calibration: Calculated in accordance with UBC / IBC standards, optimizing base-plate anchor dimensions and upright thickness for zones 1 through 4.
- Punching Precision: 50mm or 75mm continuous CNC pitch tolerance maintained within ±0.1mm, ensuring effortless level reconfigurability.
- Cold-Chain Annealing: Cryogenic testing for cold-storage installations operating at sub-zero temperatures (-25°C to -35°C) to prevent steel embrittlement.
- Third-Party Destructive Testing: Upright stub-column compression tests and beam-end connector lozenge tests periodically audited by SGS and TÜV.
Industrial Racking Trends & Next-Gen Procurement Drivers
Global warehouse real estate pressures, soaring land valuations, and rising labor costs are rapidly reshaping the specification sheets of supply chain executives. Here are the core procurement vectors driving capital expenditures through 2030.
Semi-Automated Shuttle Primacy
Traditional deep-lane Drive-In racking is being actively replaced by Radio Shuttle Racking Systems. By decoupling forklift operators from internal rack lanes, shuttle systems slash pallet cycle handling times by 40%, completely prevent forklift-upright collision damage, and support dynamic transition between FIFO (perishables) and LIFO (general manufacturing buffer).
Vertical Multi-Tier Exploitation
With industrial building rents climbing globally, logistics hubs are shifting focus to multi-tier Rack-Supported Mezzanine Platforms. Instead of incurring heavy civil engineering and brick-and-mortar expansion costs, enterprises are doubling and tripling operational cubic meters, running automated parcel sorting and micro-fulfillment above bulk pallet reserves.
Cold Chain HDG Engineering
Pharmaceutical cold storage and blast-freezing operations require superior resilience against thermal contraction and moisture-induced corrosion. Sourcing teams are migrating from standard wet paints to advanced hot-dip galvanized (HDG ISO 1461) zinc coatings or dual-stage hydrophobic epoxy powders that do not micro-fracture at -30°C.
Modular Boltless Reconfigurability
Agile 3PL operations handling short-term client contracts require high adaptability. Procurement contracts now demand boltless upright-to-beam connectors with teardrop or omega interlocking slots, enabling warehouse crews to reposition beam levels in 15-minute intervals without structural weld cutting or shutdown downtime.
Heavy Duty Storage Architecture Comparison Matrix
Compare spatial density, mechanical accessibility, cycle throughput velocity, and capital intensity to evaluate the optimal configuration for your operational inventory profile.
| System Architecture | Pallet Selectivity | Floor Space Utilization | Stock Rotation | Floor Load Profile | Automation Readiness | Ideal Industry Use-Case |
|---|---|---|---|---|---|---|
| Selective Pallet Racking | 100% Direct Access | 35% - 40% | FIFO / LIFO Flexible | Standard Slab (3-5 T/m²) | Manual / Reach Truck | General 3PL, FMCG, Spare Parts |
| Radio Shuttle System | Lane Dependent (Dense) | 75% - 85% | Dual Mode (FIFO/LIFO) | Reinforced Slab (>5 T/m²) | Semi-Automated PLC | Cold Storage, Food & Beverage, Raw Bulk |
| Drive-In / Drive-Thru | Restricted Lane Access | 65% - 75% | Strict LIFO (Drive-In) | Standard Slab with Guide Rails | Manual Forklift In-Aisle | Low-SKU, Seasonal Harvest, High-Volume |
| Rack-Supported Mezzanine | Mixed (Pallet + Bin Pick) | 90% Vertical Utilization | Multi-Channel Flow | High Bearing Capacity Slab | Conveyor / Lift Integratable | E-commerce, Apparel, Automotive Spares |
| Heavy Duty Cantilever | 100% Frontal Linear Access | 50% - 60% | Open Rotation | Heavy Concrete Foundation Pad | Side Loader / Forklift | Steel Tubing, Timber, Extrusions, Rebar |
Guangzhou HEDA Shelves: 25+ Years of Manufacturing Leadership
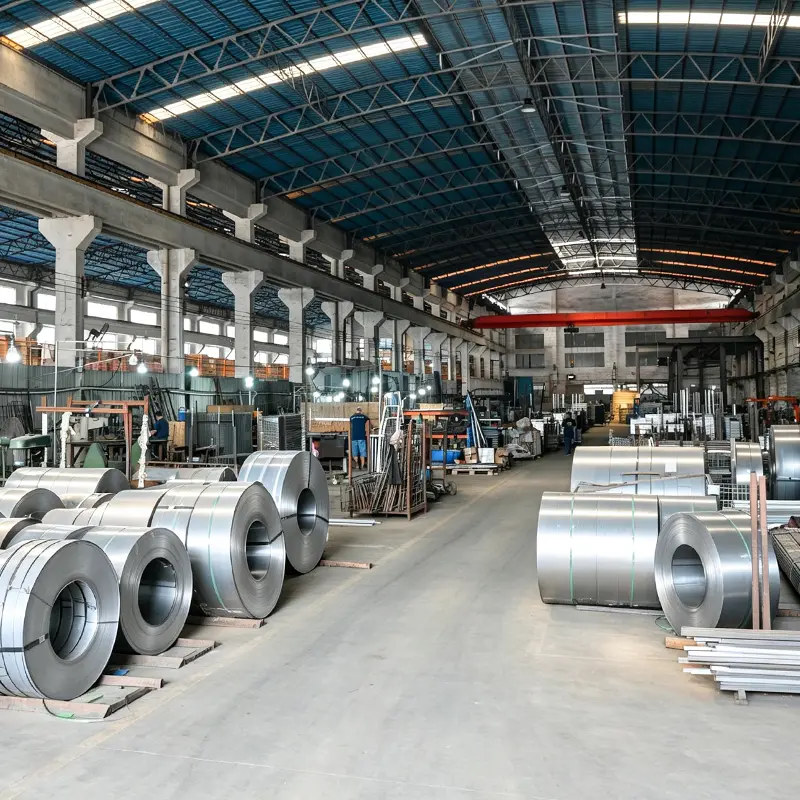
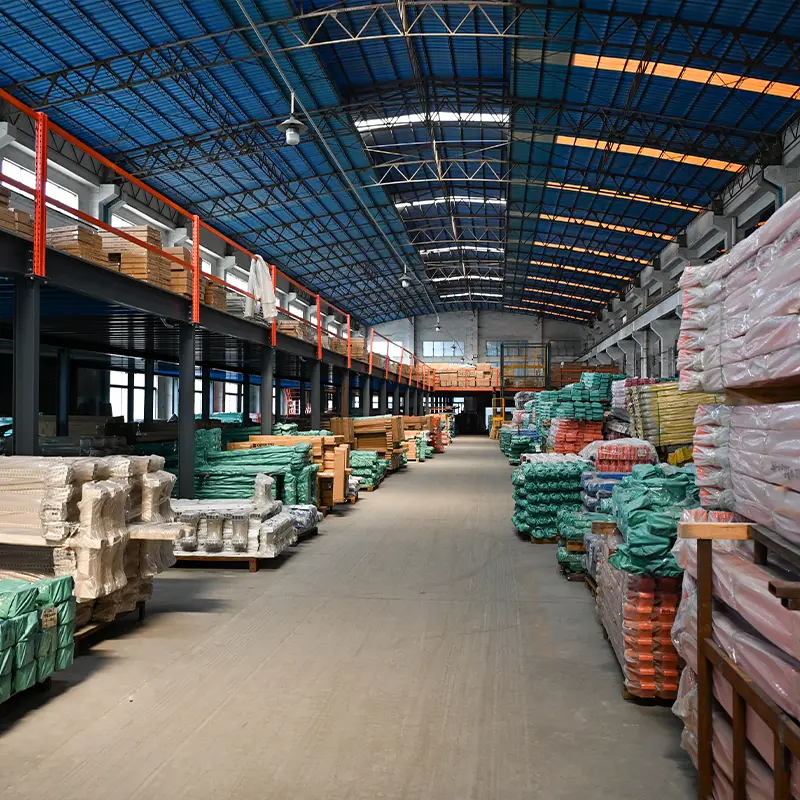
Headquartered in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. operates one of the nation's premier automated production complexes dedicated entirely to heavy-duty material handling and warehouse racking infrastructure.
10-Stage Manufacturing & Pre-Treatment Workflow
From prime steel coil arrival to final container stuffing, every rack member follows our proprietary, fully documented ten-stage industrial manufacturing protocol.

Raw Material QC
Spectrometric assay & ultrasonic flaw detection on prime coil stock.

Precision Cutting
High-speed slitting lines cut coil stock to exact engineering widths.

CNC Column Punching
Continuous CNC multi-ton presses guarantee ±0.1mm hole alignment.

Cold Roll Forming
Continuous 24-station rolling adds longitudinal load rigidity.

Profile Calibration
Box beam and upright profiles straightened to prevent camber distortion.

Edge Deburring
Mechanical edge rounding protects logistics handlers and goods.

Robotic Welding
Automatic gas shielded CO² arc welding for high-strength connector heads.

Pickling & Phosphating
Nine-tank chemical dip eliminates mill scales and oxidization rust.

Powder Coating & Cure
GEMA electrostatic guns provide even 70–90μm durable thermoset layer.

Bundling & Export Stuffing
Cushioned steel strapping and 40HQ container optimization packing.
Frequently Asked Questions on Heavy Duty Industrial Racking
Comprehensive engineering, regulatory, and logistics answers addressing the direct evaluation criteria of B2B project managers, warehouse engineers, and international procurement officers.
How are maximum beam load ratings and vertical deflections verified?
Every load specification published by HEDA Shelves is computed based on uniformly distributed loads (UDL) conforming to EN 15512:2020 and RMI MH16.1. Beam deflection is restricted to maximum 1/200th of clear length under working limit states. In physical validation, test beams undergo 1.5 times safety margin overload tests to ensure zero permanent weld cracking or structural deformation.
What specific floor slab specifications are required for heavy pallet racking?
Standard installations carrying 1,000kg to 3,000kg per level generally require a reinforced concrete slab with minimum thickness of 150mm to 200mm and compressive strength of C20/25 or higher (minimum 25 MPa). For high-bay radio shuttle or heavy mezzanine platforms exceeding 6 meters, our engineering team requires concrete core test data and joint layout to position base plates and M12/M16 chemical or expansion anchors away from control joints.
How does HEDA prevent rust and corrosion in coastal or tropical climates?
Prior to coating, steel members undergo immersion in nine chemical pre-treatment baths to completely remove mill scale, grease, and surface oxidation, followed by zinc phosphate passivation. We then apply pure polyester powder cured at 200°C with film thickness of 70–90μm. For coastal port cities (such as Chennai, Colombo, or Chattogram) and cold storage sheds, we offer pre-galvanized or hot-dip galvanized steel components.
What is the typical manufacturing lead-time and container export arrangement?
Standard pallet rack orders (1 to 5 container loads) are fabricated and surface-treated within 15 to 20 working days. Custom mezzanines or automated radio shuttle systems require approximately 25 to 30 days including trial pre-assembly. We offer FOB, CIF, CFR, and DDP terms, routing containers from Nansha or Shenzhen ports to global destinations with comprehensive export bundling to eliminate transit friction scratches.
What documentation is provided to satisfy local building control inspectors?
We supply a complete documentation binder with every project: official Certificate of Conformity for CE (2435-CPR-8605159), ISO 9001:2015 quality control records, steel mill 3.1 chemical and physical test certificates, stamped structural calculation sheets (stress, bending moment, and deflection diagrams), and detailed CAD installation drawings with component identification tags.
Can our local contractors install HEDA racking systems independently?
Yes. Over 90% of our export clients utilize local installation contractors. We supply numbered components corresponding to colored 3D exploded layout blueprints and step-by-step video manuals. In addition, our senior project engineers are available for remote video guidance or on-site supervision for large-scale logistics centers.