Industrial Pallet Racking & Multi-Tier Storage Solutions
Engineered from premium hot-rolled and cold-formed coil steels (SS400, Q235B, Q355B), automated punching with precision pitch control, and electrostatically cured anti-corrosion finishes.
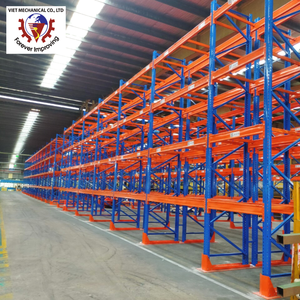
OEM Heavy Duty Steel Selective Pallet Rack Vietnam Wholesale Stainless Storage Rack For Warehouse Use
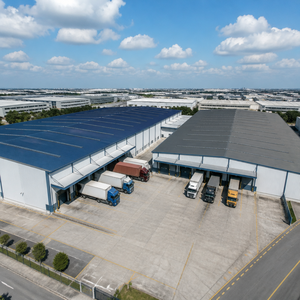
Large Scale Steel Warehouse Building High Bay Pallet Racking Storage Steel Frame Structure Design
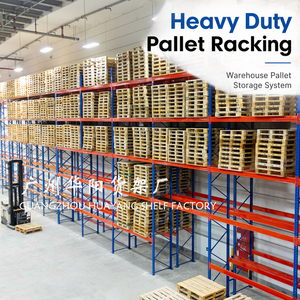
3000KG Per Level Heavy Duty Pallet Rack Industrial Warehouse Storage Steel Shelving Adjustable Pallet Racking System
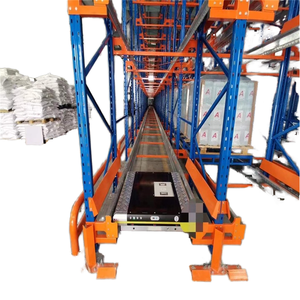
Automated Radio Shuttle Rack High Density Warehouse Storage System 2 Way Pallet Racking FIFO LIFO for Boxed Goods
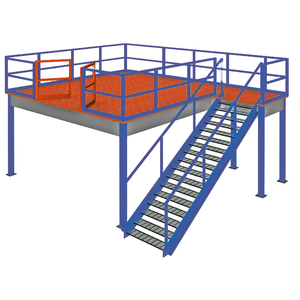
Industrial Warehouse Mezzanine Rack Steel Platform Loft Attic Rack Multi-Storey Storage System Heavy Duty Racking Solution
Heavybao Commercial Heavy Duty Brushed Stainless Steel Solid Wall Shelf Restaurant Kitchen Rack Wall Mounted Floating Shelving
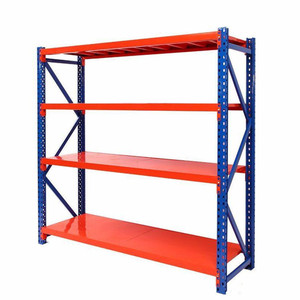
Custom Heavy-Duty Metal Rack Storage Shelf High Quality Iron Warehouse Racking Cargo Storage Equipment Customized Heavy-Duty
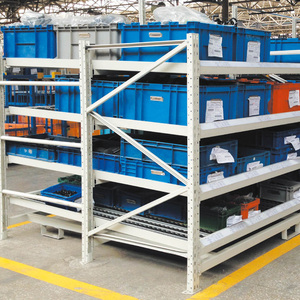
High Density Heavy Duty 5 Cold Rolled Steel Powder Coated Flow Rack Warehouse Storage Carton Pallet Gravity Shelves Customized
Direct-from-Manufacturer Scale & Engineering Governance
Operating continuously since 2001, Guangzhou Heda Shelves Co., Ltd. combines heavy metallurgical processing with rigorous FEA finite element analysis to engineer dependable industrial storage platforms worldwide.
Verifiable Compliance & Certifications
Auditable production lines operating strictly under CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Quality Management System No. 18624Q00169R0M, and comprehensive RoHS chemical inertness certifications.
Structural FEA & Free 24h CAD Layout
Complete parametric warehouse layouts designed by 300+ in-house technical personnel within 24 hours. Includes precise seismic load reviews, slab base pressure distributions, and 3D realistic rendering.
Container Cube Landed-Cost Optimization
Bespoke nested beam profiling, knock-down upright frames, and rigid bundle strapping engineered to maximize high-cube (40HQ) ocean container utilization up to 98%, substantially minimizing freight cost per pallet position.
Marine & Tropical Surface Pretreatment
10-stage automated surface conversion comprising acid pickling, zinc phosphating, and automatic electrostatic polyester powder baking (60–80μm), resisting salt spray corrosion in coastal hubs and extreme monsoons.
Engineering Structural Analysis: Pallet Racking Design Fundamentals
Industrial pallet racking is not merely static steel shelving; it is an unbraced or semi-rigid framed steel structure subjected to severe static gravitational forces, dynamic seismic ground acceleration, and operational lift-truck impact loads. Sourcing from top-tier Chinese erecting pallet racking manufacturers requires understanding the underlying mechanical criteria governing cold-formed steel sections under Eurocode EN 15512, FEM 10.2.02, and American RMI (MH16.1) codes.
The core structural integrity of an erected pallet rack hinges upon the upright frame buckling capacity and the connector beam-end moment-rotation stiffness. Upright profiles must feature roll-formed multi-rib geometry—such as an 11-fold to 13-fold cross-section—to prevent local torsional-flexural buckling under axial compression. Upright column steel thickness typically ranges between 1.5mm and 2.5mm, roll-formed continuously from structural carbon steel coils with guaranteed minimum yield strengths (Q235B with fy ≥ 235 N/mm² or high-strength Q355B with fy ≥ 355 N/mm²).
Under international standards (EN 15512 / FEM 10.2.02), beam deflection under safe working load (SWL) must never exceed L/200 (one two-hundredth of the clear beam span). Furthermore, structural frames must maintain a global safety factor of at least 1.4 to 1.5 against material yield under combined factored Dead Load (DL) + Live Pallet Load (LL) + Dynamic Forklift Impact Load (IL).
Cold-Formed Beam-to-Column Interlocking Mechanics
The beam-to-column connection dictates total system sway stability. HEDA engineering uses 3-claw to 5-claw high-tensile connection brackets welded to dual-C interlocking step beams or closed box profiles. When loaded, the downward vector of the pallet wedges the bracket tighter into the tapered upright teardrop or diamond perforations. Secondary mechanical spring locking pins (tested to withstand upward shearing forces of ≥ 5.0 kN) prevent unintentional accidental dislodgement caused by forklift mast errors.
| Racking System Classification | Structural Profile Config | Typical Clear Bay Span | Maximum Load Per Tier | Volumetric Space Density | Forklift Compatibility |
|---|---|---|---|---|---|
| Selective Pallet Racking | 90/100/120mm Omega Upright + Box Beam | 2,300mm – 3,900mm | 1,000 kg – 4,500 kg | Moderate (40–45%) | Counterbalance, Reach Truck |
| Double Deep Storage System | 100/120mm Reinforced Frame + Step Beam | 2,300mm – 3,300mm | 1,500 kg – 3,200 kg | High (60–65%) | Pantograph Deep Reach Truck |
| Automated Radio Shuttle Racking | Continuous Guide Rails + Heavy Upright | Up to 40m Lane Depth | 1,500 kg per Pallet | Maximum (75–85%) | Standard Forklift + Radio Carrier |
| Drive-In / Drive-Through System | Cantilever Arm Brackets + Saddle Beams | Continuous Pallet Rail | 1,000 kg – 1,500 kg | Very High (70–75%) | Narrow Counterbalance / Reach |
| Rack-Supported Mezzanine Floor | Integrated Heavy Uprights + C/Z Joists | Grid Spans 3,000–6,000mm | 300 – 1,200 kg/m² Floor | Multi-Floor (200%) | Pallet Jack, VNA, Goods Lift |
Future Procurement Trends in Industrial Warehouse Racking (2026–2035)
As global supply chains navigate supply diversification, port decongestion, and near-shoring expansions, procurement executives are re-evaluating their capital expenditure (CapEx) strategies for heavy warehouse racking.
Standardized Modular Interchangeability
Enterprise 3PL operators are discontinuing proprietary, vendor-locked profiles in favor of open standard 75mm (European/FEM) and 76.2mm (American standard teardrop) connector configurations. This allows regional distribution centers to expand, reconfigure, or swap beams across multiple distribution nodes without requiring complete structural replacement.
Landed CIF/DDP Tonnage Procurement
Procurement teams are shifting evaluations from ex-factory piece prices to Total Landed Cost (TLC) metrics. Due to escalating maritime container freight, sourcing decisions heavily prioritize suppliers capable of optimal bundling, computerized container load simulation (Cube Packing >95%), and high-yield steel profiles that decrease overall structural weight without sacrificing load rating.
Seismic Certification & Mill Traceability
Global insurance underwriters and municipal regulators now mandate stringent structural documentation. Buyers are obligating tier-1 Chinese exporters to supply full batch Mill Test Certificates (EN 10204 Type 3.1), demonstrating precise chemical composition, elongation percentages, Charpy V-notch impact toughness, and third-party verified seismic design calculations tailored to regional peak ground acceleration (PGA).
Technological Evolutions in Pallet Racking Fabrication
Modern manufacturing of warehouse racking has transformed from manual welding workshops into automated, high-precision industrial robotics ecosystems.
The convergence of automated materials handling, high-bay vertical architectures, and climate-controlled cold distribution chains has accelerated three foundational evolutionary shifts in racking manufacture:
Automation-Ready Tolerances (ASRS & AMR Integration)
With the rapid proliferation of Autonomous Mobile Robots (AMRs) and Automated Storage and Retrieval Systems (AS/RS), racking manufacturing tolerances have tightened from traditional ±3.0mm structural variations down to sub-millimeter precision (±0.8mm). CNC continuous roll-forming lines integrated with flying optical laser punching ensure flawless pitch consistency over 16-meter continuous single-piece upright sections.
Resilient Hot-Dip Galvanizing & Duplex Pretreatment
For sub-zero cold chain facilities (-25°C to -35°C) and coastal marine environments where standard powder coatings risk micro-cracking and under-film rust creep, advanced duplex systems are replacing single treatments. Hot-dip galvanization conforming to ISO 1461 combined with low-bake epoxy-polyester electrostatic primers ensures decades of maintenance-free service life without steel embrittlement.
Smart Structural Health Monitoring (SHM)
Emerging super-tall clad warehouses are seeing the pilot installation of IoT-enabled fiber-optic strain gauges and triaxial acceleration impact sensors embedded directly within the lower upright frame anchors. These sensors provide real-time telemetry on static payload shifts, unauthorized forklift impact shocks, and seismic foundation settlement before catastrophic structural failure occurs.
HEDA Shelves 10-Stage Industrial Production Methodology
Every structural element exported from our 30,000 m² Guangzhou facility undergoes a closed-loop quality control regimen, guaranteeing structural reliability from coil inspection to port staging.
Raw Materials
Certified steel coil inspection, yield & tensile verification (MTC 3.1).
Precision Cutting
Automated uncoiling, leveling, and high-tolerance hydraulic shearing.
Column Punching
CNC progressive multi-station punching for precise pitch alignment.
Cold Bending
Multi-pass cold rolling creates complex stiffening rib geometry.
Profile Forming
Seamless interlocking box beam and upright profile formation.
Surface Polishing
Automated deburring, weld smoothing, and sharp-edge chamfering.
Robotic Welding
Multi-axis robotic GMAW welding of beam end connectors & base plates.
Pickling & Phosphating
Chemical surface conversion removing scale and optimizing coating adhesion.
Powder Coating
Electrostatic polymer application baked at 200°C for durable finish.
QC & Ocean Bundling
Caliper dimensional audits, film wrapping, and steel strap packaging.
Frequently Asked Questions (FAQ) for International Procurement
Direct, highly specific engineering and commercial answers to help procurement officers, civil engineers, and supply chain directors execute successful import projects.
Q What primary structural parameters are required to generate an accurate rack layout and static calculation?
To produce an authoritative structural layout and quotation, we require: (1) Architectural CAD floor plan showing building column centers, door openings, clear height under roof joists, and fire sprinkler clearances; (2) Detailed pallet profile including width (W), depth (D), overall load height (H including pallet), and maximum gross weight; (3) Forklift fleet technical data sheet (clear mast lift height, minimum turning radius, right-angle stacking aisle width requirement); (4) Concrete slab specification (thickness, compressive strength fc', reinforcement mesh details); (5) Project geographical site location to determine seismic zone coefficient and wind uplift loads for outdoor or clad installations.
Q How does HEDA Shelves assure anti-corrosion resilience in humid tropical or cold-storage environments?
Corrosion resistance is achieved through our multi-phase automated surface pretreatment line. Raw steel is not simply degreased; it proceeds through acidic immersion pickling to eradicate all mill scale and surface oxidation, followed by high-density zinc phosphating. This chemically alters the microscopic steel substrate to guarantee exceptional mechanical adhesion of the electrostatically deposited thermosetting polyester powder coating (cured at 180°C–200°C, 60–80 microns dry film thickness). For extreme conditions—such as cold chain stores down to -30°C or marine coastal warehouses—we supply continuous hot-dip galvanized components (ISO 1461, ≥ 55–85μm zinc thickness).
Q What certifications can be provided to support local building permit approval and safety insurance audits?
Guangzhou Heda Shelves Co., Ltd. provides comprehensive compliance dossiers containing: European CE Certification No. 2435-CPR-8605159 (Construction Products Regulation for structural metallic works), ISO 9001:2015 Quality Management System Certification (Registry No. 18624Q00169R0M, verified valid), and third-party laboratory material test reports demonstrating RoHS chemical compliance. Furthermore, our engineering division issues stamped structural calculation packets verifying compliance with FEM 10.2.02, EN 15512, and RMI MH16.1 design philosophies upon contract award.
Q How do you solve overseas installation challenges and prevent on-site assembly errors?
Every export order is packaged using a computerized logistics numbering schema. Uprights, bracing chords, beam levels, and row spacers are tagged with physical color-coded metal/vinyl labels referencing a comprehensive master installation drawing booklet (3D isometric exploded diagrams, 2D elevation markers, and detailed torque-tightening specifications for anchor bolts). We supply step-by-step video installation workflows and provide remote video conferencing engineering support. For multi-million-dollar distribution centers, HEDA senior commissioning engineers can be deployed on-site to supervise and certify local installation crews.
Q Which discharge ports and transit corridors do you routinely service for global clients?
We routinely export full container loads (FCL—20GP, 40GP, 40HQ) from our domestic staging ports in Guangzhou, Shenzhen, and Nansha to all primary maritime transport hubs globally. This encompasses major South Asian gateways (Nhava Sheva/JNPT, Mundra, Chennai, Kolkata, Chattogram, Karachi, Colombo), Southeast Asian destinations (Ho Chi Minh, Haiphong, Bangkok, Port Klang, Manila), Middle Eastern logistics centers (Jebel Ali, Dammam, Jeddah), as well as key European and American deepwater container ports. For landlocked destinations (such as Nepal, Bhutan, or Central Asian states), we arrange seamless multi-modal sea-rail or sea-truck bonded transshipment routes.
Q What is the mechanical difference between Q235B and Q355B steel in racking structural members?
Q235B possesses a nominal yield strength of 235 MPa and ultimate tensile strength of 370–500 MPa, with high ductile elongation (≥ 26%), making it an ideal, cost-effective structural choice for low-to-medium height pallet racks and standard distribution storage. Q355B (formerly Q345) delivers an elevated yield threshold of 355 MPa and tensile strength of 470–630 MPa. Sourcing Q355B allows us to roll-form thinner wall sections while sustaining identical or superior column buckling resistance, significantly reducing total dead load on warehouse floor slabs and providing superior structural safety margins for tall uprights (≥ 10m) in high-seismic zones.
Accelerate Your Warehouse Capacity with Verified Engineering Precision
Send our senior engineering team your warehouse architectural plans today. We will supply a complete AutoCAD layout, 3D structural visual rendering, and an itemized landed-cost export proposal within 24 hours.