Heavy Chemical Selective Racks
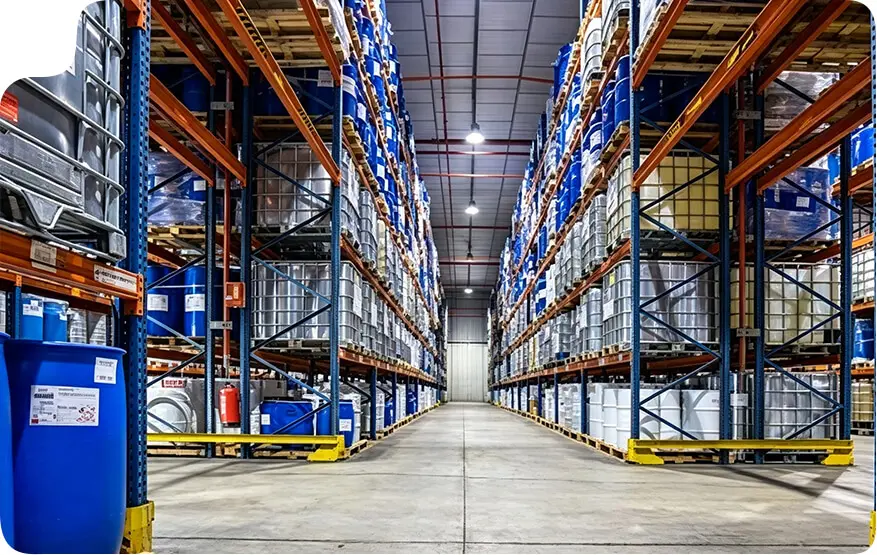
Designed for fast-moving multi-SKU chemical warehouses. Features reinforced upright profiles, drop-in chemical spill sumps, and 100% direct access to every chemical pallet position.
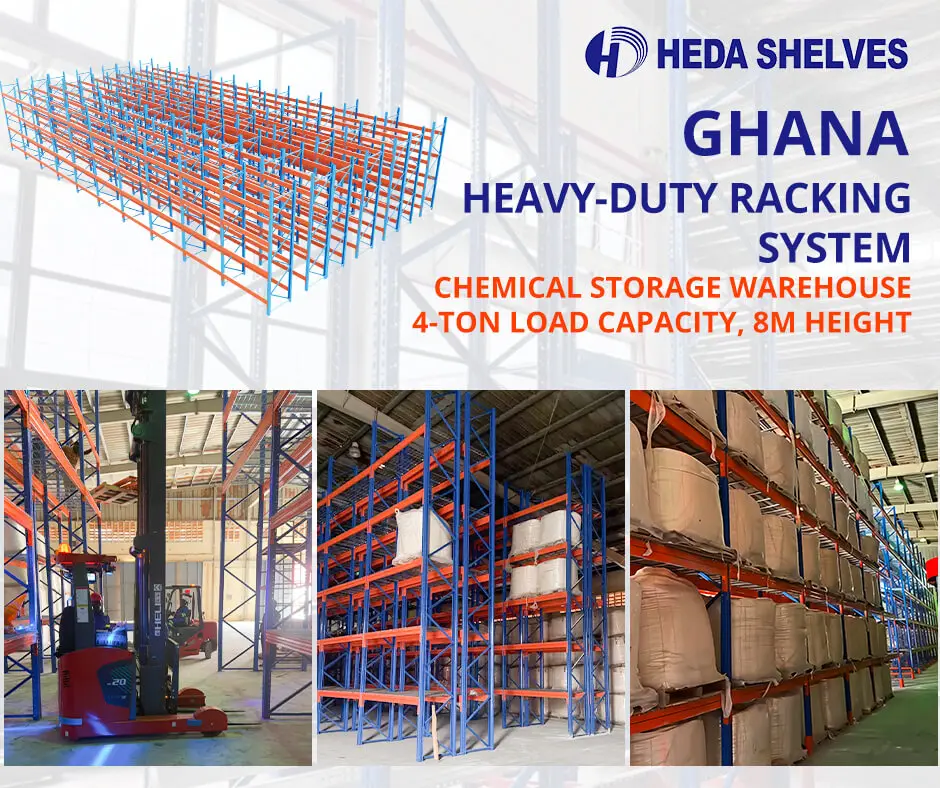
Chemical warehousing demands superior structural integrity, zero-leak tolerance, and environmental protection. Guangzhou Heda Shelves Co., Ltd. configures specialized rack systems tested against harsh chemical vapors, concentrated heavy point-loads, and strict containment regulations.
Designed for fast-moving multi-SKU chemical warehouses. Features reinforced upright profiles, drop-in chemical spill sumps, and 100% direct access to every chemical pallet position.
Purpose-built for concentrated liquid weights. Integrated curved drum cradles prevent rolling during active dispensing, while heavy-capacity beams safely carry 1,000L intermediate bulk containers (IBCs).
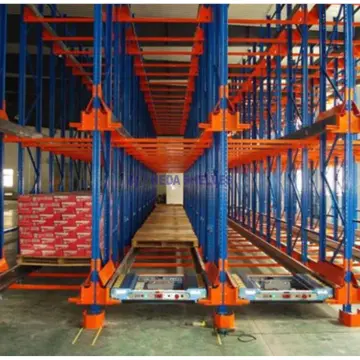
Eliminates forklift traffic inside hazardous material storage channels. Semi-automated shuttles move volatile solvents and explosive raw materials smoothly, cutting risk of impact fire hazards.
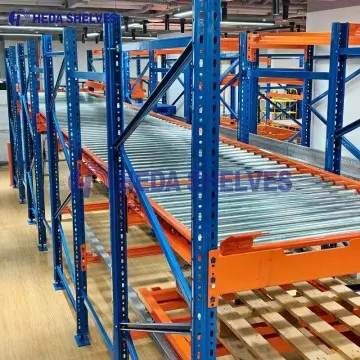
Gravity-driven roller beds engineered with acid-resistant roller bearings. Guarantees strict First-In, First-Out (FIFO) stock turnover for short shelf-life chemical catalysts, resins, and medical reagents.
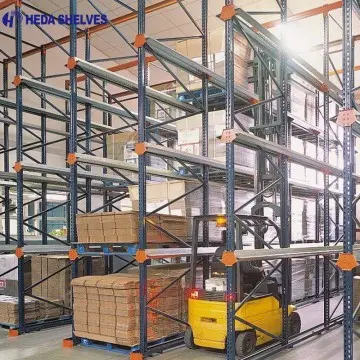
Maximizes spatial utilization for single-SKU bulk chemical storage such as polymers, plastic resins, and dry agricultural fertilizers. Continuous rail design eliminates wasteful picking aisles.
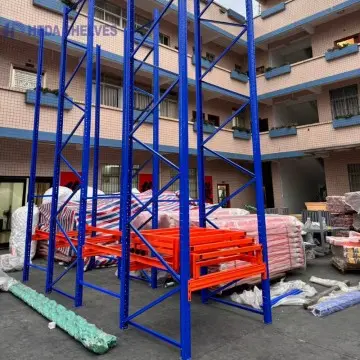
Combines high-density storage with dedicated lane selectivity. Heavy nested steel carts slide along inclined structural steel channels, safely holding 2 to 5 pallets deep per lane with minimal handling.
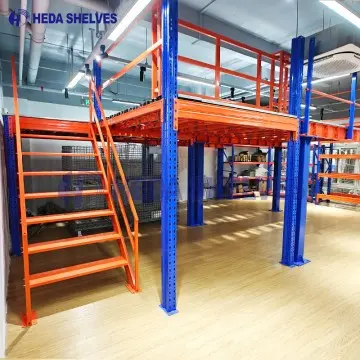
Heavy structural steel platforms (300 to 1,000+ kg/m²) custom manufactured for upper-level chemical sampling stations, cleanroom testing rooms, blending vats, and packaged lubricant staging.

Unobstructed arm storage for pressurized gas cylinders, chemical PVC/steel pipelines, chemical hoses, and bar stocks. Load capacities up to 3,000 kg per arm level with retention end-stops.
The global chemical logistics sector is facing tighter international environmental governance, stricter hazardous materials handling standards, and rapid automation adoption. Understanding these key trends ensures long-term return on capital expenditure and complete statutory compliance.
Global environmental regulatory bodies (such as EPA 40 CFR 264.175 and European DG directives) increasingly enforce secondary spill containment sumps capable of holding at least 110% of the largest vessel stored or 25% of the total liquid volume. Modern chemical racking must integrate built-in leak detection sumps and removable galvanized grating directly below pallet decks.
Standard paint finishes fail rapidly when exposed to acidic vapors, chlorine vapors, and high coastal humidity. Procurement officers are specifying multi-stage chemical pretreatment—including multi-tank acid pickling, zinc phosphating, and thermosetting epoxy-polyester powder coats—or full ISO 1461 hot-dip galvanizing for coastal chemical storage parks.
Under NFPA 30 (Flammable and Combustible Liquids Code), rack-mounted in-rack sprinkler systems (ESFR) with quick-response heads are critical. Modern chemical racking systems are engineered with dedicated internal flue spaces, perimeter upright brackets, and slotted transverse bracing to house deluge sprinkler piping safely away from forklift impacts.
To comply with stringent occupational safety mandates and avoid exposing warehouse operators to toxic fumes or explosive zones, enterprises are shifting toward AS/RS stacker cranes and radio shuttle carrier systems. Automated chemical storage increases inventory speed, prevents mast collisions with IBC tanks, and integrates with chemical tracking software.
| Chemical Storage Class | Recommended Racking System | Spill Protection & Containment | Anti-Corrosion Surface Spec | Fire & Electrical Safety Protocol |
|---|---|---|---|---|
| Flammable Solvents (Class 1A, 1B) | Selective Rack / Radio Shuttle | Galvanized catch basin sumps (110% single drum capacity) | Anti-static electrostatic powder coat (RAL custom) | In-rack ESFR deluge sprinklers + copper grounding studs |
| Corrosive Acids & Alkalis (Class 8) | Heavy Duty Selective or Drive-In | Chemical-grade epoxy resin sumps or poly-lined trays | Multi-tank pickling + high-build epoxy or hot-dip galvanizing | Corrosion-proof fiberglass grating and acid-resistant seals |
| Intermediate Bulk Containers (1000L IBC) | Reinforced IBC Heavy Duty Pallet Rack | Integrated floor collection drains + heavy containment bays | Electrostatic thermoset powder coat with 120μm minimum dry film | Continuous horizontal flue spaces for overhead foam injection |
| Agrochemicals & Fertilizers | Selective Rack with Steel Wire Mesh Decks | Modular containment pallets with drain plugs | Anti-corrosion powder coating resistant to nitrates & ammonia | Explosion-proof warehouse lighting layout compatibility |
| Pressurized Gas Cylinders | Heavy Cantilever Racks with Safety Arms | Mechanical fall-restraint chains and cradle chocks | Durable hot-dip galvanized coating for open shed ventilation | Classified zoning separation according to NFPA 55 |
* Note: Guangzhou Heda Shelves Co., Ltd. provides comprehensive structural load calculations, finite element analysis (FEA), and seismic baseline verification tailored to your specific chemical facility site drawings.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established itself as an authoritative global manufacturer of high-precision warehouse racking systems and hazardous material chemical storage racking configurations. Spanning a 30,000 square meter standardized production facility in Guangzhou, China, our manufacturing line integrates robotic welding stations, automatic cold-bending roll-forming lines, automated multi-head column punching systems, and comprehensive surface treatment facilities.
Chemical warehouse operators cannot gamble with structural fatigue or poor coating adhesion. With our experienced team of 300+ engineers, technicians, and international project directors, we execute complete in-house quality control across every production stage—from raw steel coil ultrasonic inspection to finished powder coating thickness testing.
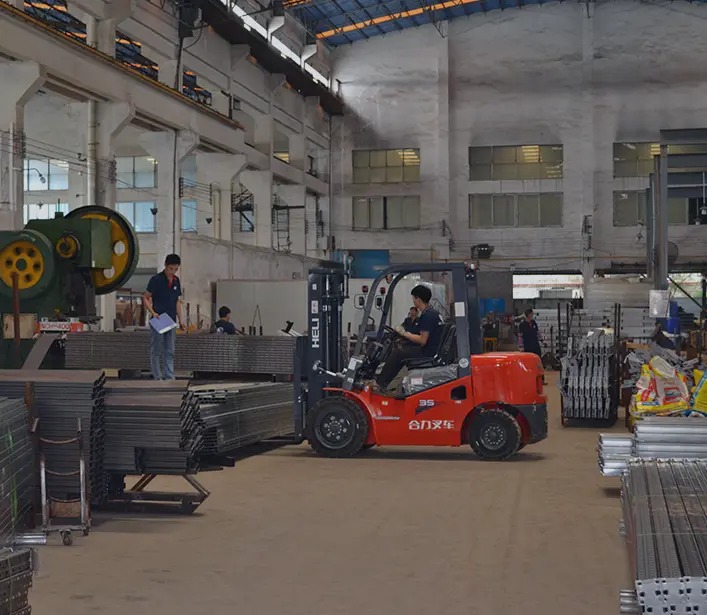 Inside Guangzhou Heda Shelves 30,000 m² Manufacturing Facility
Every upright frame, box beam, and containment component undergoes rigid manufacturing quality assurance to ensure flawless performance under corrosive chemical exposures.
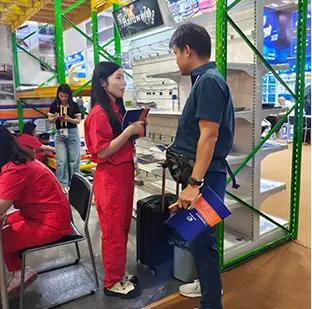
We review your chemical safety sheets, liquid viscosities, container weights, and floor slab specifications.
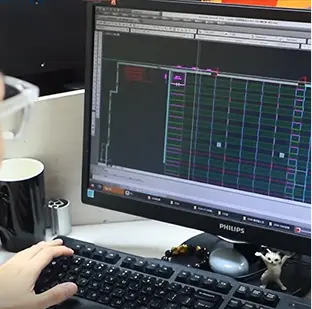
Our engineers formulate free CAD designs, 3D renderings, and secondary containment capacity calculations.
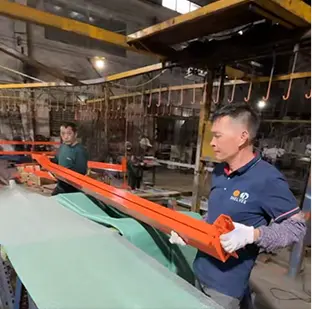
Roll forming, CNC automated punching, certified robotic welding, and pickling-phosphating surface preparation.
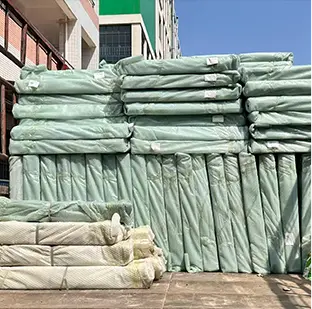
Protective bundling, moisture-barrier wraps, container load optimization, and comprehensive installation manuals.
 STEP 01
Certified Q235B & Q355B structural steel.
 STEP 02
Automated cutting to exact engineering tolerances.
 STEP 03
High-precision pitch control for beam connectors.
 STEP 04
Continuous multi-pass rollers for section stiffness.
 STEP 05
Interlocking heavy-duty welded box beams.
 STEP 06
Ensuring zero sharp edges for chemical pouch safety.
 STEP 07
Full-penetration CO2 shielded structural welding.
 STEP 08
Deep-cleaning rust scale & chemical etching.
 STEP 09
Electrostatic baking at 200°C for chemical shield.
 STEP 10
Load deflection testing and container-ready packs.
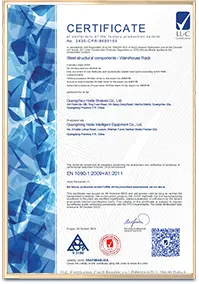
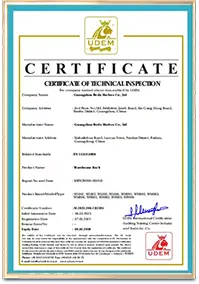
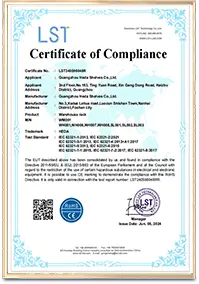
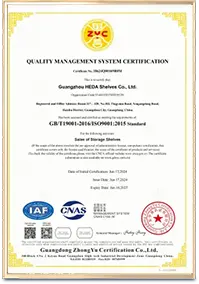
When procuring industrial chemical storage racking systems, chemical safety audits by government environmental inspectors require documented certification. Guangzhou Heda Shelves Co., Ltd. provides verifiable quality and structural credentials ready for facility validation.


Trusted by Global Chemical, Manufacturing & Logistics Enterprises

Key technical answers to the most frequent inquiries raised by dangerous goods logistics directors, EHS managers, and procurement executives.
Standard warehouse racking is engineered strictly for dry static loads. A chemical storage racking system incorporates heavy-duty structural steel profiles, certified anti-corrosion surface treatments (such as specialized chemical-resistant electrostatic powder coatings or hot-dip galvanizing), secondary spill containment sumps, drum cradles, integrated grounding studs for static discharge, and compliance with NFPA 30 and OSHA hazardous storage regulations.
Our factory implements a comprehensive multi-stage industrial finishing process: raw steel components undergo automatic multi-tank acid pickling and phosphating pre-treatments to remove scale and ensure chemical bonding, followed by heavy-build thermoset epoxy-polyester powder coating cured at 200°C. For aggressive acid, chlorine, or offshore environments, we supply hot-dip galvanized components conforming to ISO 1461.
Yes. Our engineering department designs modular chemical storage racking configurations equipped with heavy-duty box beams rated up to 4,000 kg per pair, reinforced steel decking, custom saddle cradles for horizontal barrel dispensing, and heavy-gauge galvanized drop-in sumps sized specifically for standard industrial pallets, 200L drums, and bulk IBC containers.
Our systems are engineered to facilitate compliance with global environmental and safety standards including OSHA 1910.106, EPA 40 CFR 264.175 for secondary containment, NFPA 30 flammable liquid storage criteria, and European CE structural safety norms (EN 15512 / EN 15620). We ensure adequate internal flue spacing for in-rack deluge sprinkler pipe runs.
Every chemical storage racking project delivered by Guangzhou Heda Shelves Co., Ltd. includes verified Mill Test Certificates (MTC) for steel grades (Q235B/Q355B), finite element structural calculation reports, third-party verified CE certificate No. 2435-CPR-8605159, ISO 9001:2015 certificate, component-coded installation CAD drawings, and load capacity plaques for rack bays.
Automated radio shuttle racking removes manual forklift traffic from deep storage bays, dramatically reducing the risk of accidental mast collisions with chemical containers. It optimizes climate-controlled or volatile storage areas, enhances safety separation between hazardous classes, and provides precise automated inventory tracking via integrated warehouse management systems.
Provide your warehouse dimensions, chemical classifications, and container types. Our dedicated engineering office will prepare a comprehensive CAD layout, 3D rendering, and commercial proposal within 24 hours.