Top Trusted Warehouse Pallet Storage Factory & Exporters
Global cold-rolled structural steel storage engineering, high-density automated systems, and high-cube sea freight logistics serving 120+ countries since 2001.
Engineered Product Portfolio
Industrial Warehouse Pallet Storage Systems
Heavy-duty structural configurations manufactured with premium Q235B/Q355B coil steel, precision roll-formed upright profiles, and micro-metric adjustment slots for maximum volume utilization.
Heavy-Duty
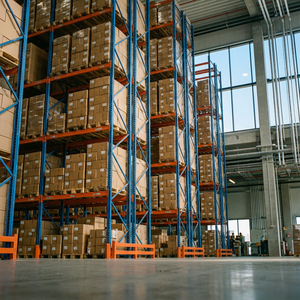
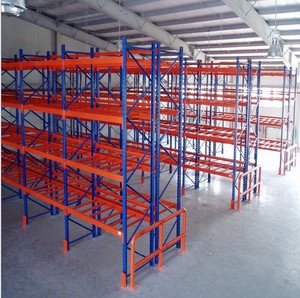
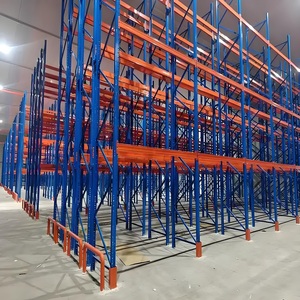
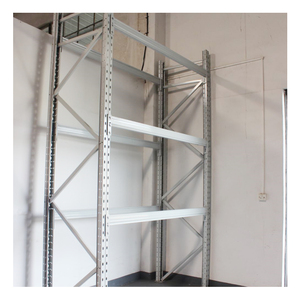
Customized Heavy Duty Pallet Racking System Warehouse Storage Rack Factory Direct
Full 100% selective accessibility with multi-stage interlocking beams and 1,000–5,000 kg capacity per level.
Engineering Integrity & Structural Dynamics in Heavy-Duty Pallet Racking
In the modern international logistics ecosystem, pallet racking is not merely static steel shelving; it is an engineered load-bearing structural framework operating under extreme, dynamic stress cycles. Specifying storage systems for distribution centers across North America, Europe, the Middle East, and South Asia requires acute consideration of structural elasticity, seismic vulnerability coefficients, metallurgical grain consistency, and soil-slab dynamic deflection.
At Guangzhou Heda Shelves Co., Ltd., every pallet storage rack system is fabricated from prime, continuous-cast Q235B and high-yield Q355B cold-rolled structural steel coils. The precision continuous roll-forming sequence cold-works the steel sections into specialized 11-fold and 13-fold omega upright profiles. This proprietary cross-sectional geometry significantly shifts the shear center and amplifies the torsional-flexural buckling threshold beyond standard EN 15512, FEM 10.2.02, and ANSI MH16.1 specifications.
Vertical frame components utilize computerized multi-stage CNC automatic stamping lines to execute high-tolerance hook-in slot arrays (available in 50mm, 75mm, and 76.2mm metric/imperial pitches). Beams are constructed with welded dual-C interlocking closed box profiles or stepped beam sections fitted with 3, 4, or 5-claw high-strength cast-steel connector plates. The integration of high-visibility zinc-coated locking pins guarantees that horizontal beams resist dynamic vertical dislodgement up to 1,000 daN shear force caused by inaccurate forklift tines or sudden upward lifting shocks.
In-House Manufacturing Depth
Complete end-to-end operational control in our 30,000 m² Guangzhou facility: laser slitting, cold rolling, robotic welding, 9-stage ultrasonic phosphating, and automatic dual-booth electrostatic powder coating.
Verifiable Regulatory Credentials
Compliance audited by internationally recognized bodies: CE Certification No. 2435-CPR-8605159, ISO 9001:2015 Management System No. 18624Q00169R0M, and full RoHS eco-compatibility.
Global Intermodal Export Flow
Turnkey ocean freight handling to primary corridors: Nhava Sheva, Mundra, Chattogram, Colombo, Karachi, Rotterdam, Houston, and Jebel Ali with container nest-loading algorithms maximizing TEU fill rates.
Strategic insights for enterprise supply chain leaders, logistics directors, and third-party logistics (3PL) infrastructure investors.
The Shift Toward Total Cost of Architecture (TCOA)
Global procurement metrics are migrating rapidly from initial FOB steel purchase prices to full lifecycle resilience. High bay warehouses, robotic material handling integrations, and rising real estate lease rates per square meter make rack deflection, seismic compliance, and surface longevity decisive factors.
Circular Steel Life-Cycle Auditing: Demands for low embodied carbon steel and non-toxic thermoset powder polymers compliant with LEED v4.1 green warehouse standards.
Pre-Engineered AMR/AGV Interfacing: Racking footprints are designed upfront with ground base plate clearances for floor-running Autonomous Mobile Robots and automated reach forklifts.
Localized Import Duty & Freight Optimization: Modular bundled knock-down frames that ensure 40HQ maritime containers hit minimum deadweight limits of 26-28 metric tons without volumetric air voids.
Engineering Benchmark Metrics
Empirical stress data collected across 10,000+ deployments demonstrates the performance divergence between generic structural racks and HEDA engineered cold-formed profile geometries:
The convergence of omnichannel supply chains, automated fulfillment, and cold chain perishables logistics has catalyzed three fundamental technological transitions across industrial storage production:
1. Semi-Automated Shuttle Kinematics
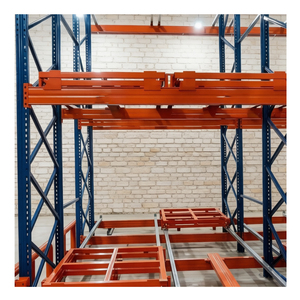
Transitioning from conventional drive-in systems to four-way radio pallet shuttles running on specialized cold-formed galvanized rails. Eliminates forklift rack incursions, reducing mast damage by 92% and boosting lane picking speed by 300%.
2. IoT Real-Time Deflection Telemetry
Next-generation rack bays integrate smart sensor brackets that monitor vertical beam micro-strains, impact vibrations, and post-seismic plumb-line shifts. Real-time telemetry notifies warehouse management systems (WMS) of overload conditions instantly.
3. Climate & Anti-Corrosion Metallurgy
Advanced pre-treatment chemistry combining iron/zinc phosphating with high-build hybrid epoxy-polyester coatings (60–90 microns). Designed to combat aggressive coastal condensation, monsoon humidity, and food facility clean-in-place washdowns.
Medium-turnover goods, buffer storage staging before dock shipping.
Rack-Supported Mezzanine
Manual / Pallet Hybrid
150% – 250% (Multi-level)
Flexible (Conveyors / Lift)
E-commerce order fulfillment, garment picking, automotive components.
Procurement Intelligence
Frequently Asked Questions for Project Specifiers
Direct technical clarity on compliance, installation engineering, slab calculations, and ocean freight logistics.
How does HEDA guarantee steel grade and structural yield strength consistency?
We source raw carbon steel exclusively from tier-one state-owned mills accompanied by verified 3.1 Mill Test Certificates (MTC). Every production batch undergoes destructive tensile tests (confirming yield strengths ≥235 MPa for Q235B and ≥355 MPa for Q355B) and chemical composition spectrophotometry before continuous roll-forming begins.
What structural data is necessary to generate a free customized CAD/3D proposal?
To deliver an engineered proposal within 24 hours, our structural engineering team requires: (1) Warehouse building DWG or dimensional PDF layout identifying column grids and overhead clearance obstructions; (2) Concrete slab thickness and rebar specifications; (3) Pallet dimensions (W x D x H) including cargo overhang and gross weight; (4) Specific forklift models, mast lift heights, and turning radii.
Can the racking profiles adapt to seismic zones and low-temperature cold storage?
Yes. We calibrate upright gauge thicknesses, cross-bracing angles, baseplate footprint dimensions, and anchor bolt embedment depths to match local seismic acceleration factors (PGA). For cold stores operating at temperatures down to -25°C, we specify low-temperature impact-resistant steel and specialized hot-dip galvanized or cryogenic epoxy coatings to eliminate brittle fracture risks.
How do you maximize ocean container utilization and prevent in-transit corrosion?
All components undergo automated steel strip strapping, protective corrugated card corner guards, and heat-shrink polyethylene wrapping. Heavy upright frames and horizontal beams are bundled via 3D container packing simulations, achieving maximum weight ratings in 40ft High Cube containers. High-grade desiccant packs are inserted to neutralize ocean-freight condensation.
What is the typical production lead time for a 500–2,000 ton project?
Standard fabrication cycle times range between 15 to 25 business days from final CAD drawing sign-off. With 30,000 m² of factory space and an average monthly rolling throughput of 30,000 tons, our multi-line automated roll-forming and robotic welding cells can absorb large-scale commercial tenders without causing bottleneck delays.
Do you provide professional on-site installation guidance and commissioning?
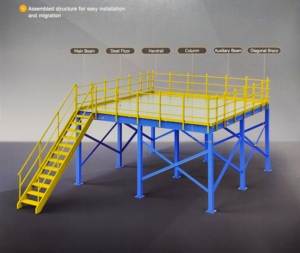
Yes. Every containerized consignment is dispatched with detailed 3D exploded assembly diagrams, piece-marked component labels, and video installation guides. For complex warehouse automation, high-bay VNA installations, and structural steel mezzanines, HEDA senior structural site engineers are dispatched internationally for hands-on contractor supervision.
What safety factors and deflection allowances are built into the load tables?
Our rack systems are engineered with a minimum structural safety coefficient of 1.5 to 1.65 based on cold-formed design standards. Under maximum rated uniformly distributed load (UDL), horizontal beam deflection is strictly restrained within the L/200 limit (where L is the clear beam span), preventing excessive permanent set and ensuring clear pallet fork entry.
How does HEDA handle private label OEM/ODM configurations for local racking brands?
We operate active private-label manufacturing agreements for racking distributors across Europe, North America, and Australia. We offer custom punching dies (matching teardrop, keyhole, or diamond hole patterns), personalized roll-formed stamping marks, specialized corporate RAL powder coating colors, and neutral or distributor-branded packaging.
Request an Engineered Warehouse Storage Layout & Factory Quote
Connect directly with our senior application engineering division. Receive a comprehensive CAD floor plan, volumetric pallet position audit, and competitive factory-direct CIF quotation within 24 hours.