Featured Industrial Gravity & Pallet Flow Racks
Engineered for seamless First-In, First-Out (FIFO) material progression. Browse our high-performance live storage racks manufactured to exacting European and global warehouse tolerances.
 500kg / Layer
500kg Steel Storage Racks 5-Layer Adjustable Pallet Racking System
 Live Dynamic
Heavy Duty Adjustable 5-Layer Carton Gravity Flow Rack CE Certified
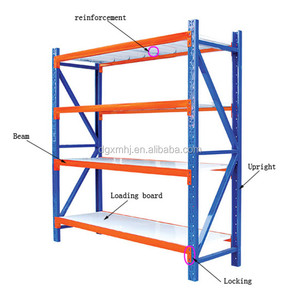 Modular Decking
Storage Warehouse Metal Medium Duty Weight Stacking Racks & Shelves
 Heavy Gravity
5 Layer Metal Pallet Flow Rack Gravity Industrial Storage Equipment
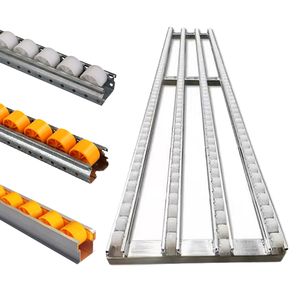 Sliding Roller
Carton Flow Rack System Sliding Roller Shelf for Distribution Lines
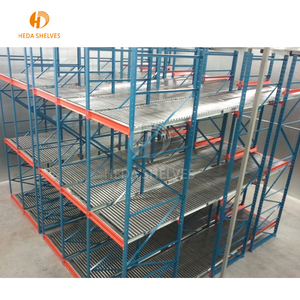 Order Picking
FIFO Order Picking Warehouse Shelf Gravity Carton Flow Rack System
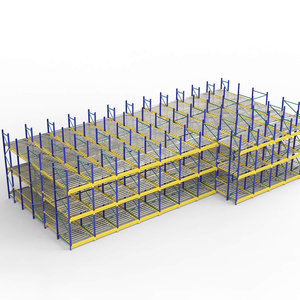 Customizable
 Heavy Duty Metal Gravity Flow Racking Storage Structure
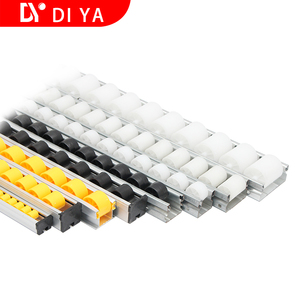 Roller Tracks
Gravity Flow Rail Roller Track Plastic Wheel 100KG Sliding Shelf
Future Warehouse Procurement Trends in Gravity Flow Storage (2025–2030)
As global fulfillment footprints contract toward urban centers and land lease values escalate exponentially, logistics operators and supply chain architects are transitioning away from static single-selective shelving toward dynamic high-density gravity flow racks. The modern procurement lifecycle no longer assesses racking simply as static steel tonnage, but rather as an unpowered mechanical automation system designed to minimize internal operational friction, labor travel distance, and floor space waste.
1. Omnichannel Micro-Fulfillment
The acceleration of same-day distribution requires carton flow beds directly integrated beneath pallet bulk replenishment levels. Micro-fulfillment centers require 100% accessible picking faces with high SKU density, reducing picker travel path by up to 65% compared to static wide-aisle configurations.
2. Hybrid AMR & AGV Interfacing
Modern flow rack purchasing specifications now demand precise tolerances for autonomous guided vehicle (AGV) and autonomous mobile robot (AMR) interfacing. Rear dynamic loading bays receive automated stock, while front gravity beds dispense single totes onto automated sorting conveyors.
3. Lifecycle TCO Over Initial CapEx
Enterprise procurement departments are prioritizing total cost of ownership (TCO) calculations. Investing in hardened polycarbonate roller wheels, magnetic friction brake rollers, and corrosion-resistant powder coatings avoids line stoppages, pallet hang-ups, and premature roller rail fatigue.
Modern enterprise buyers are also re-evaluating risk allocation. The procurement of flow racking systems demands verified mechanical resilience against structural deflection. When multiple pallets—each weighing between 1,000 kg and 1,500 kg—are accumulated along a 30-meter continuous slope, backpressure buildup against the lead discharge pallet can exceed 4,000 kg. Forward-thinking procurement directors therefore audit manufacturers strictly for integrated mechanical pallet separators and progressive brake controllers to guarantee total personnel safety and eliminate inventory crushing.
Structural Selection Matrix: Flow Racks vs. Alternative High-Density Systems
| Storage Architecture | Inventory Logic | Floor Space Efficiency | Picking Velocity | Energy / Power Needs | Primary Industrial Use Cases |
|---|---|---|---|---|---|
| Pallet Flow Racks | Strict FIFO (100%) | Extreme (Up to 80% footprint utilization) | Ultra High (Separated load & pick aisles) | Zero (Pure Gravity Driven) | FMCG, Cold Chain Logistics, Dairy, Pharmaceuticals |
| Carton Flow Beds | Strict FIFO (100%) | High (High vertical density) | Maximum (Split-second tote discharge) | Zero (Gravity Roller / Skate Wheel) | E-commerce Kitting, Electronics Assembly, Apparel |
| Drive-In Racking | Strict LIFO | High (Eliminates operating aisles) | Low (Forklifts enter structure slowly) | Zero (Static Frames) | Seasonal Bulk, Non-perishable raw manufacturing |
| Radio Shuttle System | Flexible FIFO / LIFO | Extreme (Deep lane up to 50m) | High (Automated shuttle transfer) | High (Battery-powered carts & charging) | Deep Freeze Rooms, Beverage Buffers, Central 3PLs |
| Push-Back Racks | Strict LIFO | Moderate to High (2 to 6 pallets deep) | Moderate (Single-aisle loading/picking) | Zero (Telescopic Nested Carts) | Medium turnover items, cold buffer dispatch stages |
Technological Innovations in Modern Live Storage Racking
The engineering integrity of dynamic gravity storage relies entirely on mechanical equilibrium between gravitational potential energy, kinetic motion acceleration, and controlled frictional braking. Without sophisticated metallurgy and roller dynamic engineering, flow racking risks catastrophic pallet acceleration or sudden lane jams.
Centrifugal & Magnetic Brake Rollers
To maintain safe pallet transit velocities below 0.3 meters per second regardless of load variance (from 300kg empty pallets to 1,500kg heavy cargo), state-of-the-art flow tracks utilize internal magnetic and centrifugal resistance braking rollers that throttle pallet kinetic velocity purely through mechanical induction without power cabling.
High-Tensile Cold-Formed Steels
By leveraging certified Q235B and high-yield cold-formed alloy profiles, upright uprights achieve optimal load-to-weight ratios. Precision hole punching allows millimeter-accurate pitch adjustments along the beam frames to alter decline slopes between 2.5% and 3.5% based on specific bottom-board friction factors.
Polymer Skate Tracks with Low Friction Deflection
Carton flow beds now utilize impact-resistant modified polypropylene and nylon dual-flanged wheels mounted on zinc-passivated cold-rolled sheet tracks. These deliver quiet decibel ratings below 55dB while sustaining zero wheel flat spots under prolonged ambient or sub-zero refrigeration conditions.
Solving Dynamic Load Hazards: The Mechanics of Pallet Separation
In long-run pallet flow lanes (ranging from 5 to 25 pallets deep), backpressure is the principal factor behind operator accidents and pallet damage. When a forklift attempts to lift the first pallet at the unload face, the continuous cumulative slope pressure from trailing pallets presses against it, causing severe mast binding or load collapse. Our factory engineers address this by incorporating automatic mechanical safety pallet separators.
These spring-loaded or cam-activated mechanical traps lock the second pallet in line precisely 300mm behind the lead pallet. Only when the lead pallet is lifted completely free does the latch reset, allowing the trailing queue to gently index forward one pallet position at a controlled speed. This isolated index sequence safeguards forklift masts, preserves bottom pallet boards from shearing, and maintains continuous, jam-free inventory flow across all shifts.
Why Global Enterprises Source from HEDA Shelves
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates as a vertically integrated warehouse storage equipment manufacturer. By maintaining full operational control over layout engineering, automated stamping, profile cold-roll forming, robotic welding, surface chemical pretreatment, and powder curing, we deliver verifiable reliability to distribution centers across more than 120 countries.
Our 10-Stage Precision Manufacturing Pipeline
Every gravity flow component manufactured in our facility undergoes rigorous verification against CE certification No. 2435-CPR-8605159 and ISO 9001:2015 quality assurance protocols:
Raw Materials
Certified steel coil testing for tensile strength, elongation, and carbon chemistry.
Precision Slitting
CNC slitting lines cut strip widths with +/-0.2mm tolerance to eliminate burrs.
Automated Punching
High-speed continuous presses punch teardrop and diamond upright hole patterns.
Cold Roll-Forming
Multi-stand roller dies progressively bend uprights into rigid multi-flanged columns.
Profile Forming
Box beam roll-forming and robotic seaming to provide superior deflection resistance.
Mechanical Finishing
Deburring and edge rounding ensure worker safety and prevent snagging during use.
Robotic Welding
Automated MIG welding fixtures fuse beam connectors with deep penetration fillets.
Chemical Pretreatment
Multi-stage degreasing, pickling, and phosphating bath lines create an anti-corrosion barrier.
Powder Coating
Automatic electrostatic powder booths apply tough polymer resins baked at 200°C.
QC & Ocean Bundling
Dynamic track test runs, load cell deflection checks, and container-optimized steel banding.
Thanks to our dedicated automated powder coating line and chemical pickling tanks, all racking members withstand high humidity, coastal sea air, and extreme cold storage cycling down to -30°C without flaking, peeling, or micro-cracking. For demanding ocean shipments and inland intermodal transits across South Asia, the Middle East, and the Americas, structural beams and upright trusses are strapped using automated protective padding to ensure zero on-site transit damage.
Warehouse Flow Racks: Engineering & Sourcing FAQ
Answers to common structural design, slope calculation, and loading safety questions asked by logistics planners and procurement executives.
What is the optimal slope gradient for gravity pallet flow lanes?
The industry standard gradient ranges between 2.5% and 3.5% (approximately 30mm to 35mm of vertical fall per linear meter). However, the precise pitch is determined by your pallet bottom board material (hardwood, softwood, plastic, or metal runner profiles), base deflection under full payload, and overall temperature. For cold store applications at -25°C, slope angles are slightly increased to compensate for higher lubricant viscosity within roller bearings.
Can poor-quality or damaged wooden pallets run on gravity flow beds?
Gravity flow systems rely on consistent surface contact across the bottom runners. Loose nails, warped boards, or split stringers will snag between rollers, leading to lane blockages. For operations using mixed-quality timber pallets, full-width steel roller tracks are recommended instead of twin skate rails, alongside heavy-duty guide flanges and secondary brake rollers spaced every one pallet length.
How does carton flow improve picking speed compared to static shelving?
Carton flow separates loading and picking personnel into two separate aisles. Stockers work in the rear charge aisle without obstructing pickers working along the front discharge face. With gravity naturally advancing cases forward as items are picked, travel times drop by up to 60%, restocking interference falls to zero, and picking accuracy increases significantly.
What structural safety codes and standards apply to HEDA flow racks?
All our industrial flow systems adhere strictly to EN 15512 (Steel Static Storage Systems European Standard), the RMI (Rack Manufacturers Institute) specification, and ISO 9001:2015 quality management procedures. Upright columns, bracing sections, and beam connectors undergo third-party destructive shear and moment-rotation testing, fully certified under CE marking No. 2435-CPR-8605159.
What is the maximum lane depth achievable in pallet flow installations?
Standard pallet flow lanes typically range from 3 to 15 pallets deep. However, with integrated speed controllers (centrifugal brake rollers) installed at every pallet interval and heavy-duty mechanical end separators, lanes can be safely extended up to 25 pallets deep. This creates substantial live storage buffers without requiring intermediate access aisles.
How are flow rack systems delivered and erected internationally?
Components are delivered flat-packed in containerized bundles organized by sub-assemblies. All roller beds arrive pre-assembled within their guide channels to minimize on-site installation labor. Upright trusses and horizontal beams are pre-drilled and tagged to match detailed 3D installation blueprints, step-by-step video manuals, and engineer supervision packages.
Request an Engineered Gravity Flow Layout & Project Quotation
Our engineering design department provides complimentary CAD layout optimization, track incline slope calculations, and pallet position density analyses tailored to your facility parameters within 24 hours.