Technical Data Matrix
Engineering Comparison: Heavy-Duty Industrial Racking Architectures
Shortlist optimal structural topologies based on floor area utilization, accessibility index, operational throughput velocity, and load limits per bay.
| Racking Architecture |
Direct SKU Accessibility |
Storage Volume Density |
Handling Fleet Requirements |
Standard Bay Capacity |
Typical Applications |
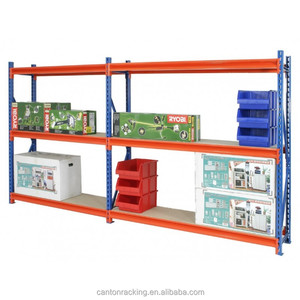
| Selective Pallet Racking |
100% Direct Access |
Moderate (35–45%) |
Counterbalance, Reach Trucks |
Up to 24,000 kg |
High-SKU 3PL, FMCG, Omnichannel Hubs |
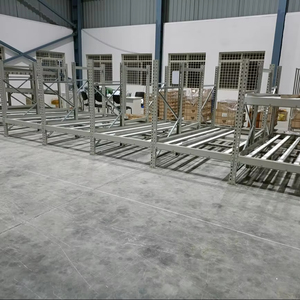
| FIFO Gravity Flow Racking |
Loading / Discharge Face |
Very High (70–85%) |
Standard Reach / Counterbalance |
Up to 15,000 kg/Lane |
Perishables, Dairy, Pharma, High Turnover |
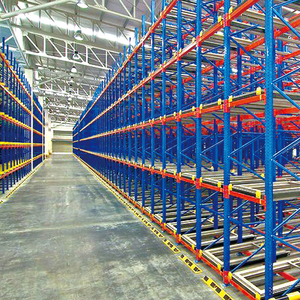
| LIFO Push Back Racking |
Front Lane Access (2–6 Deep) |
High (65–75%) |
Standard Counterbalance Forklifts |
1,500 kg per Cart |
Batch Processing, Cold Storage, Medium SKUs |
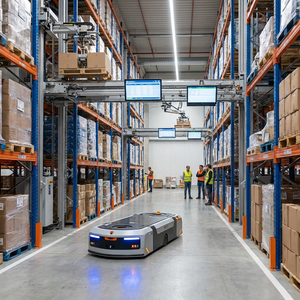
| Radio Shuttle Automation |
Automated Lane Shuttle |
Maximum (80–90%) |
Shuttle Unit + Transfer Forklift |
Unlimited Deep Lanes |
Cold Stores (-25°C), Beverage Bottling, Raw Agro |
| Very Narrow Aisle (VNA) |
100% Direct Access |
Very High (Vertical >16m) |
Man-Up / Man-Down VNA Turret Trucks |
Up to 26,000 kg |
Expensive Land Sites, Critical Parcel Depots |
| Structural Cantilever |
Continuous Front Plane |
Optimized for Length |
Side Loaders, 4-Way Reach Trucks |
3,000 kg+ per Arm |
Steel Tubing, Timber, Extrusions, PVC Pipes |
Procurement Horizons
Future Industrial Racking Procurement Trends (2026–2030)
Capital asset planners and procurement directors are adapting to shifting regulatory frameworks, rising land valuations, and rapid advances in smart warehouse automation.
AS/RS Hybrid-Ready Modular Uprights
Buyers now favor cold-rolled upright columns engineered with automated system interfaces, enabling warehouses to transition smoothly from manual forklifts to autonomous shuttle fleets without replacing structural frames.
Decarbonized & Green Steel Sourcing
ESG compliance requires mill-certified, low-carbon cold-rolled coil inputs. Environmental Product Declarations (EPDs) are becoming standard tender prerequisites for enterprise logistics parks aiming for LEED or BREEAM certifications.
Structural Health Telemetry & IoT
Next-generation uprights incorporate wireless strain gauges and deflection sensors. These telemetry units warn facility engineers of forklift impact loads, uneven weight distribution, or floor subsidence before structural failure occurs.
Advanced Metallurgy
Technological Frontiers in Industrial Racking Production
Modern racking integrity relies on precision metallurgy, automated continuous roll-forming tolerances, and advanced multi-stage chemical surface protection.
Industrial racking systems operate under extreme, continuous mechanical loads. Every structural beam, connector, and upright section must sustain static dead loads, dynamic forklift impacts, and seismic forces without catastrophic deflection. Global standards such as EN 15512:2020 in Europe and RMI ANSI MH16.1 in North America require rigorous limit-state design principles to ensure reliable real-world performance.
"Structural integrity in modern high-density warehousing is governed by cold-work hardening throughout multi-stage roll-forming lines. This process delivers superior torsional stiffness across the cross-section while optimizing total steel tonnage."
Precision 10-Stage Manufacturing Workflow
HEDA Shelves enforces a closed-loop, quality-controlled manufacturing cycle spanning raw coil verification to export-secure bundling. This ensures every component arriving at your regional port meets strict dimensional tolerances and load ratings.
 01. INCOMING COIL
High-Tensile Q235B/Q355B Steel
 02. SLITTING
High-Precision CNC Stripping
 03. PUNCHING
Automated 50/75mm Pitch Line
 04. COLD BENDING
Controlled Strain-Hardening
 05. ROLL FORMING
Omega & Box Beam Profiles
 06. POLISHING
Edge Deburring & Cleaning
 07. ROBOT WELDING
High-Integrity Beam Claws
 08. PRETREATMENT
Acid Pickling & Phosphating
 09. COATING
Epoxy Electrostatic Spray (80–120μm)
 10. QC & CRATING
Full Batch Testing & Export Stacking
Corrosion Mitigation in Challenging Environments
Warehouses in coastal ports and tropical regions face high relative humidity and airborne salinity that accelerate steel oxidation. Standard single-coat paints can micro-crack within months, compromising load capacity.
HEDA Shelves eliminates this vulnerability by passing all formed members through an automated chemical bath. This multi-stage process strips scale, micro-etches the steel, and deposits a dense zinc-iron phosphate conversion coating. A high-durability thermosetting epoxy-polyester powder coat is then electrostatically applied and cured at 200°C, producing a non-porous 80–120 micron shield that resists impact, abrasion, and aggressive industrial environments.
Procurement Due Diligence
Frequently Asked Questions: Industrial Warehouse Racking Procurement
Direct technical answers to common queries regarding international shipping, structural calculations, slab load bearing, and engineering compliance.
Q
What baseline structural data is required to generate a custom warehouse CAD layout?
To produce an engineered proposal within 24 hours, our design office requires: (1) Architectural floor plan (AutoCAD dwg or PDF) showing building column grids, dock locations, and clear ceiling heights; (2) Pallet specifications (width, depth, overall load height, and maximum tare weight); (3) Material handling equipment specifications (forklift type, turning radius, and maximum mast reach); and (4) Site seismic zone or building slab thickness/reinforcement details.
Q
How do you verify rack safety under high-risk seismic or soil conditions?
Calculations adhere to EN 15512 or RMI specifications using finite-element simulation tools. We analyze dynamic ground acceleration (spectral response curves) for your specific project coordinates, engineer oversized ductile base plates, upgrade anchor bolt embedment depths, and add cross-aisle portal bracing to prevent structural resonance during seismic events.
Q
What ocean export packaging standards are used to protect coatings during sea freight?
All upright frames and beams are separated by non-abrasive foam spacers, banded with high-tensile steel strapping, and wrapped in heavy-duty polyethylene stretch film. Structural steel feet and accessories are packed into heavy-duty fumigated wooden crates or steel cages, preventing mechanical abrasion and salt spray exposure during transit.
Q
Can your selective and drive-in racks integrate with existing competitor systems?
Yes. We operate custom CNC tooling profiles capable of producing teardrop, diamond, omega, and slotted hole pitches that match legacy installations. We frequently engineer extension bays and replacement parts for third-party systems while verifying structural continuity and load compatibility.
Q
What are the minimum concrete slab specifications for heavy-duty industrial racking?
For standard selective racking up to 8 meters tall, we typically recommend a reinforced concrete slab of at least 150–200mm thickness with a compressive strength of C20/25 to C25/30, rated for point loads of 40–80 kN per leg. For automated VNA or high-bay systems exceeding 12 meters, slabs must be engineered to DIN 18202 / EN 15620 flatness tolerances to prevent mast sway.
Q
What warranty terms and quality inspection documentation accompany each shipment?
Every commercial order includes factory mill test certificates (MTC) verifying steel composition, coating adhesion test reports, and formal CE/ISO compliance declarations. All structural steel elements carry a comprehensive 5-to-10-year manufacturer warranty against weld cracking and premature material failure under rated loads.