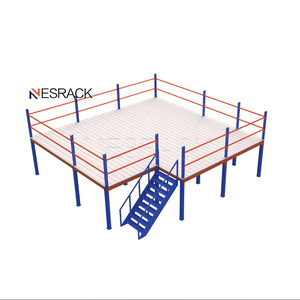
Attic Platform Heavy-Duty Second Floor Mezzanine
Multi-tier structural mezzanine engineered to expand vertical space by up to 100%, handling 300–1,000 kg/m² loads.
Precision-fabricated gravity flow beds, radio shuttles, and integrated multi-tier mezzanine frameworks engineered to EN 15512 and ISO standards.
Multi-tier structural mezzanine engineered to expand vertical space by up to 100%, handling 300–1,000 kg/m² loads.
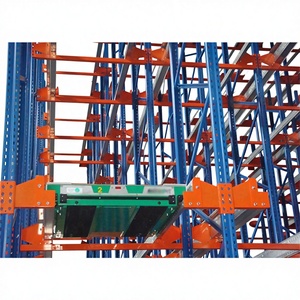
Semi-automated deep lane pallet shuttle system for ultra-dense cold chain and FMCG buffers with FIFO/LIFO versatility.
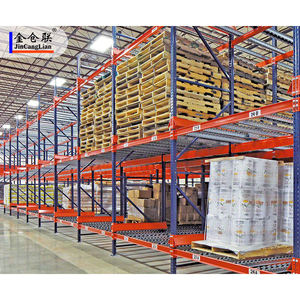
Engineered roller tracks with integrated centrifugal brake drums, ensuring automatic pallet travel and flawless FIFO stock rotation.
Modular steel structural system optimized for order fulfillment hubs, high-density tote sorting, and spare-parts depots.
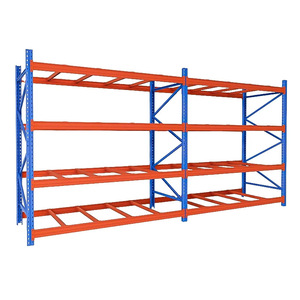
Precision-punched 50mm/75mm pitch upright frames with load-bearing box beams up to 4,500 kg per storage pair.
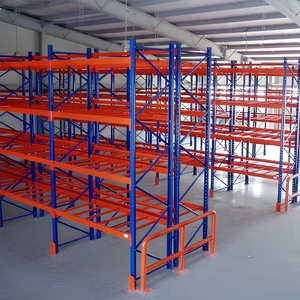
Tough electrostatic powder-coated finishing over phosphated cold-rolled steel, engineered for tropical, coastal, and chemical facilities.
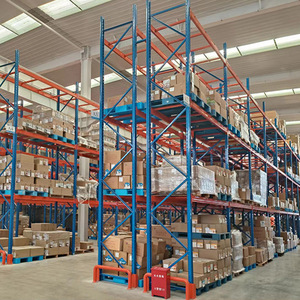
Standard North American tear drop punch profile with universal beam connectors, heavy return lips, and safety pin locking.
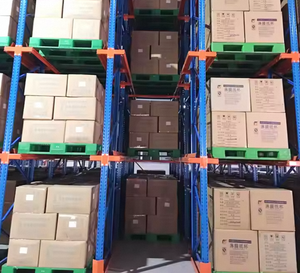
High-bay very narrow aisle configurations reaching 15m heights, maximizing cubic storage density while maintaining 100% selectivity.
A multi-factor engineering audit covering cold-formed steel integrity, dynamic roller testing, safety compliance, and direct factory pricing.
| Manufacturer / Supplier | Primary Manufacturing Base | Specialized Core Technology | Certifications | Engineering Strengths & Export Reach |
|---|---|---|---|---|
| Guangzhou HEDA Shelves Co., Ltd. | Guangzhou, China (30,000 m²) | Heavy-Duty Gravity Pallet Flow & Shuttle Hybrid | CE (2435-CPR-8605159) / ISO 9001 / RoHS | Factory-direct pricing, 24h custom CAD layouts, extreme humidity anti-corrosion finishes, high South Asia & global export volume. |
| Interroll Group | Sant'Antonino, Switzerland | Pallet Flow Magnetic Speed Controllers & Rollers | ISO 9001 / CE / UL | Global market benchmark for roller component manufacturing, high capital expenditure profile, premium conveyor integrations. |
| Bito-Lagertechnik Bittmann GmbH | Meisenheim, Germany | Continuous Carton Flow & Multi-Tier Flow Frames | TÜV / ISO 9001 / EN 15512 | Robust European structural compliance, tailored pharmaceutical flow picking tunnels, high ergonomic design tolerances. |
| Dexion (Gonvarri Material Handling) | Laubach, Germany / Madrid, Spain | Dynamic Flow Racks & Automated Storage Cells | EN 15512 / ISO 14001 / CE | Extensive engineering heritage across heavy European manufacturing lines, modular dynamic rail profiles. |
| Mecalux, S.A. | Barcelona, Spain / Chicago, USA | Pallet Flow, Carton Flow & WMS Software Systems | ISO 9001 / RMI / CE | Large multinational footprint, proprietary warehouse execution and software stack, global turnkey execution. |
| SSI Schaefer | Neunkirchen, Germany | Dynamic Live Storage Racking & Pick-to-Light Flow | ISO 9001 / CE / DIN | High-throughput distribution center integrators, advanced automation hardware, premium enterprise tier capital projects. |
| Stow Group | Dottignies, Belgium | Heavy Duty Pallet Flow Tracks & Shuttle Integration | EN 15512 / ISO 9001 | Standardized cold-formed profiles, extensive distributor networks throughout EMEA and the Americas. |
| Advance Storage Products | California, USA | Full-Lane Deep Roller Gravity Pallet Flow Beds | RMI Certified / ANSI MH16.1 | Specializes in deep freeze (cold storage) multi-lane pallet flow lines with heavy impact plate protection. |
| Nedcon (Steel Dynamics Group) | Doetinchem, Netherlands | Complex Flow Mezzanines & Dynamic Live Storage | EN 1090 / ISO 9001 | Specialized in high-bay structural platform flow integration and high-speed multi-level automated picking systems. |
| Unarco Material Handling | Tennessee, USA | T-Bolt & Interchangeable Flow Through Rack Systems | RMI / ISO 9001 | Broad US footprint, extensive carton flow configurations for parcel and retail consolidation facilities. |
Dynamic flow through racking relies on gravitational mechanics to advance unit loads smoothly along a declining slope without structural distortion.
A standard gradient of 3% to 4% (approx. 1:25) is engineered into the roller bed. Speed-braking rollers must be calibrated against the gross pallet mass to prevent runaway acceleration, ensuring pallets travel at a safe, uniform speed under 0.3 m/s.
Dynamic gravity beds demand pallets with consistent bottom runners (e.g., Euro or GMA standard). Any bottom board deflection exceeding L/200 creates high point friction, causing hang-ups. Skid runners, slave boards, or full-width steel rollers resolve non-uniform pallet challenges.
At the discharge face, significant back-pressure accumulates from rear pallets. Mechanically linked pallet separators isolate the lead pallet from upstream line pressure, allowing forklifts to extract loads without frictional drag or structural tipping hazards.
Forward-thinking supply chain managers are shifting from static storage to dynamic, low-carbon, and automation-integrated systems.
Refrigerated warehouse real estate costs 3-5x more to operate. Flow through racking slashes cubic air space by up to 45% compared to selective racking, cutting refrigeration loads and ensuring seamless First-In, First-Out (FIFO) turnover for temperature-sensitive perishables.
Modern fulfillment yards are adopting autonomous mobile robots. New flow rack procurement contracts demand optical locating pins and mechanical docking bays at charge and pick faces, enabling AGVs to load and retrieve without human intervention.
Rising carbon taxes and cross-border adjustments prioritize factories using certified Q355B low-alloy steel. Cold roll-forming profiles reduce raw steel mass while preserving equivalent section modulus and moment-carrying capacity.
With international ocean logistics driving landed costs, savvy global procurement teams insist on pre-nested upright bundles and modular bolt-free roller cassettes to maximize 40HQ container utilization rates up to 96%.
Controlling the entire value stream from flat coil uncoiling to final protective sea packaging in Guangzhou, South China.
Since 2001, HEDA Shelves has operated an integrated 30,000 m² manufacturing plant with automated roll-forming lines, computerized continuous punching, and robot-welded beam connectors, delivering unmatched production consistency.
Our structures comply with verified international audits: CE Certification No. 2435-CPR-8605159, ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and full RoHS compliance across electrostatic powder-coated surfaces.
Every beam and column passes through automated pickling and chemical phosphating tanks prior to industrial thermosetting powder curing, delivering superior salt-spray and high-humidity protection for harsh maritime and coastal distribution zones.
Essential guidance for warehouse operators, structural engineers, and industrial procurement professionals.
Pallet flow requires two dedicated working aisles: a charging (loading) aisle and a picking (discharge) face, making it a true First-In, First-Out (FIFO) gravity system. Push-back utilizes nested carts or inclined rollers operating from a single loading aisle, functioning as a Last-In, First-Out (LIFO) arrangement where incoming pallets push existing inventory deeper into the rack lane.
To provide certified structural calculations and CAD models, our engineering team requires: (1) Warehouse building DWG/PDF drawings indicating clear ceiling heights and column grids, (2) Floor slab concrete compressive strength (e.g., C25/C30) and slab thickness, (3) Pallet footprint dimensions, bottom board orientations, and gross load weights (e.g., 1,000–1,500 kg), and (4) Forklift specifications including mast lift height and turning radius.
Structural steel framing undergoes acid pickling and immersion phosphating before electrostatically applying industrial-grade polyester powders cured at 200°C. For deep freeze environments down to -30°C or high-salinity ports (such as Colombo, Chennai, or Chattogram), hot-dip galvanization is specified on roller housings, upright bases, and mechanical brake drums to eliminate galvanic and surface oxidation.
All structural components are individually tagged with numbered project codes matching isometric 3D assembly drawings and bill-of-materials (BOM) documentation. Step-by-step video procedures are provided for local contractors. For large multi-tier platforms or extensive dynamic installations, senior HEDA field engineers can be deployed on-site to direct erection, plumb columns, torque anchors, and calibrate brake roll velocities.
Consult directly with our structural engineering team. Receive comprehensive CAD layouts, 3D renderings, and transparent container-optimized quotes within 24 hours.