Featured Industrial Pallet Racking & Commercial Storage Solutions
Explore our factory-engineered storage systems manufactured to CE, ISO 9001:2015, and international warehouse safety standards. Each structural profile delivers verifiable steel load ratings, cold-formed Q235B/Q355B tensile resilience, and modular expandability.
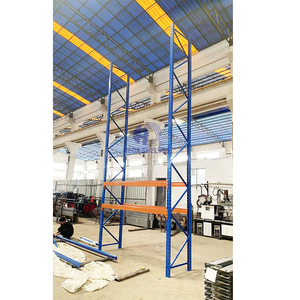
Engineering Dynamics of Tall Pallet Racking in High-Bay Intralogistics
Designing racking structures exceeding 8 to 30 meters requires advanced structural mechanical modeling, finite element analysis (FEA), second-order P-Delta moment evaluations, and stringent dynamic deflection control.
1. Structural Mechanics, Slenderness Ratios & Beam-to-Column Connection Stiffness
Modern tall pallet racking systems—often deployed as Very Narrow Aisle (VNA) configurations, clad-rack warehouses (rack-supported buildings), or Automated Storage and Retrieval Systems (AS/RS)—operate under severe mechanical stress profiles. Unlike conventional low-rise shelving where static down-aisle loads predominate, tall pallet racking structures face complex interactions between gravitational dead loads, variable pallet live loads, forklift operational impact, wind loads (in clad structures), and seismic accelerations.
As structural height scales above 12 meters, the column slenderness ratio (λ = kL / r) becomes the primary governing criterion in structural stability. To prevent localized torsional buckling and systemic Euler column failure, HEDA utilizes cold-formed closed-box or multi-flanged Omega-profile uprights engineered from premium structural steels (Q235B and Q355B). Our column upright sections feature continuous multi-bend stiffening ribs along the web and flanges, drastically increasing the section modulus (Z) and radius of gyration (r) without introducing deadweight overhead.
Furthermore, the beam-to-column connector is modeled as a semi-rigid joint. The rotational stiffness (Ci) of the multi-claw connector bracket directly dictates down-aisle frame sway and load redistribution. Through extensive physical testing in accordance with EN 15512:2020 and RMI ANSI MH16.1 specifications, our proprietary 4-claw and 5-claw high-tensile connectors achieve high initial rotational stiffness with positive mechanical lock-pin engagement, ensuring systemic safety factors exceeding 1.5 to 2.0 under maximum combined stress states.
2. Seismic Resilience, Base Plate Engineering & Concrete Slab Anchoring Dynamics
In tall pallet racking installations, vertical loads transform into immense overturning moments at the base plate. Under seismic event excitation, ground spectral acceleration (Ss and S1) transmits shear waves through the concrete foundation slab into the upright frame. HEDA's structural engineers perform dynamic response spectrum analyses to model how cross-aisle diagonal bracing and top tie-beams dampen vibration harmonics.
Our heavy-duty base plates utilize thickened structural steel plates (10mm to 20mm thickness) precision-welded with load-distributing gusset stiffeners. High-strength chemical wedge anchors (Grade 8.8 or 10.9) ensure seismic pull-out resistance against concrete breakout and pull-through modes. When installed on slabs with compressive strengths between 25 to 35 MPa, our anchor configurations safely transfer dynamic overturning moments directly into the structural foundation without risk of localized slab micro-fracturing.
- Finite Element Analysis (FEA) verified beam deflections maintained within strict L/200 to L/300 serviceability limits.
- Automated CNC roll-forming lines delivering profile length tolerances within ±0.5mm across 15-meter upright spans.
- 100% full-penetration robotic continuous welding on heavy-duty beam connector endplates and base shoe assemblies.
- Surface treatment via 10-stage automated pickling, phosphating, and nano-ceramic bonding before electrostatic cure.
Full-Spectrum OEM & ODM Customization Capabilities
From bespoke upright punching geometries to specialized high-density pallet runners, our in-house engineering team provides end-to-end original equipment and design manufacturing for global tier-one supply chains.
Custom Profile Geometry
OEM development of proprietary upright and beam sections, custom pitch punching (50mm, 75mm, 76.2mm teardrop), and unique nesting tolerances for automated racking frames.
Full CAD / 3D BIM Modeling
Rapid 24-hour turnaround for parametric architectural CAD layouts, structural calculations, Tekla/Revit BIM files, and realistic 3D volumetric warehouse simulations.
Surface Coating Formulations
Tailored electrostatic thermosetting polyester powder coatings (60–90 μm), hot-dip galvanization for sub-zero freezer cold stores, and high-salinity marine air barrier finishes.
Private Label & Packaging
Complete OEM private labeling, custom steel stamping, localized assembly manuals, and container-optimized steel nesting bundles designed to reduce landed shipping costs.
10-Stage Precision Manufacturing Workflow
Strict in-house quality control across every metallurgical stage ensures zero defect tolerance and millimeter-level alignment across multi-kilometer rack installations.
 STEP 01
Raw Materials
Mill-certified Q235B/Q355B coils verified for tensile yield strength.
 STEP 02
Precision Slitting
High-speed longitudinal slitting ensuring laser-straight strip widths.
 STEP 03
CNC Punching
Continuous multi-station high-speed mechanical hole punching.
 STEP 04
Cold Bending
Multi-roller forming providing high residual structural rigidity.
 STEP 05
Roll Forming
Continuous automatic roll-forming of uprights and step beams.
 STEP 06
Deburring & Polish
Automated edge grinding and weld spatter removal for safety.
 STEP 07
Robotic Welding
Precision robotic MIG welding of beam brackets and base plates.
 STEP 08
Chemical Pretreatment
Multi-stage acid pickling, degreasing, and rust-inhibiting phosphating.
 STEP 09
Powder Coating
Electrostatic spray guns curing tough polyester coats at 200°C.
 STEP 10
QA & Export Loading
Rigid thickness testing, load checks, strapped export bundling.
Future Logistics Trends & Tall Pallet Racking Procurement Evolution
Warehousing operations across the Americas, Europe, Middle East, and Asia-Pacific are transitioning from conventional low-density floor storage to highly automated, vertically intensive logistics architectures.
1. Vertical Density & Land Scarcity
Skyrocketing industrial real estate costs are pushing warehouse clear heights from 9 meters toward 18–35 meters. Tall racking structures maximize vertical volumetric cube utilization, delivering over 250% higher pallet density per square meter of expensive concrete floor footprint.
2. Automation Readiness (ASRS & AMR)
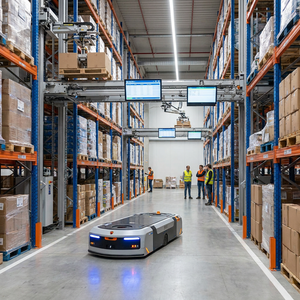
Modern tall racking is no longer static steel; it serves as precision trackways for automated crane systems, autonomous mobile robots (AMRs), and 4-way radio shuttles. Manufacturing tolerances must be tightened to sub-millimeter scales to prevent optical sensor tripping and robotic positioning faults.
3. ESG & Low-Carbon Structural Steel
Procurement frameworks now audit the embedded carbon footprint of warehouse fixtures. HEDA works with electric-arc furnace (EAF) steel suppliers and utilizes non-toxic, VOC-free thermoset powder coats, reducing life-cycle carbon emissions while meeting strict corporate sustainability benchmarks.
4. Climate & Coastal Durability
Global logistics hubs located in tropical, monsoonal, or coastal zones demand elevated anti-corrosion barriers. Multi-stage chemical phosphating and hot-dip galvanized specifications safeguard tall high-bay frameworks against humidity-induced oxidation, salt fog, and chemical vapor degradation.
Engineering Comparison Matrix: High-Bay & Tall Racking Systems
Evaluate critical operating parameters, access efficiency, density indices, and material handling equipment (MHE) prerequisites to select the optimal racking topology.
| Racking Topology | Maximum Height Range | Pallet Accessibility | Volumetric Space Density | Required Forklift / MHE | Ideal Sector Applications |
|---|---|---|---|---|---|
| Tall Selective Pallet Rack | Up to 14 meters | 100% Direct Access | Medium (~50-60%) | Standard Counterbalance / Reach Truck | 3PL, FMCG, E-Commerce Multi-SKU Distribution |
| Very Narrow Aisle (VNA) | Up to 18 meters | 100% Direct Access | High (~75-85%) | VNA Turret Truck (Wire / Rail Guided) | High-Density Regional Distribution Centers, Pharma |
| Radio Shuttle High-Bay | Up to 24 meters | Lane-Based (FIFO / LIFO) | Ultra-High (~85-92%) | Standard Forklift + Automated Shuttle Car | Cold Storage, Food & Beverage, Seasonal Bulk Reserves |
| Double-Deep Pallet Rack | Up to 12 meters | 50% Direct Access | High (~65-75%) | Deep-Reach Pantograph Forklift | General Manufacturing Buffers, Paper & Packaging |
| Automated AS/RS Clad Rack | Up to 35+ meters | 100% Automated Access | Maximum (>95%) | Fully Automated Stacker Cranes (SRM) | Mega Fulfillment Hubs, Heavy Automotive, Petrochemical |
| Rack-Supported Mezzanine | Multi-Tier (2-4 Floors) | Manual / Cart Picking | Dual-Purpose Multi-Level | Freight Lifts, Conveyors, Manual Order Pickers | Garment Retail, Small Parts, Spare Components, Returns |
Why Global Procurement Directors Partner with Guangzhou Heda Shelves
With over two decades of localized engineering expertise and containerized export reach across more than 120 countries, HEDA Shelves bridges high-capacity precision manufacturing with rigorous structural safety certifications.
Verifiable Global Certifications
Fully accredited with CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and RoHS environmental compliance for strict regulatory compliance in Europe, the Americas, and APAC.
30,000 Ton Monthly Capacity
Spanning 30,000 m² of modern production facilities in Guangzhou, our automated slitting, punching, cold-roll forming, and coating lines guarantee on-time container staging for large multi-thousand-bay logistics infrastructure projects.
Export Packing & Turnkey Support
Precision bundling designed to maximize 40HQ container load factors, bundled with clear component numbering, comprehensive CAD assembly blueprints, step-by-step video instructions, and remote or on-site engineering supervision.
Frequently Asked Questions: Technical Sourcing of Tall Pallet Racks
Authoritative guidance on floor loading dynamics, seismic calculations, fire suppression integration, and shipping logistics.
High-bay installations require floor slabs designed for heavy concentrated point loads and punch shear. A minimum slab thickness of 200mm to 250mm with Grade C25/30 or C30/37 concrete (compressive strength 25–35 MPa) is typically required. For Very Narrow Aisle (VNA) systems, slab floor flatness must strictly adhere to DIN 18202 Table 3, Group 4 or TR34 (FM1 / FM2 specifications) to prevent high-mast oscillation and turret mast deflection during elevated travel.
When racking clear height exceeds 9 to 12 meters, standard ceiling-mounted ESFR (Early Suppression Fast Response) sprinklers may suffer from thermal draft delay and water plume dissipation. HEDA integrates dedicated longitudinal and transverse sprinkler pipe pathways directly behind pallet back-stops and inside intermediate horizontal frame bracings. This provides rigid mounting points and pipe clearance protecting fire suppression hardware from accidental forklift tine contact.
We model seismic performance utilizing finite element response spectrum calculations compliant with EN 16681, RMI ANSI MH16.1, and local building codes (e.g., IBC or IS 1893). Parameters include site soil profile class, spectral response accelerations (Ss and S1), and the structural behavior factor (q). Cross-aisle diagonal bracing patterns, horizontal top-tie trusses, and heavy-duty seismic base plates are structurally proportioned to dissipate kinetic energy while maintaining elastic stability.
Standard pallet racking operates within general manufacturing tolerances of ±2.0mm. In tall VNA and ASRS automated racks, cumulative tolerances can cause high-mast collisions or robotic optical sensor misalignment. HEDA enforces strict CNC roll-forming tolerances: upright column length within ±0.5mm, hole pitch spacing within ±0.1mm, and frame plumbness within H/1000 or tighter. This level of precision eliminates sway and ensures continuous, unhindered automated shuttle travel.
Every structural component undergoes a thorough 10-stage automated pre-treatment protocol including industrial degreasing, hot acid pickling to eliminate mill scale, and zinc phosphating or nano-ceramic conversion. Our electrostatically applied polyester powder coating is baked at 200°C to achieve a dry film thickness of 60 to 90 microns. Components pass standardized 500-hour neutral salt-spray (ASTM B117) tests. For outdoor yards or sub-zero freezer cold storage, hot-dip galvanization is available.
Uprights and beam profiles are nested in specialized steel-strapped bundles with heavy protective corrugated interleaves, shock-absorbing corner pads, and moisture-barrier stretch wrap. Heavy uprights are positioned with reinforced dunnage for forklift tines to facilitate safe, rapid devanning at destination ports. By optimizing 40ft High Cube (40HQ) volumetric loading ratios, HEDA reduces per-pallet freight landed costs significantly for international procurement directors.