Industrial Heavy-Duty Storage Racking Series
Certified cold-rolled structural steel storage configurations fabricated in our 30,000 m² automated facility. Fully customizable dimensions, load ratings from 500 kg to 5,000 kg per level, and anti-corrosion electrostatic epoxy powder finishes.
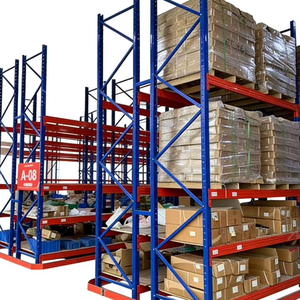
Heavy-Duty Cold Rolled Steel Epoxy Coated Warehouse Rack Shelves
Precision-engineered using Q235B high-tensile cold-rolled steel with electrostatic thermoset epoxy coating. Ideal for express distribution hubs, basement depots, and high-density manufacturing parts storage.
- Standard Load:800 - 2,500 kg / level
- Pitch Adjustability:50mm / 75mm increment
- Surface Pretreatment:9-Stage Pickling & Phosphating
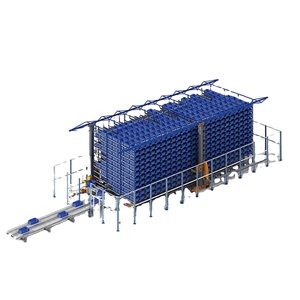
Automated Pallet ASRS Warehouse Storage & Retrieval System
High-bay crane-compatible automated structural matrix engineered for high-throughput unmanned fulfillment centers. Millimeter-level profile tolerances ensure seamless interface with stacker cranes and WMS software.
- Clear Height:Up to 36 Meters
- Interface Standard:FEM 9.831 / EN 15512
- Pallet Capacities:500 - 1,500 kg / position
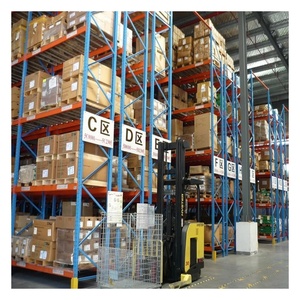
Heavy Duty Steel 5-Layer Bearing Stacking Pallet Rack System
Multi-tier structural steel racking featuring continuous roll-formed columns and heavy-duty box beams with 4-claw safety connector locks. Certified anti-corrosion protection for humid and high-traffic conditions.
- Layer Capacity:500 - 3,000 kg / level
- Deflection Tolerance:1/200th span under max load
- Safety Locking:Heavy-duty spring safety pins
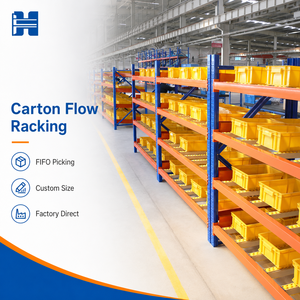
Carton Flow Rack System Gravity Roller Order Picking Shelves
Ergonomic gravity roller track layout engineered for pick-to-light sorting, e-commerce order fulfillment, and automotive assembly lines. Guarantees true First-In First-Out inventory turnover with zero energy consumption.
- Track Composition:Aluminum/Steel roller tracks
- Incline Ratio:3% to 5% slope gradients
- Picking Integration:Supports digital pick-to-light
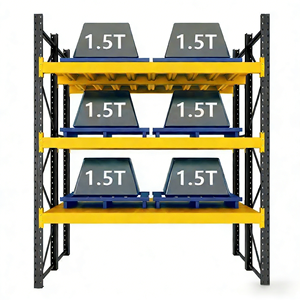
Customizable Heavy Duty Metal Warehouse Storage Shelves
Bespoke structural warehouse shelving tailored for specialized industrial parts, hardware wholesale, and manufacturing buffer storage. Supports wire mesh decking, steel panels, or drop-in cross-support bars.
- Modularity:100% boltless beam assembly
- Decking Media:Galvanized mesh / Zinc plates
- Upright Section:80x60 / 90x70 / 100x70 mm
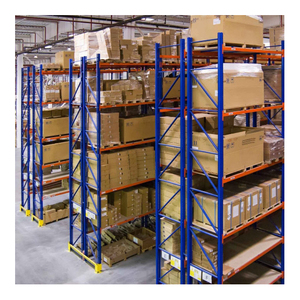
Peterack CE Certified Warehouse Heavy Duty Selective Racks
Certified selective pallet racking providing immediate 100% accessibility to every pallet location. Compatible with counterbalance forklifts, reach trucks, and narrow-aisle (VNA) material handling fleets.
- Compliance:CE No. 2435-CPR-8605159
- Accessibility:100% direct individual pallet pick
- Column Profiling:Omega-profile cold rolled
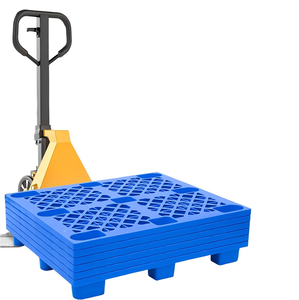
Industrial HDPE Pallet Storage Rack Anti-Static & Anti-Collision
Corrosion-proof hybrid racking integrating heavy-duty polymer impact absorption with cold-rolled steel framing. Engineered for chemical warehouses, pharmaceutical cold chains, and electrostatic-sensitive cleanrooms.
- Load Range:800 - 4,000 kg / bay
- Protection:Anti-static & shock absorption
- Chemical Resistance:Acid, alkali & oil resistant
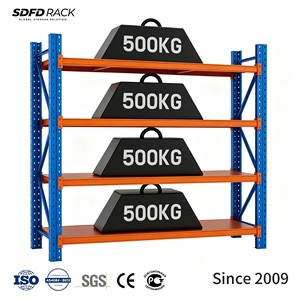
Custom Industrial Multi-Level Carpet Roll & Coil Beam Racking
Engineered open-span cradle beam system designed specifically for rolled textiles, cylindrical coils, and long industrial floor coverings. Eliminates pressure marks and roll distortion while maximizing vertical cubing.
- Beam Structure:Saddle cradle & pipe axle fittings
- Bay Lengths:Customizable up to 4.5m per span
- Safety Standard:AS 4084 / FEM 10.2.02
Why Global Supply Chains Trust Guangzhou Heda Shelves Co., Ltd.
Established in 2001, HEDA Shelves has evolved into an international powerhouse in storage engineering, providing complete turnkey logistics infrastructure from raw coil roll-forming to computerized finite element analysis (FEA).
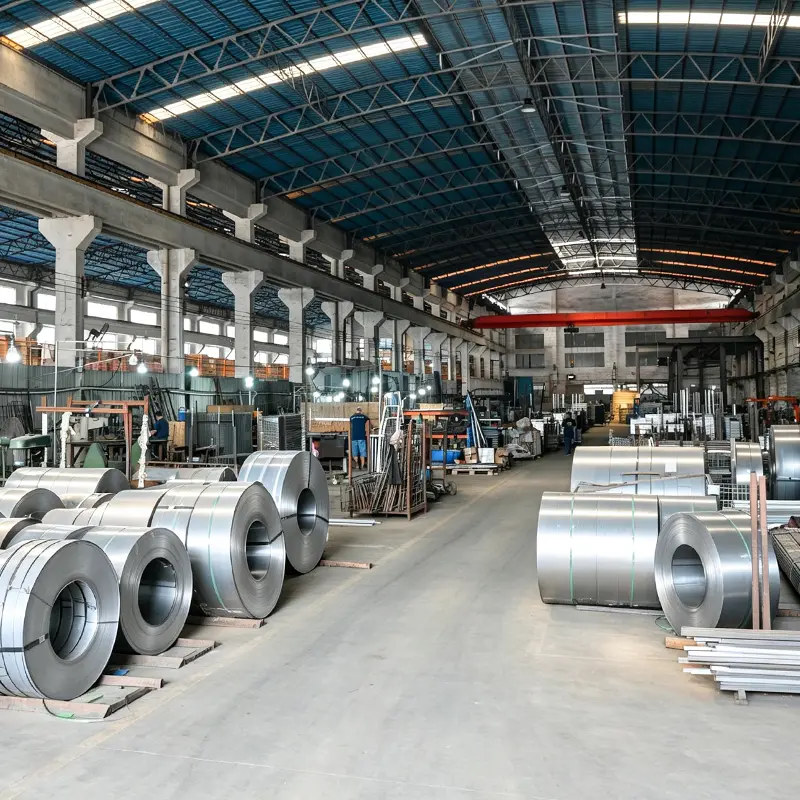
25+ Years Industrial Mastery
Over two decades of dedicated research and manufacturing excellence, delivering mission-critical warehousing systems across commercial logistics, retail distribution, cold-chain hubs, and global industrial manufacturing plants.
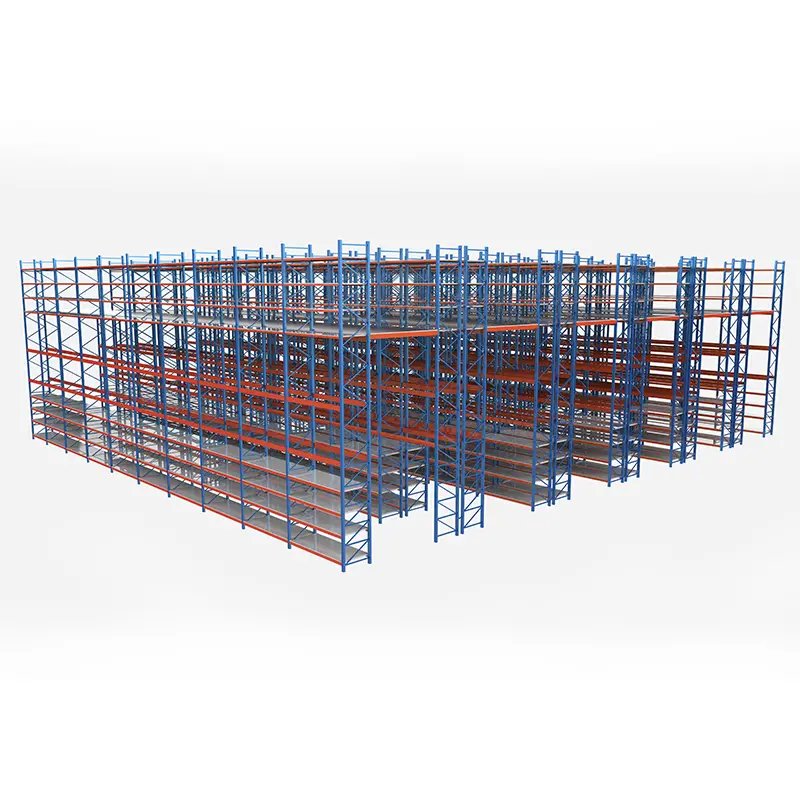
Complimentary CAD & 3D Design
Our dedicated team of certified structural engineers delivers comprehensive AutoCAD layouts, realistic 3D spatial simulations, and finite element stress analysis calculations within 24 hours to maximize cubic floor utilization.
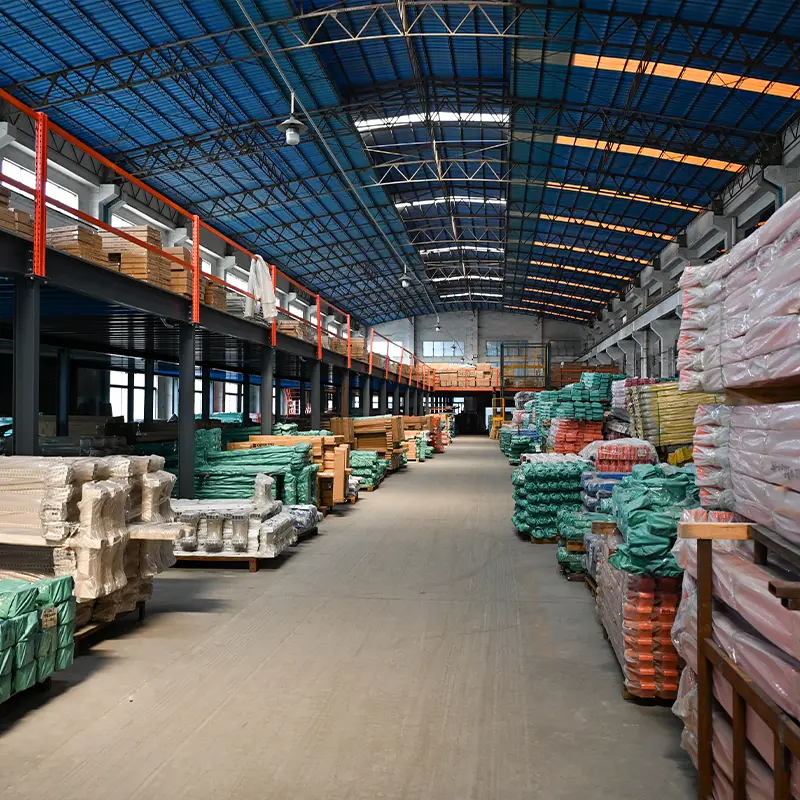
Certified Structural Durability
Rigorous quality control governed by CE certification (No. 2435-CPR-8605159), ISO 9001:2015 management systems (No. 18624Q00169R0M), and RoHS environmental standards. Every batch undergoes ultrasonic weld and tensile testing.
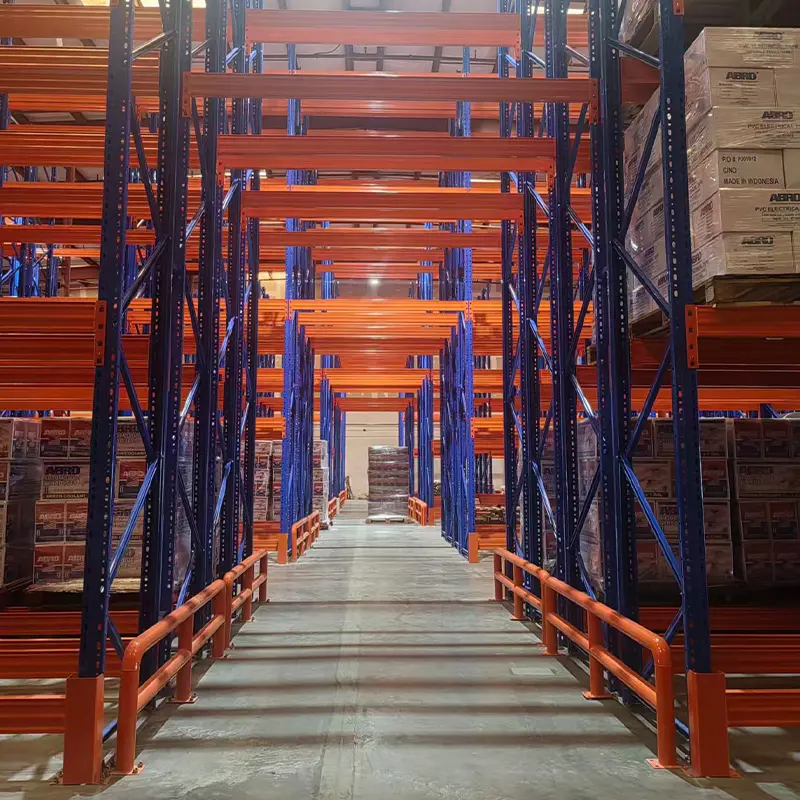
Bespoke OEM / ODM Tailoring
From custom punching pitch configurations and custom RAL powder coatings to specialized pallet runners and structural mezzanine multi-tier extensions, we configure every rack to your fleet requirements and seismic constraints.
Industrial Racking Architectural Comparison Matrix
Selecting the ideal storage typology requires balancing selectivity, density, capital expenditure per pallet position, and forklift material handling velocities. Evaluate systems according to industrial standards.
| Racking Architecture | Direct Selectivity | Volumetric Density | Rotation Logic | Aisle Width Reqt. | Ideal Procurement Use-Case |
|---|---|---|---|---|---|
| Selective Pallet Racking | 100% Direct | Moderate (40%) | FIFO / LIFO | 3.0 - 3.8 Meters | Fast-moving retail distribution, multi-SKU FMCG, 3PL logistics |
| Double Deep Pallet Racking | 50% Semi-Direct | High (60%) | FILO / LIFO | 3.0 - 3.4 Meters | Medium SKU volumes, wholesale dry storage, manufacturing buffers |
| Drive-In / Drive-Through | Lane Selective | Ultra-High (75%) | LIFO (Drive-In) / FIFO | Forklift Drives Inside | Cold storage, bulk beverages, agricultural food reserves |
| Radio Shuttle Cart Racking | Lane Selective | Maximum (85%) | Flexible FIFO / LIFO | Aisle for Mast Only | Deep-freeze warehousing (-25°C), high-value cold chain, pharmaceutical batches |
| Carton & Pallet Gravity Flow | Face Selective | Very High (70%) | Strict FIFO | Separated Load / Pick | Perishable food processing, cosmetics, date-sensitive batch picking |
| Very Narrow Aisle (VNA) | 100% Direct | High (65%) | FIFO / LIFO | 1.5 - 1.8 Meters (Guided) | High clear-height urban fulfillment hubs with high floor land values |
| Heavy Duty Cantilever Racking | 100% Unobstructed | Specialized | Free Access | Depends on Load Length | Steel pipes, extrusions, timber boards, coils, structural bar stock |
| Structural / Rack Mezzanine | 100% Multi-Level | Multiplies Floor x2/x3 | Hybrid Manual/Auto | Integrated Walkways | E-commerce bin shelving, returns processing, automotive spare parts depots |
Future Procurement Trends in Warehouse Storage Systems
Global supply chain leaders are shifting procurement criteria from baseline upfront price to holistic lifecycle resilience, environmental compliance, and rapid modular scalability. Key structural market dynamics include:
Total Cost of Ownership (TCO) Prioritization
Procurement teams are shifting away from lower-grade steel varieties toward high-tensile structural grades (Q355B / SS400). Higher yield strengths decrease structural tonnage while preserving rated beam deflections under heavy operational cycles, lowering long-term maintenance costs and floor slab subsidence risks.
Cold-Chain Density & Thermal Efficiency
With refrigerated warehousing electricity expenses escalating exponentially, cold-store developers are standardizing on Radio Shuttle and automated high-bay systems. Reducing cubic dead air reduces thermodynamic refrigeration run-time by up to 35%, driving massive long-term operating profit margin enhancements.
Containerized Ocean Freight Optimization
Direct OEM factory packing strategies now incorporate computerized 3D container bundling software. High-density steel bundling and nested upright designs optimize 40HQ ocean container weight-to-volume ratios, cutting international maritime transport expenses per pallet position by up to 22%.
Stringent ESG & VOC Compliance
Multinational enterprise buyers mandate non-toxic, TGIC-free electrostatic powder coatings complying with RoHS and REACH regulations. Closed-loop, zero-discharge pre-treatment lines with automated phosphating ensure structural environmental safety and superior salt-spray corrosion resistance.
Technological Evolution: From Static Iron to Automated Intralogistics
The industrial storage manufacturing sector has crossed an architectural threshold. Modern storage systems function not merely as passive structural steel frameworks, but as high-precision physical substrates for autonomous intralogistics robotics.
ASRS & AMR Robot-Ready Tolerances
Traditional racking tolerated installation deviations of ±3mm to ±5mm. With the explosive rise of Autonomous Mobile Robots (AMRs) and high-speed Automated Storage and Retrieval Systems (ASRS), precision roll-forming lines operate to tolerances within ±0.5mm across 12-meter continuous upright profiles.
- Laser-guided automated CNC punching lines
- Seamless optical track alignment for stacker cranes
- Deflection ratios calibrated to FEM 9.831 tolerances
Finite Element Analysis (FEA) & Seismic Design
Warehouse footprints are expanding into seismically active territories across Latin America, the Pacific Rim, and South Asia. Racking engineering relies on computerized 3D Finite Element Analysis (FEA) software to model second-order elastic deformation, torsional buckling, and joint stiffness under dynamic ground accelerations.
- Seismic design compliant with RMI MH16.1 & EN 16681
- Heavy-duty seismic baseplate anchoring systems
- High-ductility steel alloys resisting brittle fracture
Digital Twins & Dynamic Space Simulation
Modern warehouse design bypasses static paper drafts. Engineers generate dynamic Digital Twins representing the warehouse's structural envelope, column matrices, HVAC ducting, clear fire suppression sprinkler grids, and forklift swept paths to pre-emptively eliminate operational collisions.
- Clash detection with MEP & NFPA sprinkler networks
- Interactive 3D walkthrough models for project signoff
- Automated bill-of-materials (BOM) steel calculation
10-Stage High-Precision Manufacturing Process
Guangzhou Heda Shelves Co., Ltd. controls the complete manufacturing chain in-house. From certified strip steel inspection to final international seaworthy bundling, every manufacturing stage is audited under ISO 9001:2015 quality control protocols.
Raw Steel Analysis
Certified Q235B / Q355B coils verified via spectrometer.
Slitting & Cutting
CNC continuous slitting to precise strip widths (±0.1mm).
Automated Punching
High-speed continuous hydraulic punching for hole pitches.
Precision Roll Forming
Multi-station cold roll forming creates complex profiles.
Box Beam Interlocking
Twin-C profile seam welding ensures high deflection rigidity.
Robotic Joint Welding
Automatic multi-axis robotic welders bond beam end connectors.
Shot Blasting & Acid Wash
9-stage immersion bath removes mill scale and oxidization.
Electrostatic Coating
Automated powder spray booths apply 60-90μm epoxy resin.
Thermal Curing Tunnel
Cured at 180°C - 200°C for chemical scratch resistance.
QC & Seaworthy Pack
Dimension verification, protective wrap, and containerization.
Frequently Asked Questions for Warehouse Racking Procurement
Direct answers to core technical, architectural, structural, and international logistics questions submitted by warehouse developers, supply chain consultants, and industrial procurement committees.
What structural data is necessary to generate an initial CAD layout and price quotation?
To deliver an accurate architectural proposal and structural calculation, our engineering team requires: (1) Warehouse building footprint (AutoCAD or PDF) identifying column grid centers, clear internal height beneath rafters, dock door locations, and fire exit doors; (2) Unit load specifications: pallet width, depth, overall load height (including wooden/plastic skid), and gross weight per pallet; (3) Forklift material handling specifications, specifically aisle width turning radius requirements and maximum extended mast height; (4) Local seismic zone classifications and concrete floor slab thickness/compressive strength (e.g., 200mm slab @ 30 MPa).
How does HEDA Shelves ensure compliance with international structural racking codes?
Our structural calculation models conform strictly to European EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design), FEM 10.2.02, and American RMI (Rack Manufacturers Institute) MH16.1 specifications. Load limits undergo strict safety factor verification (typically 1.4 to 1.5 against ultimate tensile yield). We maintain factory-certified CE marking (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 quality assurance management, with third-party chemical and load testing certificates provided for project verification.
What is the standard beam deflection limit permitted under maximum operational loading?
In accordance with EN 15512 and RMI standards, the maximum allowable vertical elastic beam deflection must not exceed L/200, where 'L' represents the clear span distance between upright columns (e.g., for a 2,700mm pallet beam span, maximum permissible vertical deflection is 13.5mm under uniformly distributed load). For automated ASRS high-bay operations or automated crane interfacing, our engineers calibrate beam sections to higher structural stiffness thresholds of L/300 or L/400 to prevent automated optical sensor misalignment.
How are steel surfaces protected against coastal humidity and tropical corrosion?
HEDA Shelves implements a rigorous automated 9-stage pre-treatment line prior to coating. Components pass through degreasing, pickling, neutralizing, and zinc phosphating baths to eliminate all organic contaminants and micro-scale mill scale. Racks receive thermoset epoxy-polyester hybrid powder coating baked at 180°C–200°C, yielding a uniform dry film thickness of 60 to 90 microns that surpasses 500 hours of continuous salt-spray testing (ISO 9227). For external outdoor yards or sub-zero refrigeration, continuous hot-dip galvanizing (HDG) per ISO 1461 is available.
Can OEM/ODM components be manufactured to integrate with existing legacy racking brands?
Yes. HEDA Shelves provides extensive ODM and OEM reverse-engineering services. If your distribution center requires extensions or replacement beams/uprights compatible with major global systems (e.g., teardrop patterns, European 50mm pitch Omega profiles, or Australian 76.2mm pitch slots), our CNC tooling engineers configure bespoke punch dies and roll tooling to ensure structural interchangeability and load equivalence.
What is the standard production lead time and international container shipping packaging?
Standard factory production lead time for standard projects (1 to 5 forty-foot high cube containers) ranges between 15 and 25 calendar days following drawing signoff. All components are packaged using seaworthy bundling practices: upright frames and beams are nested with non-abrasive corrugated spacers, banded with heavy-duty tensioned steel strapping, and wrapped in water-resistant plastic stretch film. Baseplates and small connection hardware are packed into reinforced, labeled wooden crates for easy on-site inventory reconciliation.
Do you provide on-site installation guidance and overseas structural supervision?
Every export project is accompanied by detailed structural component drawings, anchor bolt torque charts, and sequenced 3D erection manuals with piece-mark numbering. For large-scale distribution projects or complex multi-tier mezzanine floors, HEDA Shelves deploys experienced structural installation supervisors directly to your project location to oversee local assembly crews, verify vertical plumbing tolerances, and ensure compliance with anchor pull-out torque standards.
What concrete slab properties and anchor specifications are mandated for heavy installations?
Standard heavy-duty selective and drive-in pallet racking installations require a continuous non-cracked, reinforced industrial concrete slab of minimum C20/25 or C25/30 grade (compressive strength 25 to 30 N/mm²), with a minimum slab thickness of 150mm to 200mm. Each upright footplate is secured using high-tensile wedge expansion anchors or concrete screw anchors sized in accordance with calculated baseplate overturning moments and seismic shear values.
Plan Your Storage Project with Certified Structural Engineers
Submit your warehouse layout drawings or logistics specifications today. Our engineering department will generate a customized AutoCAD space optimization layout, detailed bill of materials, and direct factory quotation within 24 hours.