Medium Duty
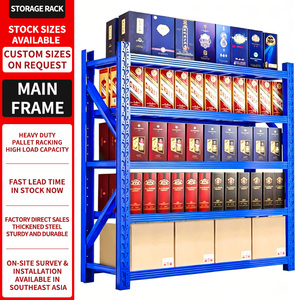
Direct factory manufacturing certified to CE and ISO 9001 standards. Explore our eight core structural racking architectures built with cold-rolled Q235B/Q355B steel, designed for maximum volume utilization and load safety.
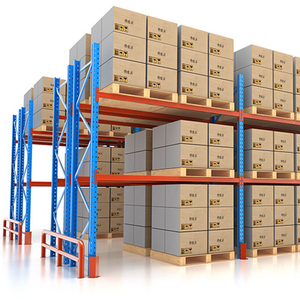
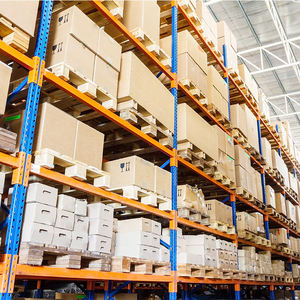
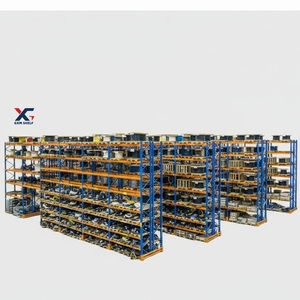
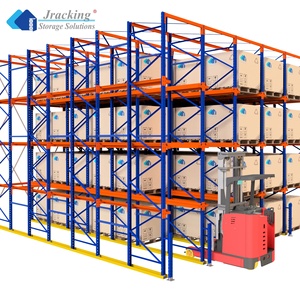
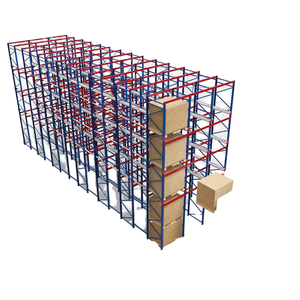
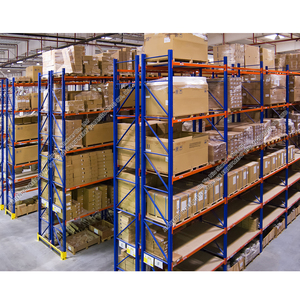
Modern warehouse racking is not simply structural steel shelving; it is a critical load-bearing civil mechanism subject to combined flexural bending, local torsional buckling, and dynamic seismic ground acceleration. As an authoritative OEM/ODM supplier operating a certified 30,000 m² factory campus since 2001, Guangzhou Heda Shelves Co., Ltd. integrates full-lifecycle metallurgical precision and automated roll-forming technologies to eliminate structural deflection risks and optimize landed cost per pallet position.
Core Structural Standard Compliance: All manufactured racking sections comply with European Standard EN 15512 (Steel Static Storage Systems: Adjustable Pallet Racking Systems - Principles for Structural Design), FEM 10.2.02, and US RMI MH16.1 specifications, verified by rigorous third-party testing with full mill traceability.
The structural longevity and load integrity of industrial pallet racks depend on the base steel microstructure. Our factory utilizes high-grade, continuous cast strip steel sourced from certified prime domestic mills. For standard ambient selective setups, high-ductility Q235B carbon structural steel (nominal yield strength $f_y = 235 \text{ MPa}$, elongation $\ge 26\%$) delivers balanced elasticity and energy absorption under accidental forklift impacts. For high-bay rack structures exceeding 12 meters, automated crane AS/RS configurations, and heavy cantilever arms handling upwards of 3,000 kg, we specify low-alloy high-strength Q355B (yield strength $f_y = 355 \text{ MPa}$). This reduces structural self-weight while guaranteeing safety factors against local flange buckling under maximum allowable dead-plus-live loading.
Every structural upright, box beam, and bracing channel manufactured in our Guangzhou production complex passes through a rigidly monitored 10-stage quality-assured process:
Stage 1 to 5: Cold-Forming & High-Tolerance Punching. Raw coils undergo automated decoiling and high-precision CNC slitting to sub-millimeter tolerances. Continuous multi-station roll-forming lines bend profiles via progressive roller passes (up to 24 roll-stands) to produce omega-shaped upright columns with internal stiffening ribs without introducing micro-cracking along bend radii. Fully automated hydraulic punching dies deliver accurate 50mm, 75mm, or 76.2mm hole patterns to ensure rigid hook-pin engagement.
Stage 6 to 10: Structural Welding & Multi-Stage Surface Treatment. Interlocking beam-end connectors are welded onto box beams using robotic dual-head CO2/Argon shielded arc welding machines, providing uniform penetration depth without heat-induced camber. Components enter an 8-stage pre-treatment line featuring acid pickling, multi-stage water rinsing, zinc phosphating, and de-ionized surface sealing to remove all mill scale and grease. Finished components receive an automated electrostatic polyester powder coat cured at 200°C for 25 minutes, creating a cross-linked coating film (thickness 60–90 microns) resistant to scratch damage, chemical vapors, and humid coastal salinity.
Selecting the optimal pallet racking configuration requires cross-referencing pallet selectivity against warehouse spatial cube utilization, material handling fleet kinematics, and picking cycles. Review our engineering comparison below:
| Storage System Type | Direct Selectivity | Floor Cube Utilization | Inventory Rotation | Typical Forklift Interface | Capital Cost Index |
|---|---|---|---|---|---|
| Selective Pallet Racking | 100% (Instant Access) | 35% - 45% | FIFO / LIFO Flexible | Counterbalance, Reach Truck | Baseline (Low) |
| Double Deep Racking | 50% (Two-Deep Pallets) | 50% - 60% | LIFO | Deep-Reach Pantograph Truck | Low - Moderate |
| Drive-In / Drive-Through | Single Lane Access | 65% - 75% | LIFO (Drive-In) / FIFO | Counterbalance, Narrow Chassis | Moderate |
| Push-Back Cart Racking | Lane Facing (2-6 Deep) | 60% - 70% | LIFO | Standard Reach / Counterbalance | Moderate - High |
| Radio Shuttle Automation | Lane Facing (Deep Lane) | 75% - 85% | FIFO & LIFO Software Controlled | Standard Forklift + Radio Shuttles | Moderate - High |
| Very Narrow Aisle (VNA) | 100% (Direct Access) | 55% - 65% | FIFO / LIFO Flexible | Wire/Rail Guided VNA Man-Up Turret | Moderate |
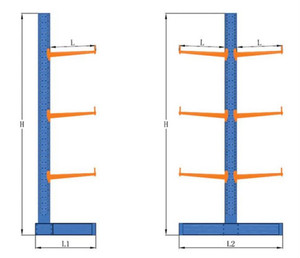
| Heavy Duty Cantilever | 100% Open Horizontal Face | Variable (Long Goods) | Batch / Random Access | Side Loader, Multi-Directional Truck | Moderate |
Global supply chain volatility, urban real estate appreciation, and accelerated logistics automation have radically altered pallet rack procurement methodologies. Engineering buyers are moving away from commodity steel tenders toward total cost of ownership (TCO) life-cycle assessments, seismic compliance verification, and future-ready automation modularity.
Procurement teams demand racking upright profiles that integrate floor-level Autonomous Mobile Robot (AMR) drop stations and upper-level Semi-Automated Radio Shuttle carriers without requiring complete system redesigns.
With refrigerated warehouse power costs spiking globally, procurement is prioritizing high-density Drive-In and Pallet Flow setups that cut conditioned cubic volume per pallet position by over 40% compared to wide aisles.
Specifiers in emerging logistics centers across South Asia, the Middle East, and Latin America mandate finite element seismic verification matching specific local ground acceleration coefficients ($S_s, S_1$).
Rising ocean freight makes nesting density paramount. Standardized bundle configurations packed with steel dunnage allow upwards of 26 to 28 tons net weight per 40ft High Cube container without transit abrasion.
Operating from our integrated manufacturing facilities in Guangzhou, Guangdong, Guangzhou Heda Shelves Co., Ltd. provides comprehensive engineering, structural customization, and high-volume containerized fulfillment for global distributors.
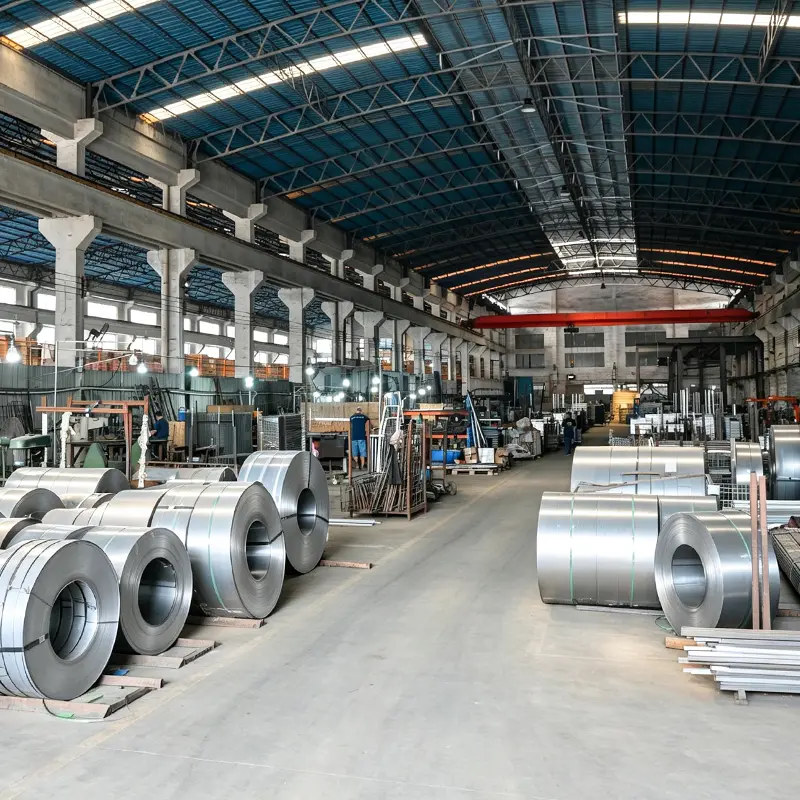
Founded in 2001, we possess deep engineering knowledge spanning warehouse layouts, logistics flow modeling, and steel structures for automotive, chemical, pharmaceutical, and 3PL distribution centers.
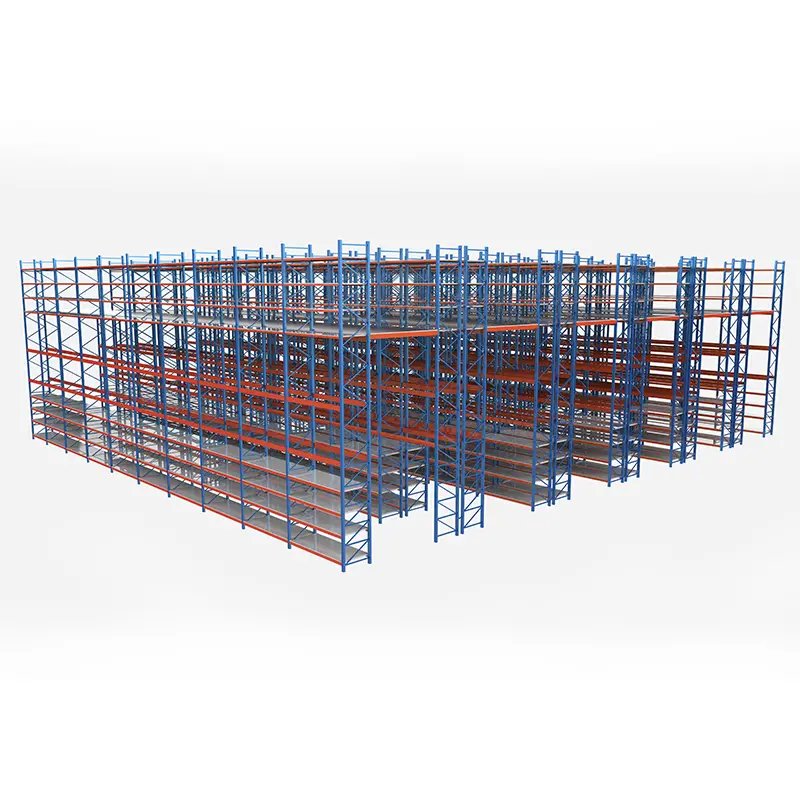
Our in-house design engineering department generates full 2D architectural warehouse layouts, 3D structural perspective renderings, and load capacity tables within 24–48 hours upon receiving warehouse drawings.
Rigorous quality tracking backed by official CE Certificate (No. 2435-CPR-8605159) and ISO 9001:2015 Quality Management System Certification (No. 18624Q00169R0M). Every batch is stamped for safety trace integrity.
Get answers to critical technical questions regarding steel grade certifications, corrosion resistance, floor slab loadings, and containerized ocean shipping.
Connect directly with our senior racking structural engineering team. Submit your warehouse floor plan today for a complimentary CAD layout, beam deflection calculation, and container-optimized CIF price schedule.