25+ Years
Engineering Since 2001
30,000 m²
Smart Factory Footprint
30,000 T
Monthly Output Capacity
ISO & CE
Audited European Compliance
Heavy-Duty Warehouse Solutions
High-Density Pallet Racks & Dynamic Live Storage Systems
Manufactured strictly in accordance with FEM 10.2.02 and EN 15512 standards. Explore our precision-engineered core industrial racking systems deployed across 120+ international markets.
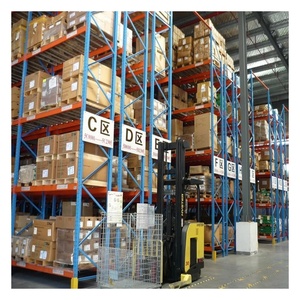
Physics of Gravity Flow
Precision Dynamics: Calculating Inertia, Braking & Ramp Gradient
Warehouse roller racking—also recognized across industrial engineering as gravity flow racking, pallet live storage, or carton flow beds—operates on an unpowered, kinetic incline principle that cuts internal transit time by up to 60%.
Unlike static cantilever or standard selective pallet racks, engineering a reliable roller rack system demands an exact equilibrium between friction, load mass, and deceleration kinetics. As a certified Chinese wholesale manufacturer, Guangzhou HEDA Shelves Co., Ltd. calculates track slope angles (strictly between 2.5° to 4.0°) governed by the mathematical relation:
tan(θ) > μstatic | Safe Controlled Velocity: v = √(2 · g · s · (sin θ - μk cos θ))
When handling pallet payloads exceeding 1,200 kg across high-depth lanes (up to 20 pallets deep), runaway inertia represents a major operational hazard. HEDA integrates heavy-duty centrifugal magnetic brake rollers spaced precisely at every pallet position, ensuring smooth, non-impact terminal arrival against our spring-loaded safety separators.
- Separation Mechanism at Discharge: Auto-locking pallet stop isolates the lead pallet from subsequent rear pressure, enabling 100% stress-free forklift extraction.
- Dual-Flanged & Cylindrical Rollers: Cold-drawn galvanized carbon steel rollers equipped with precision 6204-2RS sealed bearings for friction-free movement.
- High Modulus Cold-Formed Uprights: High-tensile Q235B / Q355B steel omega-profile columns roll-formed with a continuous 50mm / 75mm pitch matrix.
Kinetic Flow Engineering Matrix
| Component Parameter | Carton Live Flow | Heavy Pallet Flow |
|---|---|---|
| Target Unit Weight | 5 kg – 35 kg / Box | 300 kg – 2,500 kg / Pallet |
| Standard Incline Gradient | 3.0% – 5.5% (1.7° – 3.2°) | 3.5% – 4.5% (2.0° – 2.6°) |
| Roller Track Pitch | 28mm – 50mm Poly/Alu | 100mm – 150mm Steel Tube |
| Velocity Dampening | Integrated Guide Rails | Centrifugal Gear/Magnetic Brake |
| Rotation Philosophy | Strict FIFO (First-In, First-Out) | Strict FIFO / Buffering |
| Surface Protection | Electrostatic Polymer 80μm | Hot-Dip Galv. / Epoxy Powder |
Structural Compliance Note: Every roller track beam and dynamic frame is structurally checked via Finite Element Analysis (FEA) to eliminate longitudinal frame racking and localized beam torsion under dynamic cycling.
Strategic Market Intelligence
Next-Generation Procurement Trends for Warehouse Roller Racks
Global supply chains are re-engineering facility layouts for automated throughput and nearshore resilience. Here is how enterprise racking procurement is evolving toward 2030.
Autonomous AMR & AGV Integration
Procurement is pivoting from forklift-loaded static racks toward automated roller beds equipped with end-stop sensor triggers and optical beacons that synchronize directly with Autonomous Mobile Robots (AMRs) for lights-out material replenishment.
Zinc-Aluminum-Magnesium (ZAM) Coatings
Where cold chain condensation and tropical monsoon moisture destroy conventional hot-rolled steel, buyers now mandate ZAM-alloy treated roll surfaces and hot-dip galvanized uprights delivering up to 30 years of salt-spray corrosion immunity without degradation.
Modular Split-Roller Adaptability
The rise of erratic SKU footprints has rendered single-width roller beds obsolete. Modern multi-tier picking configurations utilize modular drop-in split-roller wheel tracks that allow warehouse managers to adjust lane widths in minutes without tools.
Total Cost of Ownership (TCO) Prioritization
Leading supply chain directors evaluate bids not by landed FOB steel cost alone, but by total cubic meter utilization. Gravity roller beds achieve a footprint savings ratio 45% superior to standard selective racking, delivering full CAPEX payback inside 18 months.
Architectural Selection Guide
Engineering Comparison: Roller Beds vs. High-Density Racking
Evaluate mechanical parameters, aisle requirements, rotation efficiency, and cost ratios across major warehouse structural typologies before final equipment specification.
| Storage System Type | Pallet Accessibility | Volumetric Space Density | Inventory Flow Mode | Standard Safe Load Rating | Primary Industrial Sector |
|---|---|---|---|---|---|
| Gravity Pallet Roller Racks | 1 Pallet Face per Lane | Extreme (Up to 85% Floor Ratio) | Strict FIFO (Gravity Incline) | 500 – 2,500 kg / Pallet | Cold Storage, Dairy, Fast FMCG |
| Dynamic Carton Flow Shelving | Multi-Lane Split Track | High (Dense Picking Surface) | Strict FIFO (Roller Run) | 30 – 100 kg / Sub-divider | E-Commerce, Automotive Parts, Pharma |
| Push-Back Nested Cart Racks | Single Aisle Loading Face | High (2 to 6 Pallets Deep) | LIFO (Last-In, First-Out) | 1,000 – 1,500 kg / Position | Buffer Storage, Dry Grocery Warehouses |
| Heavy Duty Selective Pallet Rack | 100% Immediate Direct Access | Moderate (35% - 40% Floor Ratio) | Random / Batch Access | 1,000 – 4,000 kg / Beam Pair | General 3PL, Raw Materials, Retail Hubs |
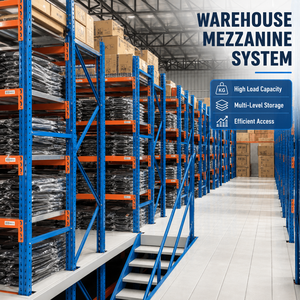
| Rack-Supported Mezzanines | Integrated Multi-Level Floors | Maximum Vertical Clearance | Hybrid Manual / Conveyor | 300 – 1,200 kg / m² Floor Area | Apparel, Small Parts, Distribution Hubs |
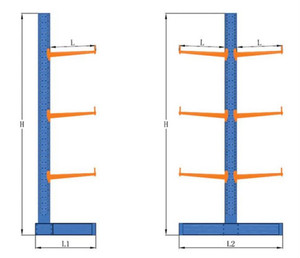
| Heavy Industrial Cantilever | Full Longitudinal Access | High For Long Loads | Direct Crane / Forklift Pick | 1,000 – 3,000 kg / Supporting Arm | Steel Pipe, Aluminum Profiles, Timber |
*All dynamic gravity roller tracks and structural upright capacities are calculated compliant with AS4084-2023, RMI (MH16.1), and European EN 15512 safety load factors.
Guangzhou HEDA Shelves Co., Ltd.
Why Tier-1 Importers Partner with Our Manufacturing Facility
With an active export footprint in more than 120 nations, Guangzhou Heda Shelves Co., Ltd. controls the complete engineering chain in-house—from cold strip coil slitting to automated 12-stage chemical surface conversion.
25+ Years of Dedicated Cold-Roll Forming
Founded in 2001, our 30,000 m² modern manufacturing complex houses 16 automated high-speed roll forming lines, continuous CNC punching presses, and robotic GMAW welding cells capable of outputting 30,000 tons of structural steel storage members every month.
8-Stage Pickling & Phosphating Pretreatment
Coating adherence failures in humid environments stem from poor chemical prep. HEDA executes continuous immersion pickling and phosphating to eliminate micro-scale mill scale before curing lead-free polyester-epoxy powder at 200°C, exceeding 500 hours of continuous salt-spray testing.
Full Regulatory Compliance & Verifiable Audits
Our plant operates under certified ISO 9001:2015 Quality Management standards (Cert No. 18624Q00169R0M) alongside European CE Machinery/Structural compliance (No. 2435-CPR-8605159). Container loading inspection, mill test certs (MTRs), and torque testing reports accompany every export bill of lading.
Standard Export Workflow to Major Ports
Direct container dispatch from South China ports (Nansha, Huangpu, Shenzhen) with scheduled intermodal transits to major global logistics gateways:
⚓ Nhava Sheva (JNPT) / Mundra
⚓ Chattogram / Kolkata
⚓ Colombo / Port Qasim
⚓ Hamburg / Rotterdam / L.A.
01
Data & Pallet Analysis
We review your clear ceiling height, slab thickness, pallet dimensions (1200x1000, 1200x800), and SKU throughput velocity.
02
3D CAD & FEA Layout
Our engineering division produces full 2D architectural placement drawings, aisle calculations, and 3D operational renders within 24 hours.
03
Precision Factory Run
CNC slitting, roll-forming, punching, welding, and 8-stage powder coating with batch traceability on every steel profile.
04
Crated Packing & Transit
Bundled with steel strapping, non-scratch geotextile wrapping, and containerized bracing engineered for long ocean voyages.
Application Scenarios
Tailored Roller Racking for Specialized Global Industries
Dynamic storage demands custom configurations depending on package rigidness, ambient temperatures, and turnaround cycles.
Cold Chain & Frozen Food (-30°C)
Refrigerated space is energy-intensive. By replacing static aisles with high-density gravity roller lanes, cold stores increase pallet storage capacity by up to 55%. We supply specialized low-temperature bearing lubricants and galvanized roller sleeves that prevent frost bonding.
Automotive Assembly Kanban
Assembly line workstations require steady component delivery without pallet stackers clogging aisles. Our carton flow roller beds interface directly with Kanban bin systems, gravity-feeding heavy fasteners, mechanical kits, and stamping modules straight to picking personnel.
Fast-Moving E-Commerce Fulfillment
For high-turnover multi-SKU sorting distribution centers, HEDA builds multi-tiered pick-tower mezzanines integrating live carton flow beds with directional picking LEDs, cutting picker travel distance and guaranteeing absolute batch expiration compliance.
Procurement Due Diligence
Frequently Asked Questions on Warehouse Roller Racks
Clear, unvarnished engineering answers to help purchasing officers, operations directors, and logistics consultants make fully informed purchasing decisions.
How do you calculate the optimal slope angle for gravity flow racks?
Standard pallet flow racks run at an incline between 3.5% and 4.0% (approximately 2° to 2.5°), whereas lightweight carton flow beds require 4.0% to 5.5%. Before manufacturing, our testing center performs run-off tests with your actual pallet bases (wood, HDPE plastic, or steel perimeter bases) to measure deflection and determine precise pitch intervals.
What prevents pallets from jamming or colliding in deep lanes?
We install calibrated magnetic or gear-driven centrifugal brake rollers that automatically throttle rolling speed to under 0.3 meters per second regardless of pallet weight. Additionally, mechanical pallet separators hold back the entire queue until the discharge operator safely lifts and clears the lead pallet.
Can weak or broken bottom wooden pallets operate on roller racks?
Pallet flow systems rely on a rigid bottom surface. Weak or fractured boards can catch on roller gaps. For facilities operating mixed or lower-grade disposable pallets, HEDA engineers high-density full-width twin-roller tracks or provides drop-in galvanized wire mesh guidance trays to ensure clean rolling performance.
What is the standard manufacturing and shipping lead time?
Standard engineering design and structural calculations take 2 to 3 days. Production across our 30,000 m² factory runs 15 to 25 days depending on total project tonnage (e.g., 2 to 8 40HQ containers). Transit times from Guangzhou/Shenzhen to South Asia ports average 10–18 days, and to Europe/US West Coast 22–32 days.
Do you supply installation blueprints and on-site assembly supervision?
Every container shipment includes an itemized, color-coded CAD assembly guide with numbered components corresponding directly to the packing manifest. We supply step-by-step video installation tutorials, and upon request, can dispatch an experienced site engineer to supervise local contractor teams for multi-tier mezzanine and high-bay projects.
How does HEDA guarantee steel quality and anti-corrosion life?
All raw material coils are procured directly from certified tier-one state mills (such as Baosteel and Shougang) with verified mechanical yield strength exceeding 235–355 MPa. In-house salt spray testing verifies that our electrostatic epoxy-powder coating delivers exceptional corrosion protection even in coastal or high-humidity monsoon regions.