Featured Tall Warehouse Storage Systems
Our vertically integrated manufacturing facility in Guangzhou fabricates heavy-duty, high-tolerance racking structural profiles designed to meet international EN 15512, FEM 10.2.02, and RMI standards. Explore the core systems driving automated and semi-automated vertical warehousing worldwide.
Roller Track Gravity Flow Rack System Brackets
Heavy-duty cold-formed gravity flow brackets and precision skate wheel assemblies engineered for dynamic FIFO live pallet lanes with integrated speed controllers.
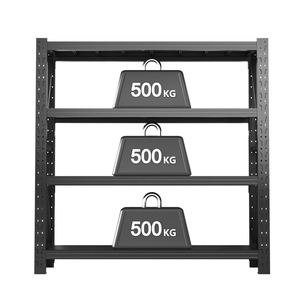
Heavy Duty Steel Shelving Rack 500kg Layer Load
Multi-tier industrial longspan storage engineered with interlocking stepped beams and rigid steel shelf decking for heavy manual picking and intermediate e-commerce bays.
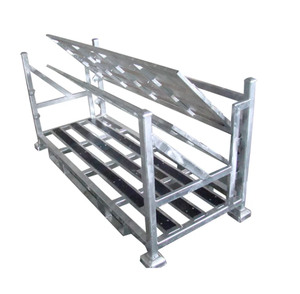
Stackable Steel Auto Parts Storage Rack & Bin
Reinforced post-pallet containers featuring flip-top accessibility and electro-galvanized rust barriers for heavy auto body stamping and sub-assembly logistical storage.
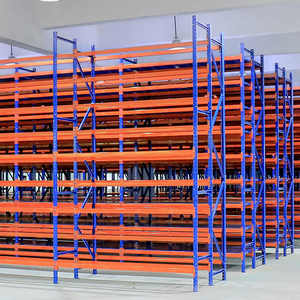
Heavy Duty Warehouse Steel Shelving System
Universal structural commercial warehouse framework optimized for high cubic volume consolidation, variable pitch adjustments, and heavy boxed inventory sorting.
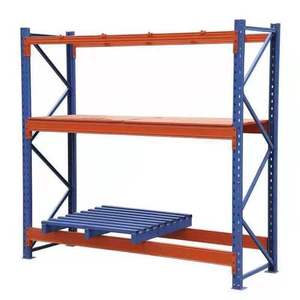
Adjustable Pallet Rack Heavy Duty Storage Racking
Continuous vertical uprights with 75mm/50mm adjustment pitches, high-tensile 3-4 claw connectors, and safety locks preventing accidental dislodgement under forklift impact.
Customized 3-Layer Heavy Duty Mezzanine Platform
Full-height cubic space multi-tier platform built on cold-rolled steel columns. Triples usable footprint without structural modifications to warehouse civil walls.
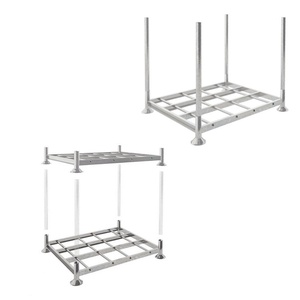
Detachable Vertical Stillage Pallet Storage Rack
Demountable steel post stillage bins engineered for seasonal warehouse surges, tire distribution yards, cold-store cross-docking, and nested freight returns.
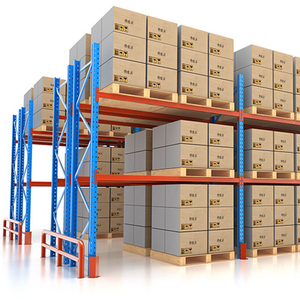
Selective Pallet Racks (Single & Double Deep)
World standard high-bay selective racking with certified anti-corrosion finishes. Accommodates European, ISO, and Australian pallet footprints with wide aisle or VNA layouts.
Tall Warehouse Racking Architectural Comparison
Selecting the ideal high-bay storage configuration requires evaluating SKU volatility, equipment aisle dimensions, floor slab load capacity, and capital expenditure versus volumetric density.
| System Architecture | Max Elevation | Aisle Clear Width | Pallet Selectivity | Floor Footprint Utilization | Handling Equipment Class |
|---|---|---|---|---|---|
| Selective Pallet Racking | Up to 12.5 meters | 3,000 – 3,500 mm | 40% – 45% | Counterbalance / Reach Truck | |
| Very Narrow Aisle (VNA) | Up to 18.0 meters | 1,600 – 1,900 mm | 60% – 68% | VNA Turret Truck / Inductive Wire | |
| Radio Shuttle Racking | Up to 24.0 meters | Lane Dependent | 75% – 85% | Automated Carrier + Reach Forklift | |
| Drive-In / Drive-Through | Up to 11.0 meters | Forklift Channel | 65% – 75% | Standard Counterbalance Truck | |
| Clad-Rack High-Bay (AS/RS) | Up to 40.0+ meters | 1,450 – 1,600 mm | 85% – 92% | Stacker Cranes (SRM) / AMR Satellites |
Future Procurement Trends in High-Bay Warehouse Racking
As industrial land prices escalate and robotic automation replaces conventional manual material handling, global supply chain directors must anticipate technical shifts before investing in multi-decade steel infrastructure.
Vertical Expansion: 12m to 30m+ High-Bay Clearances
Constrained metropolitan zoning and rising land premiums across North America, Europe, and Asia-Pacific are making 8-meter to 10-meter facilities economically non-viable. Modern mega-fulfillment hubs are standardizing on 18m to 35m clear heights.
This requires upright columns cold-formed from high-yield Q355B or European S355 steel with micro-deflection tolerances to prevent cumulative harmonic oscillation when high-reach turret masts or crane mast guides operate at speed.
- FEM 9.831 / EN 15620 class 100-200 alignment
- Seismic base plate anchoring up to 40mm thickness
ASRS & Autonomous Mobile Robot (AMR) Convergence
Racking is no longer static metal shelving; it has become the physical chassis for automated logistics. Forklift-only facilities are migrating to semi-automated radio shuttle pallets and fully automated 4-way shuttle systems.
Racking profiles now require precision-machined guide rails, integrated optical positioning reflectors, and laser-aligned guide channels that accommodate 4-way multidirectional shuttles capable of traversing vertical elevators without operator intervention.
- Millimeter-precise beam deflection ratios ≤ L/300
- Power buss-bar integration inside upright bays
Eco-Coating, Coastal Durability & Cold Chain Resiliency
Global pharmaceutical and deep-freeze logistics (-30°C) demand specialized surface metallurgy. Traditional zinc-plated hardware is rapidly being replaced by continuous hot-dip pre-galvanized coils or multi-stage nano-ceramic conversion coatings.
Heavy epoxy powder coatings certified for zero VOC emission, low humidity degradation, and resistance to aggressive condensation cycles are now standard contract stipulations among multinational 3PL operators and chemical distributors.
- ISO 12944 C3 to C5 industrial anti-corrosion classes
- Low-temperature brittle fracture structural tests (-40°C)
Why Global Supply Chains Partner With Guangzhou Heda Shelves
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into one of China's premier tall warehouse racking exporters, managing full lifecycle design, robotic roll-forming, global freight packing, and localized commissioning.
25+ Years Production Depth
Over two decades of precision metallurgical engineering across food, automotive, chemicals, retail, and third-party logistics. More than 10,000 automated high-bay warehouse projects successfully delivered worldwide.
Full In-House Automation
Our 30,000 m² factory houses dedicated high-speed roll forming lines, robotic multi-point beam connector welders, automated 10-stage pickling and phosphating lines, and electrostatic powder booths producing 30,000 tons monthly.
Audited International Certifications
Fully certified under European Construction Products Regulation CE Mark No. 2435-CPR-8605159, certified ISO 9001:2015 Quality Management System No. 18624Q00169R0M, and verified RoHS environmental compliance.
Container-Optimized Sea Freight
Proprietary computer-modeled nesting and steel banding ensure maximum 40HQ container utilization (≥96% cubing efficiency). Components arrive safely at gateway ports including Rotterdam, Hamburg, Los Angeles, Nhava Sheva, and Jebel Ali.
10-Stage Precision Manufacturing Workflow
Structural safety in high-bay racking systems demands continuous metallurgical inspection and zero-tolerance fabrication at every stage of the production cycle.
Tall Warehouse Racking Procurement FAQ
Expert engineering answers to critical inquiries raised by warehouse architects, structural consultants, general contractors, and global supply chain directors.