High-Efficiency Warehouse Pallet Racking & Industrial Steel Shelving
Explore our export-certified heavy duty pallet racks, structural angle shelving, automated shuttle tracks, and boltless rivet configurations built to ISO 9001:2015 and European CE safety benchmarks.
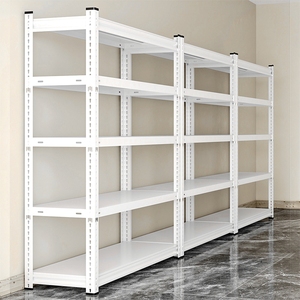 Heavy Duty
 Steel Storage Rack Adjustable Metal Shelving Warehouse Pallet Racking Corrosion Resistant Industrial Shelves
- Up to 5,000 kg / level capacity
- 75mm / 50mm pitch beam adjustment
- Phosphated anti-corrosion powder coat
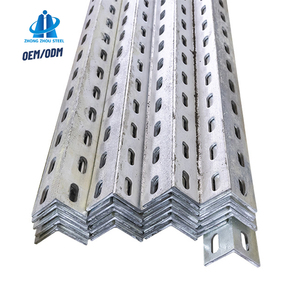 OEM Custom
Customized Heavy-Duty Slotted Angle Rack Fast Delivery Steel and Carbon Metal Building Materials at Manufacturer's Price
- Q235B cold-rolled carbon steel
- Modular rapid-cut punched holes
- Cost-effective workshop shelving
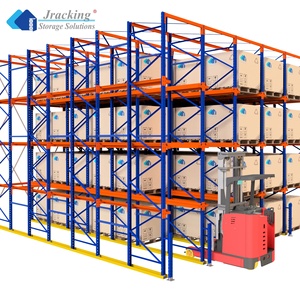 CE Certified
Warehouse Heavy Duty Industrial Shelves Steel EU Blue and Orange Selective Pallet Racking Shelving System CE Certified
- 100% pallet selectivity access
- Classic RAL5015 blue & RAL2004 orange
- Compliant with EN 15512 safety code
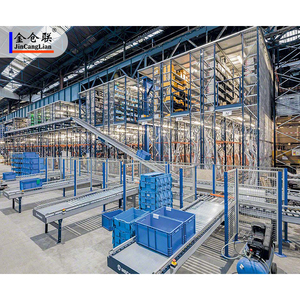 Automated
Express System Remote Control with Shuttle Car Radio Shuttle Robot Pallet Racking Shelves Narrow Intelligent Warehouse Shelving
- High-density semi-automated deep lane
- FIFO & LIFO software control mode
- -25°C cold storage certified vehicle
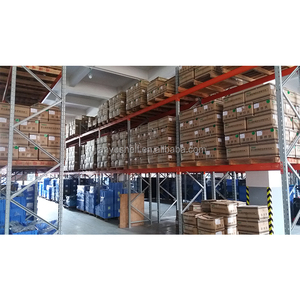 Commercial
 Industrial Storage Rack System Heavy Duty Pallet Warehouse Solution
- Heavy box-beam locking safety design
- Seismic frame bracing calculation
- Suited for retail logistics & 3PL hubs
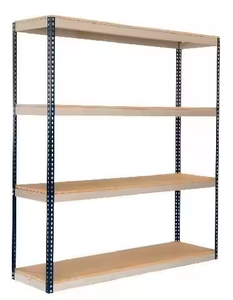 Light Duty
Good Quality Customized Size Light Duty Shelves Warehouse Rack System Steel Storage Shelving
- 100–300 kg / layer uniform load
- Fast assembly, boltless steel decking
- Ideal for e-commerce carton picking
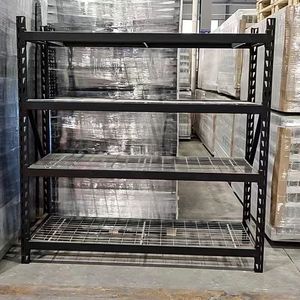 Medium Duty
Warehouse Racking System for Light Duty Pallet Storage | Industrial Metal Rack Corrosion Protection Selective Pallet Rack Carton
- Hybrid carton-flow & light pallet tiers
- Multi-level picking shelf integration
- Electrostatic spray scratch resistance
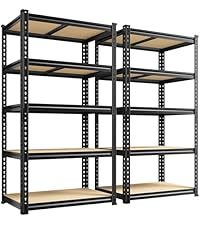 Boltless Rivet
5 Layer Industrial Storage Shelving Racks Heavy Duty Adjustable Boltless Rivet Rack Corrosion Protection Warehouse Powder Coated
- 5-Tier high rigidity rivet beam locking
- Steel wire mesh / MDF timber shelves
- Toolless installation in 10 minutes
Need Tailored Structural Engineering or Custom Racking Specifications?
Our engineering division produces comprehensive AutoCAD layout proposals, static finite element structural load calculations, and turnkey factory-direct price quotes within 24 hours.
Why Tier-1 Global Procurement Directs to HEDA Shelves
Established in 2001, Guangzhou Heda Shelves Co., Ltd. controls the end-to-end metallurgical engineering, roll-forming fabrication, and global logistics execution for over 10,000 warehouse projects across 120+ countries.
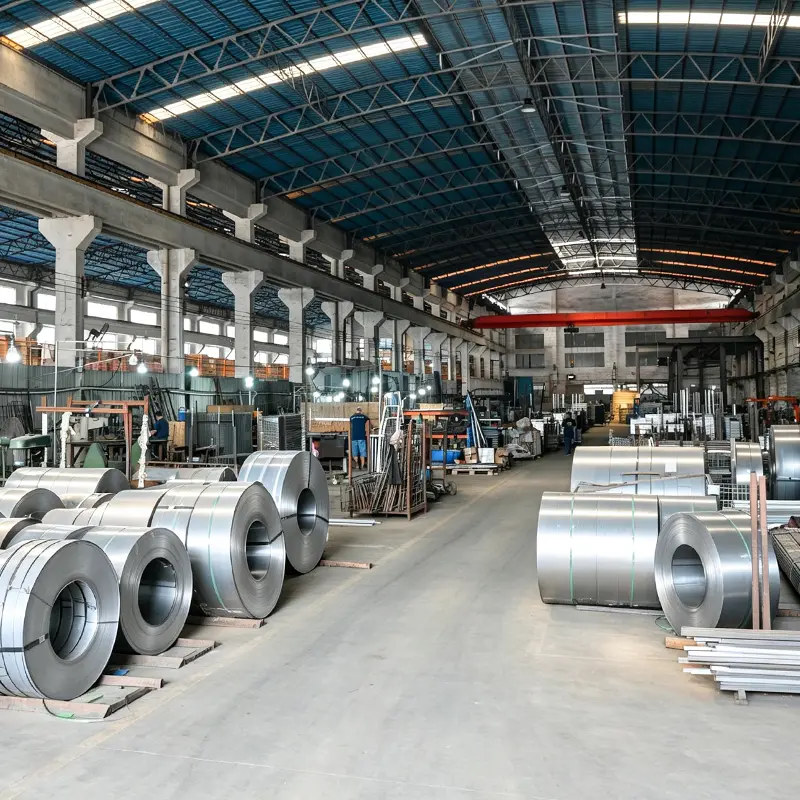
25+ Years Racking Expertise
Decades of deep metallurgical experience in cold-rolled structural steel, seismic base calculations, and multi-tier mezzanine engineering for food, chemical, automotive, and 3PL supply chains.
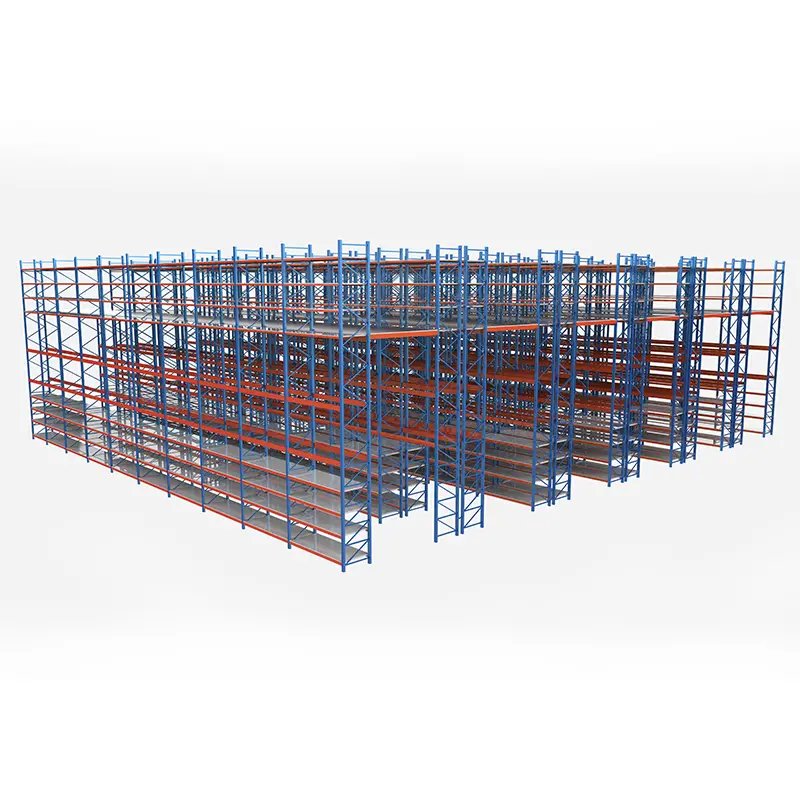
Complimentary 3D & CAD Design
Our senior structural engineers analyze aisle turning radii, reach truck clearances, and dead/live load deflection factors to render comprehensive AutoCAD blueprints and realistic 3D spatial simulations.
CE & ISO 9001:2015 Certified
Every beam, upright column, and row spacer is certified under CE No. 2435-CPR-8605159, ISO 9001:2015 Registration No. 18624Q00169R0M, and RoHS directives for absolute chemical and structural safety.
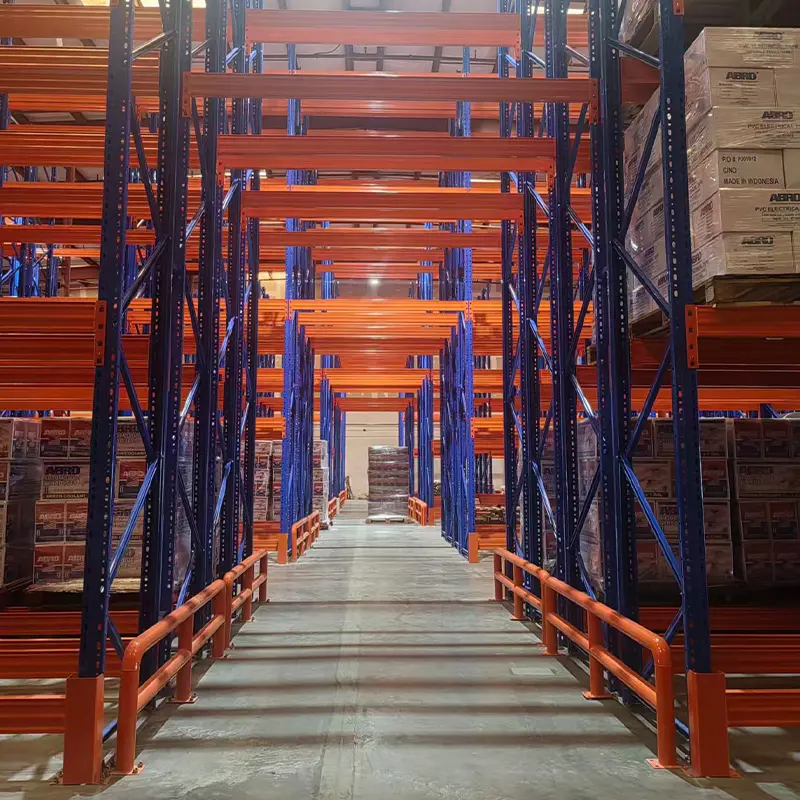
OEM/ODM Turnkey Customization
From custom beam gauges (1.5mm to 2.5mm) and non-standard punch pitches (50mm, 75mm, 76.2mm) to specialized RAL epoxy colors and heavy galvanized finishes for low-temperature cold rooms.
10-Stage Precision Manufacturing Workflow
Uncompromising quality control through end-to-end automated roll forming, robotic welding, and automated surface treatment.
 STEP 01
Certified Steel Coils
Strict mill inspection of Baosteel/Shougang Q235B & Q355B coils for yield strength.
 STEP 02
Precision CNC Slitting
High-speed uncoiling and strip slitting calibrated within ±0.1mm dimensional tolerance.
 STEP 03
Automated Pitch Punching
Continuous punch presses create exact teardrop or diamond beam locking slots.
 STEP 04
Cold Roll Forming
Multi-roller forming lines fold steel into rigid multi-rib omega column structures.
 STEP 05
Box-Beam Fabrication
Twin C-profile cold clamping produces maximum moment-resistant interlocked beams.
 STEP 06
Mechanical Deburring
Edge radiusing and robotic slag grinding prevent burrs and guarantee personnel safety.
 STEP 07
Robotic CO2 Shielded Welding
Full-penetration robotic welds fuse heavy beam connectors with zero spatter.
 STEP 08
9-Stage Pre-Treatment
Immersion degreasing, acid pickling, and phosphating create microscopic anti-rust bonds.
 STEP 09
Thermoset Powder Coating
Automated Swiss Gema guns apply 60–90µm epoxy polymer cured at 200°C.
 STEP 10
QC & Container Packing
Deflection testing, film wrapping, and timber-nested bundling maximize 40HQ loads.
Technical & Structural Development Trends in Pallet Racking
Modern warehousing is undergoing a paradigm shift driven by automated material handling, micro-fulfillment centers, high-yield metallurgical advances, and dynamic seismic engineering codes.
High-Yield Thin-Walled Microalloyed Steels
Traditional structural racking relied heavily on standard Q235 carbon steel profiles with thicker walls to compensate for buckling limits. Today's manufacturing centers around advanced microalloyed high-strength cold-formed steels like Q355B and high-yield cold-rolled coils with yield strengths exceeding 355 to 420 MPa.
Through finite element analysis (FEA) and specialized cold-roll forming, manufacturers produce complex omega column profiles featuring up to 12 distinct mechanical bends. This design optimizes the gyration radius and polar moment of inertia, reducing overall system deadweight by 14% to 18% while enhancing load capacity and resistance against torsional flexure.
- Omega geometry with interior stiffening ribs
- Higher strength-to-weight ratio cuts ocean freight tonnage
- Compliance with EN 15512:2020 limit state design
AS/RS & 4-Way Radio Shuttle Integration
The global push toward lights-out automation has transformed the physical requirements of steel racks. Racking is no longer merely a static shelving matrix; it now serves as high-precision track infrastructure for automated guided vehicles (AGVs), autonomous mobile robots (AMRs), and four-way radio shuttle buggies.
These dynamic systems demand tighter manufacturing tolerances: beam level deflections are restricted to L/300 or L/400 (compared to the historical L/200 standard for manual forklifts), and rail joint alignment deviations must stay under ±0.5mm across 100-meter deep lanes to avoid shuttle sensor errors and track binding.
- Integrated power-bus rail and optical target channels
- Cold-drawn galvanized guide rails with high coplanarity
- Floor expansion joint compensation for high-bay AS/RS
Seismic Performance & Ductility Engineering
Warehouses built across active seismic corridors require rigorous non-linear dynamic simulation. The latest design standards (Eurocode 3, RMI MH16.1, and AS 4084-2023) emphasize continuous energy-dissipating connections between the vertical column and the horizontal box beam.
State-of-the-art Chinese manufacturers employ multi-tang boltless connector brackets with heavy-duty cold-forged safety locking pins. Under seismic ground motion, these multi-tooth mechanical connections allow controlled cyclic micro-slip, safely absorbing ground acceleration energy rather than transferring brittle shear stresses directly into the anchor bolts or the concrete foundation.
- Dynamic cyclic test certification for beam-end connectors
- Oversized structural base plates with epoxy chemical anchoring
- Vertical diagonal X-bracing and horizontal portal ties
Future Procurement Trends for Pallet Racking & Industrial Shelves
A strategic breakdown for supply chain directors, procurement leads, and logistics facility developers looking to minimize Total Cost of Ownership (TCO) and avoid costly project delays.
Knock-Down Design & CBM Freight Optimization
With unpredictable international shipping rates, procurement teams evaluate racking manufacturers based on total landed cost rather than initial FOB factory gate pricing. Top Chinese factories utilize 100% bolted knock-down (KD) upright frames rather than fully welded upright trusses.
This approach allows structural columns, vertical bracing, and horizontal struts to pack flat into 40-foot High Cube (40HQ) maritime shipping containers. A single 40HQ container can accommodate up to 24 to 26 metric tons of knocked-down components—reducing ocean freight expenses per pallet position by 35% compared to pre-welded configurations.
- High-density steel banding with corner edge protectors
- Component-coded bundles aligned to installation zones
- Pre-calculated container weight-to-volume ratio optimization
Low-VOC Powder Coatings & Cold-Chain Finishes
Environmental policies (ESG compliance) and the rapid growth of refrigerated e-grocery cold storage have changed coating requirements. Standard single-coat paints crack and peel in -30°C freezer facilities, creating corrosion points from freeze-thaw condensation cycles.
Modern procurement guidelines demand automated zirconium or zinc-phosphate conversion pre-treatments followed by lead-free, heavy metal-free TGIC polyester or thermoset epoxy powders. For harsh exterior canopies or salty coastal locations, heavy-duty hot-dip galvanizing (HDG) per ISO 1461 with 85µm zinc thickness has become the preferred standard.
- Zero VOC electrostatic thermoset polymer deposition
- 500-hour to 1,000-hour salt spray endurance (ASTM B117)
- Flexibility retention under sub-zero freezer cycles
Factory Direct Engineering Transparency (E-E-A-T)
Global supply chains now bypass intermediate trading brokers, working directly with established production mills capable of providing transparent raw material traceability and verifiable structural load testing.
Experienced buyers require complete Mill Test Certificates (MTC) indicating carbon, manganese, and phosphorus levels for each master coil, alongside batch-specific third-party laboratory tensile reports and static load deflection verification under full design stress.
- Third-party SGS / TÜV load destructive test certificates
- Laser digital measurement validation of hole centers
- Complete traceability from steel heat number to site
| Racking Architecture | Optimal Load / Unit | Direct Selectivity | Floor Space Use | Primary Industrial Application | Compliance Standards |
|---|---|---|---|---|---|
| Selective Pallet Racking | 500 – 4,000 kg / level | 100% Immediate | 40% – 50% | General 3PL, FMCG multi-SKU hubs, retail distribution | CE, ISO 9001, EN 15512 |
| Radio Shuttle System | 1,000 – 2,000 kg / pallet | Lane-Selective (LIFO/FIFO) | Up to 85% Density | Frozen cold rooms, beverage processing, seasonal buffers | CE, Machinery Directive, ISO |
| Drive-In Racking | 800 – 1,800 kg / pallet | Low (Last-In, First-Out) | 70% – 80% | Raw material storage, grain/feed, bulk packaging lines | ISO 9001, RMI MH16.1 |
| Heavy Duty Slotted / Rivet | 150 – 800 kg / layer | 100% Hand Pick | 50% – 60% | Hardware, automotive workshops, garment sorting | RoHS, CE, Factory Standard |
| Multi-Tier Mezzanine | 300 – 1,000 kg / m² | Zoned Multi-Level | 200%–300% Area | Apparel e-commerce picking, pharma split-case packing | CE No. 2435-CPR, EN 1090 |
Frequently Asked Questions by Industrial Racking Buyers
In-depth answers addressing structural calculations, steel grades, international logistics, installation procedures, and quality compliance for global procurement professionals.
What structural steel grades are used, and how is certified load capacity validated?
Industrial pallet racking manufactured by Guangzhou Heda Shelves Co., Ltd. is fabricated primarily from premium Q235B and high-strength Q355B hot-rolled or cold-rolled strip steels from accredited mills like Baosteel. Structural load calculations follow European EN 15512 and FEM 10.2.02 codes. Capacities are calculated based on limit-state finite element analysis incorporating safety factors of 1.4 to 1.5 against beam yielding and 1.6 to 2.0 against column stability failure, verified through physical destructive load testing.
How do selective pallet racking, drive-in, and radio shuttle systems compare in ROI?
Selective pallet racking offers the lowest initial capital cost per pallet position and provides 100% direct access to every SKU, making it ideal for high-mix, fast-turnaround operations. Drive-in racking increases storage density by up to 75% by eliminating fork aisles, but is limited to LIFO rotation and carries higher risks of rack impact from forklifts. Radio shuttle systems require higher initial upfront capital for automated shuttle carts, but deliver the highest pallet density, support both FIFO and LIFO modes, eliminate forklift transit within the racks, cut labor travel times by 40%, and significantly reduce accidental frame damage.
What exact information is required to receive an accurate AutoCAD layout design?
To produce an optimized CAD proposal, our engineering team requires: (1) An architectural warehouse layout drawing in DWG or PDF showing interior column grids, building clear heights, fire sprinkler drop depths, doors, and dock locations; (2) Detailed pallet dimensions including width, depth, overall cargo height, and maximum gross weight per pallet; (3) Forklift model, turning radius, and maximum mast lift elevation; and (4) Facility operating temperature (ambient or sub-zero cold room) along with local seismic zone data.
How does HEDA Shelves protect steel racks from rust in humid or coastal environments?
Protection begins with an automated 9-stage surface treatment process that includes high-temperature immersion degreasing, clean-water rinses, acid pickling to eliminate mill scale, and a microcrystalline zinc-phosphate conversion coating. Components then receive an electrostatic thermosetting polyester-epoxy powder coating cured at 180°C to 200°C, producing a dense 60–90µm dry film thickness. For open sheds, high-humidity port terminals, or sub-zero freezer warehouses, hot-dip galvanizing per ISO 1461 is available, providing a sacrificial zinc layer exceeding 85µm for decade-long rust resistance.
What certifications does HEDA Shelves hold for international import compliance?
HEDA Shelves operates under a verified ISO 9001:2015 Quality Management System (Certificate Registration No. 18624Q00169R0M) and holds European CE conformity certification No. 2435-CPR-8605159, permitting structural steel racking installations across EU member states. Additionally, all electrostatic powder coating materials are RoHS compliant, verifying the absence of lead, cadmium, mercury, and toxic polybrominated compounds. Documentation packs include Mill Test Certificates (EN 10204 Type 3.1) and container loading manifests for clean customs processing.
How are heavy steel racking components packaged to prevent damage during ocean transit?
All upright columns and long beams are organized into tight bundles using high-tensile steel straps, supported by structural wooden dunnage blocks and heavy edge protector channels. Every bundle is wrapped in water-resistant plastic stretch film and reinforced with lifting slings for forklift and crane handling at the destination port. Small hardware items such as base plates, anchor bolts, beam locking pins, and row spacers are packed in double-walled corrugated cartons secured onto fumigated wooden export pallets.
Can local installation teams erect the racking, and is engineering support provided?
Yes. Approximately 85% of our international clients utilize local mechanical or material handling contractors for installation. To facilitate smooth on-site assembly, HEDA Shelves provides comprehensive installation packages that include color-coded layout schematics, component placement schedules, bolt torque specifications, and step-by-step 3D assembly videos. For complex automated shuttle systems, multi-tier mezzanine floors, or large-scale distribution centers, our senior engineers are available for on-site supervision, laser alignment inspection, and commissioning.
What is the typical production lead time and payment term structure?
Standard production lead times for standard selective pallet racking and slotted shelving systems range from 15 to 25 calendar days for a 2 to 5 container (40HQ) order. Highly customized solutions, specialized colors, automated radio shuttle runs, or hot-dip galvanized finishes typically require 25 to 35 days. Payment terms generally operate on a 30% T/T deposit upon engineering drawing confirmation, with the remaining 70% balance payable against the Bill of Lading (B/L) copy, or via an Irrevocable Letter of Credit (L/C) at sight.