Heavy Duty
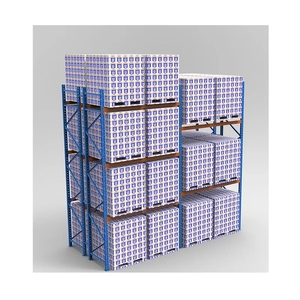
Heavy Duty Industrial Shelving Stacking Pallet Racking
Q235B Steel50/75mm PitchCE Certified
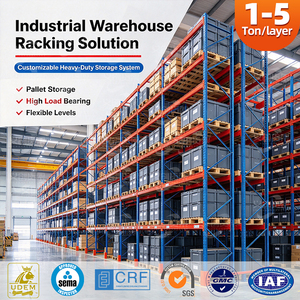
Engineered to FEM, RMI, and ISO 9001 standards, our heavy-duty wide span and selective systems deliver maximum volumetric density, load integrity up to 4,500 kg per beam level, and rapid supply chain turnover.
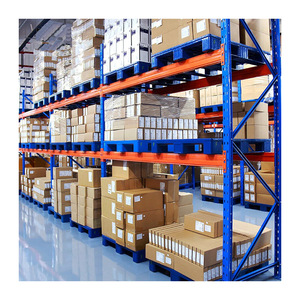
Combining continuous cold-roll forming, robotic laser cutting, and full-immersion surface pre-treatment across a 30,000 m² smart production base in Guangzhou, China.
We source prime cold-rolled coils exclusively from top-tier state mills (Baosteel/Shougang). Our Q235B and Q355B steels undergo rigorous tensile and yield verifications to guarantee compliance with EN 15512:2020 and RMI MH16.1.
Our workshop houses multi-stage roll-forming lines capable of handling column profiles up to 120mm width and 2.5mm wall thickness without structural micro-fracturing. Automated CNC punching guarantees a ±0.5mm hole pitch tolerance.
Each profile undergoes a 10-stage preparation cycle: degreasing, ultrasonic acid pickling, zinc phosphating, and 180°C thermoset epoxy powder baking. Packed with protective honeycomb dunnage for maximum 40HQ container load factor.
As modern distribution centres migrate toward hyper-automation, seismic resilience, and ESG compliance, the criteria for selecting wide pallet racking have transformed fundamentally.
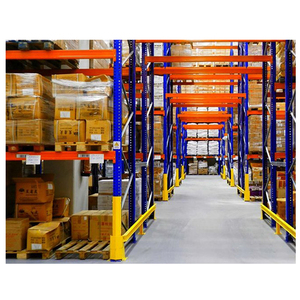
Traditional static wide pallet racks are giving way to hybrid architectures that interface directly with Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). Warehouses demand widened bottom-tier clearance, ground guidance channels, and ultra-flat floor baseplate anchoring to ensure automated reach trucks operate at zero-tolerance deviations.
Procurement Shift: Strategic buyers increasingly audit deflection ratings under dynamic robotic picking velocities rather than solely resting static loads.
With real estate and energy costs soaring in frozen food, pharmaceutical, and perishables sectors, standard selective layouts are actively replaced by deep-lane Radio Shuttle racks. This maximizes cold air cubic volume, reduces refrigeration kilowatt-hours per pallet, and removes forklift travel inside sub-zero environments.
Procurement Shift: Sourcing specifications have shifted towards low-temperature certified steel alloys (-30°C impact test certified) with specialized cold-flow powder coatings.
Procurement directors are shifting focus from Initial Purchase Price (CapEx) to Total Cost of Ownership (TCO). This emphasizes high-yield, weight-optimized cold-formed sections that reduce shipping freight, combined with non-toxic, RoHS-compliant powder finishes that withstand coastal humidity and chemical fumes.
Procurement Shift: Demanding standardized teardrop or European hook configurations that allow modular reconfiguration and future expansion without discarding existing upright frames.
| Storage Architecture | Pallet Accessibility | Volumetric Density | MHE Compatibility | Optimal Industry Application |
|---|---|---|---|---|
| Wide Span Selective Racking | 100% Direct Immediate | Moderate (35%–45%) | Standard Counterbalance, Reach Trucks | High-SKU 3PLs, Retail Fulfillment, FMCG Hubs |
| Double-Deep Pallet System | 50% Direct Access | High (55%–65%) | Pantograph Reach Trucks | Raw Materials, Intermediate Manufacturing Buffer |
| Semi-Automated Radio Shuttle | Batch / Lane Access | Maximum (75%–85%) | Standard Forklifts + Battery Shuttles | Cold Storage, Beverage, Seasonal Agri Consolidation |
| Rack-Supported Mezzanine | Multi-Level Manual & Pallet | Vertical Space Multiplier (200%) | Pallet Jacks, Vertical Cargo Lifts | E-commerce Split-Case Picking, Spare Parts Supply |
Key technical, logistic, and structural considerations addressed by our Senior Structural Engineering Team to streamline your direct China factory acquisition.
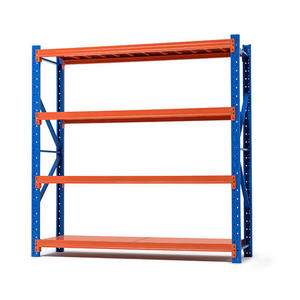
Our engineering calculations adhere strictly to FEM 10.2.02 and ANSI MH16.1. A minimum deflection limit of L/200 (length of beam divided by 200) is maintained under 100% full working load. For a typical 2,700mm beam bay accommodating two standard 1,200mm × 1,000mm pallets loaded at 1,500 kg each (3,000 kg total layer load), we engineer dual interlocking C-profile welded box beams (e.g., 120×50×1.5mm) with 3-claw or 4-claw stamped connectors secured with safety drop pins tested to resist an accidental vertical upward dislodgement of ≥ 5 kN.
To receive a free, certified CAD layout within 24 hours, buyers should provide: (1) Architectural DWG drawing highlighting structural building columns, fire exits, and overhead clear heights; (2) Concrete slab thickness, compressive rating (e.g., 25–30 MPa), and rebar reinforcement depth; (3) Pallet parameters including width, depth, height, and gross weight inclusive of wooden skid; (4) Material handling equipment (forklift turning radius, mast lowered/extended heights, and aisle tolerances).
We implement a military-grade automated pre-treatment line. Raw steel parts go through acid cleaning and immersion phosphating to eliminate micro-scale mill scale and oil, providing a reactive crystal matrix that bonds mechanically with electrostatic epoxy-polyester powder. The finished coating undergoes 500-hour neutral salt-spray chamber testing (ASTM B117) without cross-hatch blister formation. For container stowage, upright frames are nested with corrugated paper separation, steel band reinforcement, and vapor-corrosion-inhibitor (VCI) film coverings.
Yes. Over 85% of our overseas clients install our systems with local contractors. Every exported project includes: comprehensive 3D step-by-step erection schematics, component tags marked per bay and tier, baseplate anchor torque specs, and high-definition installation video walkthroughs. For enterprise-scale automation projects exceeding 5,000 pallet positions, we deploy bilingual structural supervisors directly to project sites across South Asia, the Middle East, Southeast Asia, and Europe.