High-Efficiency Warehouse Racking & Storage Portfolios
Engineered for rigorous industrial distribution hubs, manufacturing facilities, and heavy-duty fabrication environments requiring certified structural integrity.
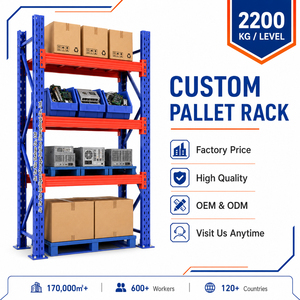
Heavy Duty Pallet Rack System 2200KG Per Level
High-capacity cold-rolled structural steel rack engineered for electronic hardware containers, battery packs, and dense plastic bin staging.
View Engineering Specs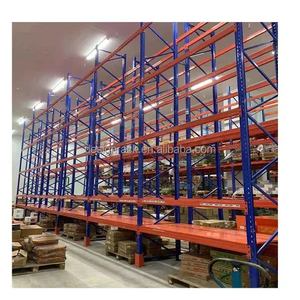
Industrial Metal Steel Single Deep Forklift Pallet Racks
100% direct pallet selectivity engineered for fast counterbalanced and reach truck navigation across multi-SKU retail and transit facilities.
View Engineering Specs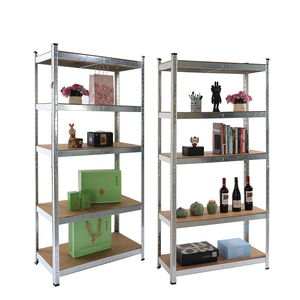
Light-to-Medium Duty Long Span Steel Storage Shelving
Modular boltless interlocking framework for split-case manual order picking, maintenance workshops, and high-frequency staging buffers.
View Engineering Specs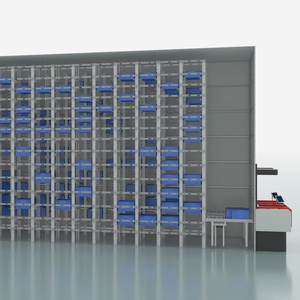
Factory-Direct Zinc Galvanized Smart Shelving 50kg/Deck
Corrosion-resistant zinc galvanized modular bays intended for precision assembly lines, small parts classification, and humid warehouse wings.
View Engineering Specs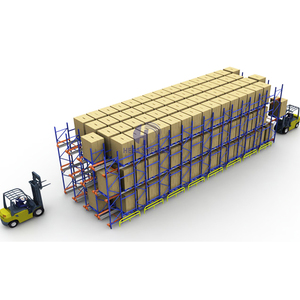
Automated Four-Way Radio Shuttle High-Density Racking
Next-generation automated storage and retrieval system (ASRS) running bi-directional radio shuttles for maximum cube utilization.
View Engineering Specs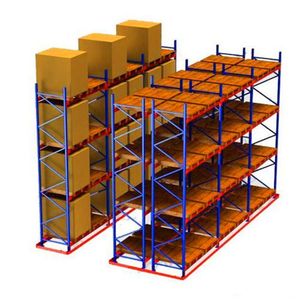
High Density Heavy Duty VNA (Very Narrow Aisle) Racks
Engineered for guided turret trucks to compress working aisle profiles down to 1.6 meters, maximizing structural vertical clearance.
View Engineering Specs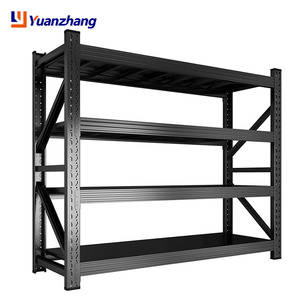
Industrial Metal Heavy Long Span Shelving Modular Set
Adjustable tier height storage engineered for industrial MRO maintenance cribs, automotive sub-assemblies, and carton distribution.
View Engineering Specs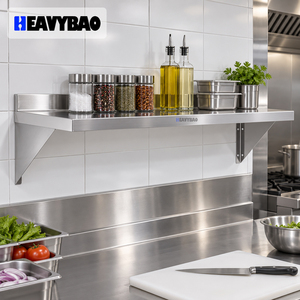
Commercial Heavy Duty Stainless Steel Sanitary Wall System
Brushed food-grade stainless steel storage modules designed for cold washdown kitchens, sanitary processing, and sterile lab storage.
View Engineering Specs30,000 m² Facility
Certified Guangzhou manufacturing plant delivering over 30,000 tons of structural steel storage equipment every month.
Audited CE & ISO
Strict structural adherence to CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 global quality benchmarks.
Direct OEM / ODM
Complete in-house roll forming, automated punching, weld testing, custom epoxy coating, and structural CAD optimization.
Global Port Logistics
Container-optimized bundle logistics servicing 120+ nations across Europe, the Americas, the Middle East, and South Asia.
Engineering Whitepaper: Specifying Industrial Cantilever Racking Systems
Cantilever racking systems are the benchmark engineering solution for facilities handling non-palletized, long-span, or irregularly dimensioned materials. Where standard selective racking is limited by front upright columns, cantilever designs use open front arms supported by robust vertical columns and heavy base structures. This open front architecture allows unimpeded horizontal access for oversized items such as structural steel I-beams, extruded aluminum, PVC tubing, industrial timber, sheet metal packs, and heavy plumbing fixtures.
As warehouse construction costs increase globally, operations managers must maximize vertical volume while retaining picking flexibility. Cantilever systems turn open floor layouts into organized vertical storage racks, reducing footprint congestion and keeping material damage to a minimum.
Structural Column and Cantilever Arm Engineering
Industrial cantilever racks rely on precise structural load distribution. The entire system is built on two primary structural configurations:
- Roll-Formed Cantilever Systems: Constructed from cold-rolled steel coils, these racks are cost-effective and versatile for light to medium-heavy applications (500 kg to 1,500 kg per arm level). They handle fluctuating inventory in retail hardware distribution, light carpentry storage, and plastic profile centers.
- Structural I-Beam (Hot-Rolled) Systems: Fabricated from structural hot-rolled H-beams and I-sections, these units are designed for severe-duty industrial applications (ranging from 1,500 kg to beyond 5,000 kg per arm). They provide exceptional impact resistance against industrial counterbalanced forklifts in steel fabrication yards, timber mills, and harsh outdoor yards.
| System Class | Material Construction | Capacity Per Arm | Access Configuration | Primary Industrial Sector |
|---|---|---|---|---|
| Light-Medium Cantilever | Cold-Rolled Q235B Steel | 300 kg – 1,000 kg | Single / Double Sided | Plastic Extrusions, Molding, Furniture |
| Heavy-Duty Cantilever | Heavy Roll-Formed Section | 1,000 kg – 2,500 kg | Single / Double Sided | Timber, Building Sheets, HVAC Ducting |
| Extra Heavy Structural | Hot-Rolled H/I Beams | 2,500 kg – 5,000+ kg | Single / Double Sided | Steel Coils, Rebar Bundles, Pipes, Rigging |
| Cantilever Mezzanines | Integrated Truss & Deck | Custom Dynamic Load | Multi-Level Walkway | E-commerce Split Picking, Heavy Auto Parts |
Technological Trends in Cantilever Storage & Future Procurement Dynamics
Procuring warehouse racking has evolved beyond simply looking at steel tonnage. Structural specifications now incorporate automated handling workflows, seismic compliance, and advanced coating treatments. Procurement professionals must plan for these operational shifts to maintain high return on capital over a 15 to 20-year operational life.
Integration with Guided Automated Forklifts
Narrow aisle (VNA) cantilever setups now feature induction wire or magnetic floor tracks. High-lift multidirectional and articulated sideloaders travel along these tracks at higher speeds with zero mast sway, cutting required aisle clearance from 4.5 meters down to under 2.2 meters.
Advanced Hot-Dip Galvanization for Outdoor Yards
Industrial timber and pipe suppliers are moving long-span storage outdoors to free up insulated indoor space. Modern systems combine automated post-fabrication hot-dip galvanizing (ISO 1461) with heavy roof trusses to protect stored goods from rainfall and sun exposure.
Real-Time Load & Deflection Sensor Telemetry
Smart racking installations now feature strain-gauge telemetry embedded directly into critical cantilever pivot joints. These sensors warn warehouse operations managers if an arm experiences shock impacts or static loads that exceed design thresholds.
Why Source from Guangzhou Heda Shelves Co., Ltd.
Guangzhou Heda Shelves Co., Ltd. has specialized in industrial racking engineering, automated warehousing systems, and custom mezzanine fabrication since 2001. Operating from a 30,000 m² factory in Guangzhou, China, our manufacturing line integrates precision multi-station roll-forming lines, automated punch presses, robotic welding stations, and an environmentally compliant powder coating facility.
Every cantilever project starts with an engineering assessment. Our technical team works from your site CAD files, evaluating slab thickness, concrete compressive strength, local seismic classifications, and your forklift fleet specs. We supply detailed 3D load diagrams, finite element analysis (FEA) reports, and clear assembly documentation before the first beam is cut, giving global logistics operators predictable installation timelines and verified structural performance.
Frequently Asked Questions on Cantilever Storage
Essential structural and commercial considerations for operations managers, procurement heads, and warehouse planners.
Transform Your Warehouse Floor Layout
Send our Guangzhou engineering team your facility floor plan, target load specifications, and handling machinery profiles. We will deliver a comprehensive 2D CAD layout, 3D structural rendering, and line-item quotation within 24 hours.
Inquire Now