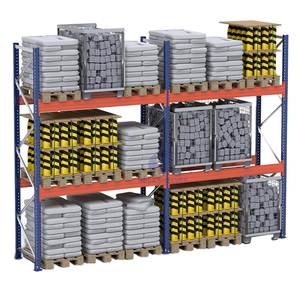
Corrosion Protected
Cold-rolled steel with electrostatic coating; multi-point hook connectors; engineered for corrosive coastal hubs.
View Product Specs
Manufactured under CE and ISO 9001:2015 standards in Guangzhou, China. Each system is custom-configured for seismic resilience, floor-load stability, and maximum volumetric utilization.
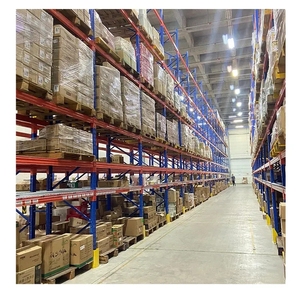
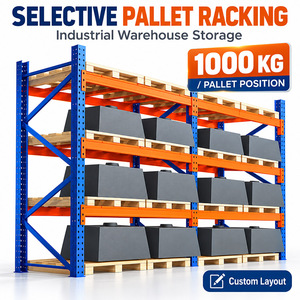
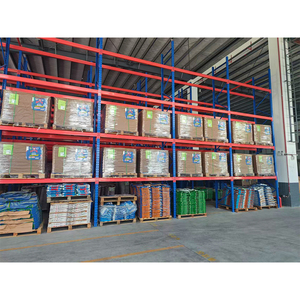
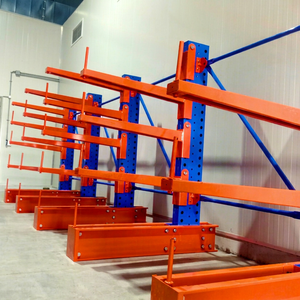
In modern supply chain engineering, real estate cost per square meter and energy tariffs for temperature-controlled facilities have driven warehouse operators to re-evaluate conventional static selective racking. As China's premier manufacturer and exporter of heavy-duty storage infrastructures, Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves) provides industrialized movable pallet racking systems (also referred to technically as Electric Mobile Racking or Powered Mobile Pallet Systems) that eliminate fixed access aisles, condensing storage density by up to 80% to 100% compared to conventional selective racking, while maintaining 100% random selectivity to every single pallet location.
Key Kinematic Concept: Instead of dedicating 60% of floor area to underutilized forklift transit aisles, a movable pallet racking system places conventional heavy-duty superstructure bays atop electronically controlled, heavy-duty mobile chassis carriages. Guided by precision-machined floor rails embedded into the concrete slab, carriages glide laterally at controlled speeds (typically 4.5 to 5.5 m/min) via distributed variable frequency drives (VFD), opening a dynamic access aisle exactly where picking or replenishment is commanded.
Export-grade movable pallet racking manufactured by HEDA Shelves integrates multi-layered electro-mechanical fail-safe architectures compliant with international safety standards, including EN 15095 (Power-operated mobile racking and shelving safety requirements) and CE Directives 2006/42/EC. Each mobile carriage is built with welded cold-formed box sections and equipped with dual-flanged forged steel wheels driven by synchronized helical gear motors.
Floor safety is enforced via optoelectronic photoelectric light curtains and dual-zone safety laser scanners positioned at the foot of each mobile base. If a forklift operator, warehouse picker, or fallen carton breaches the active aisle corridor while the mobile bases are in transit, the PLC emergency circuit activates immediate regenerative motor braking, cutting movement in under 0.2 seconds and preventing crush injuries or equipment damage. Furthermore, aisle-face emergency stop cords and manual override switches ensure that line operators have immediate mechanical control at all times.
| Engineering Parameter | Electric Movable Pallet Racking | Standard Selective Pallet Racking | Drive-In Pallet Racking | VNA (Very Narrow Aisle) Racking |
|---|---|---|---|---|
| Volumetric Space Utilization | 85% – 90% of total cube | 35% – 42% of total cube | 65% – 75% of total cube | 55% – 65% of total cube |
| Direct Pallet Selectivity | 100% Immediate Random Access | 100% Immediate Random Access | LIFO (Poor SKU Selectivity) | 100% Immediate Random Access |
| Aisle Requirement | Single Dynamic Floating Aisle | One Fixed Aisle Every 2 Rows | Dedicated Drive-In Lanes | Continuous Narrow Fixed Aisles |
| Cold Storage Energy Efficiency | Ultra-High (40% less cooling cost) | Low (High cooling per pallet) | Moderate (High thermal mass) | Moderate |
| Structural Standards Compliance | EN 15095 / EN 15512 / ISO 9001 | RMI / AS 4084 / FEM 10.2.02 | RMI / FEM 10.2.07 | FEM 10.2.02 / DIN 18202 |
| Capital Investment ROI | 18 – 28 Months (Driven by rent/cold OPEX) | Base Baseline | 36 – 48 Months | 30 – 42 Months |
How geopolitical pressures, cold-chain modernization, dark warehousing, and zero-carbon steel mandates are reshaping capital expenditure decisions across cross-border procurement teams.
With electricity costs soaring globally, cold store operators in Europe, the Middle East, and Southeast Asia are prioritizing movable racking to minimize refrigerated building cubic volumes. By packing 90% more frozen goods into the same footprint, refrigeration compressor runtime and thermal leakage drop dramatically, yielding lower OPEX and carbon tax liabilities.
Movable pallet racking is moving away from purely manual pendant or RF remote activation. Modern procurement requires PLC controllers to natively integrate via API with Warehouse Management Systems (WMS) and autonomous mobile robots (AMRs), opening dynamic aisles in advance of autonomous forklift arrival to build true "lights-out" distribution centers.
Global buyers in earthquake-prone zones—including Japan, the Philippines, Chile, Turkey, and New Zealand—now mandate dynamic finite element seismic simulations. Procurement specs require movable chassis with anti-tip mechanical latches and base accelerometers that auto-lock carriages during initial seismic shock waves.
Selecting an industrial storage supplier in China requires rigorous evaluation of engineering authenticity, fabrication infrastructure, and export reliability. Founded in 2001 and headquartered in Guangzhou, Guangzhou Heda Shelves Co., Ltd. has grown to encompass a modernized 30,000 square meter production complex with an annual fabrication capacity exceeding 360,000 metric tons of certified structural steel racking.
Full CE certification (No. 2435-CPR-8605159) and audited ISO 9001:2015 Quality Management certification (No. 18624Q00169R0M). Every upright profile and weldment undergoes documented non-destructive testing (NDT).
We do not outsource critical processes. From automated high-speed rolling mills and multi-head continuous punching to submerged arc robotic welding, dual-stage pickling, phosphating, and electrostatic powder coating, quality control is direct and uncompromised.
Export packaging is engineered for high-cube (40HQ) containers. Uprights, heavy chassis, and drive motors are nested in customized steel cradles with moisture-barrier wrapping, eliminating transit deformation across trans-oceanic routes.
Every movable racking system exported by HEDA Shelves adheres to a closed-loop fabrication cycle: (1) Mill-certified Q235B/Q355B coil spectrometer verification; (2) CNC precision slitting and sizing; (3) Automated continuous upright punch pressing; (4) Multi-stand cold-roll bending for high moment of inertia; (5) Precision robotic connector welding; (6) Surface shot-blasting and mechanical scale removal; (7) 8-stage chemical pickling and phosphating for rust inhibition; (8) Automated electrostatic polyester thermoset powder curing at 200°C; (9) Factory pre-assembly testing of motorized chassis drive trains; (10) Barcode bundling, load-testing verification, and ocean container export pack-out.
Critical engineering, floor slab, electrical, and customs insights directly answered by HEDA Shelves chief structural engineers.
Movable pallet racking exerts concentrated point loads through steel guide wheels onto the concrete slab. Warehouses typically require a reinforced concrete slab thickness of 200mm to 300mm with a minimum compressive strength of C25/30 or C30/37. Floor flatness must comply with DIN 18202 Table 3 Group 4 or EN 15620 tolerances to prevent carriage wheel drag or uneven load transfer across motorized drive axles. HEDA Shelves provides customized slab load distribution calculations and embedded rail leveling templates for your local civil contractors.
For greenfield facilities, rails are set during the secondary screed pour using precision leveling screws and turnbuckles to guarantee exact elevation. In existing warehouses, specialized diamond-blade slot trenching is performed to saw-cut channels into the existing slab. Rails are positioned, micro-leveled using optical transit levels, secured with high-tensile anchors, and grouted with non-shrink high-early-strength epoxy mortar. Both top-mount flush rails and sunken profile options are engineered to allow unhindered standard forklift cross-traffic.
Yes. HEDA Shelves engineers specialized low-temperature cold store packages. These feature IP65-rated drive motors, low-temperature synthetic food-grade lubricants that resist thickening down to -35°C, internal anti-condensation heating elements inside main PLC cabinets, polyurethane or cryogenic alloy steel guide wheels to eliminate cold-brittleness fracture, and dual-layer hot-dip galvanized or zinc-rich epoxy coated steel structural bases.
Each movable racking cluster is outfitted with an uninterruptible power supply (UPS) for control circuitry, allowing safe emergency stoppage. For extended blackouts, systems feature manual mechanical brake releases on each gear motor. Operators can use a manual ratchet crank or tow-bar coupling to manually roll open an aisle, ensuring that perishable goods or urgent picking operations are never held hostage to grid power disruptions.
Every shipment is delivered with comprehensive English engineering drawings, color-coded component tagging, wiring schematics, and high-definition installation video tutorials. For large-scale projects across North America, Europe, the Middle East, Southeast Asia, and South Asia, HEDA Shelves dispatches seasoned field engineers to manage mechanical assembly, rail grouting oversight, and electrical PLC commissioning alongside your local installation crews.
Even when accounting for international sea freight and import duties, procuring heavy-duty movable racking from HEDA Shelves Guangzhou typically yields an overall project cost savings of 25% to 40% compared to European or domestic North American rack fabricators. Our massive steel consumption contracts, automated robotic production, and optimized ocean shipping bundle designs deliver unmatched commercial advantages without sacrificing structural steel mill test certification standards.
Contact our senior structural engineering team for a complimentary CAD warehouse layout, 3D simulation rendering, and full project quotation within 24 hours. Let us engineer your ideal high-density storage solution.