Export-Ready Industrial Racking & High-Density Dynamic Systems
Precision-manufactured with premium Q235B cold-rolled structural steel, certified under strict European conformity norms, and optimized for maximum cube-utilization in distribution centers, cold chain facilities, and manufacturing plants.
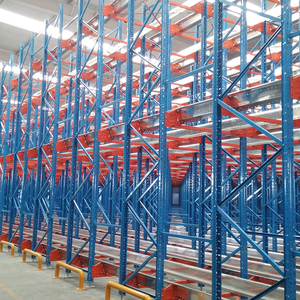
High Density Radio Shuttle Pallet Racking System
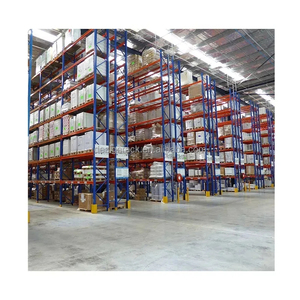
5-Layer Custom Heavy Duty Steel Beam Selective Rack
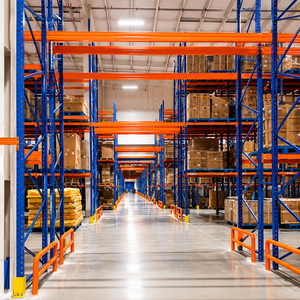
Modular 2000kg Heavy Duty Pallet Rack System
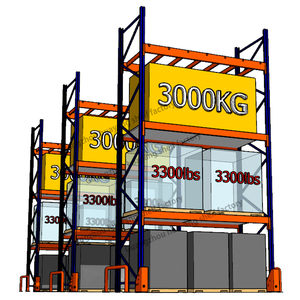
CE Certified 5-Layer Anti-Corrosion VNA Pallet Rack
Custom Industrial Storage Metal Stacking Units
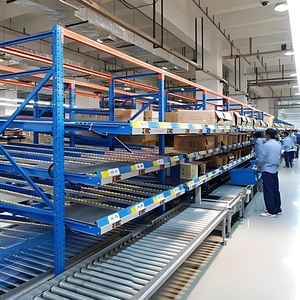
Adjustable Wheel Track Carton Flow Picking Rack
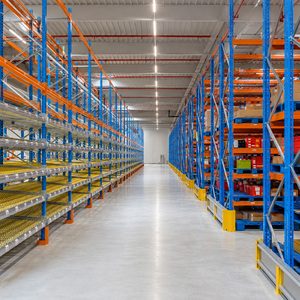
Q235B Porta Paletes Storage Racks for 3PL Hubs
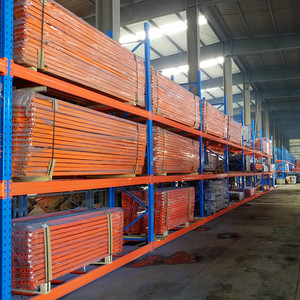
Conventional Q235 Steel Pallet Rack (500-1500kg)
Technical Whitepaper: Engineering Criteria for CE Certified Mobile Shelving Systems
In modern supply chain architecture, static storage aisles represent dead floor space that inflates operational overhead. Conventional selective pallet racking allocates between 55% to 65% of total warehouse surface area strictly to access aisles for material handling equipment. CE certified mobile shelving and heavy-duty motorized racking systems resolve this fundamental inefficiency by mounting entire structural rack banks onto electronically synchronized, rail-guided mobile carriages. By opening a single working aisle on demand via computerized radio control or warehouse management system (WMS) integration, mobile shelving achieves up to an 85% to 100% increase in storage capacity within identical facility footprints.
Guangzhou Heda Shelves Co., Ltd. approaches mobile system manufacturing through rigorous metallurgical validation. Utilizing premium cold-formed Q235B and Q355B structural steel, our uprights are roll-formed via continuous multi-stage rolling lines with continuous hole-punch indexing. The upright cross-section utilizes multi-bend omega profiling, delivering an exceptional section modulus and resistance to torsional buckling. Floor tracks are machined from high-tensile steel rails with leveled anchor grout beds aligned within DIN 18202 Class 3 structural slab flatness tolerances.
Rail-Guided Kinetic Carriages
Fabricated from heavy hollow structural sections (HSS) and C-channels, our mobile carriages feature integrated wheel assemblies with self-aligning spherical roller bearings. Independent gearmotor drives deliver soft-start, frequency-inverted acceleration to eliminate pallet tipping during carriage traverse.
EN 15095 Optical Safety Array
Operator safety is paramount. Every motorized aisle incorporates multi-point category 4 optical light curtains, photoelectric safety beams across carriage skirts, floor-level trip wires, and manual emergency e-stops. Any beam obstruction halts carriage motion in under 0.2 seconds.
PLC Automation & WMS Dispatch
Integrated Siemens or Omron central logic controllers coordinate aisle movement via wireless handheld terminals or direct automated forklift dispatch. Modes include aisle ventilation positioning, night parking, cold-store circulation, and fire-alarm automatic aisle opening.
Future Procurement Trends in High-Density Mobile & Industrial Racking
As industrial real estate costs escalate across global hubs, procurement directors are shifting from static capital equipment purchases to highly integrated, energy-efficient dynamic kinetic storage architectures.
Deep-Freeze Thermal Energy Optimization
In cold chain storage (-25°C to -30°C), cooling an empty static aisle represents massive operational power leakage. Mobile racking slashes the refrigerated room volume by up to 45%, cutting refrigeration compressor electricity demand by over 30% per stored pallet position.
Hybrid AGV / AMR Dynamic Interfacing
Modern mobile racks are abandoning purely manual controls in favor of machine-to-machine (M2M) API protocols. Autonomous Mobile Robots and automated reach forklifts wirelessly instruct the mobile carriage to open the required picking face en route to pallet drop-off.
Decarbonized Steel & Eco Pretreatment
Tier-1 procurement mandates now demand verified low-carbon supply chains. HEDA utilizes recyclable structural steel paired with non-toxic zirconium and phosphate chemical pretreatment baths and zero-VOC heavy-duty thermoset powder finishes.
Seismic-Damped Foundation Engineering
Dynamic storage systems in seismic activity zones require specialized base anchoring and dissipation couplings. Structural modeling accounts for ground acceleration vectors, preventing resonant amplification across tall dynamic mobile racks.
System Architecture Comparison Matrix
Evaluate space footprint utilization, accessibility constraints, and operational velocity across major warehouse storage topologies to determine optimal project feasibility.
| Storage System Topology | Floor Footprint Efficiency | Direct SKU Selectivity | Required Aisle Width | Operational Turnover Mode | Best Suited Application |
|---|---|---|---|---|---|
| CE Mobile Pallet Shelving | 85% – 95% (Maximum) | 100% (On-Demand Aisle) | Single Floating Aisle (~3.0m) | FIFO or LIFO Selectable | Cold storage, archival vaults, 3PL, pharma |
| Selective Pallet Racking | 40% – 50% (Standard) | 100% (Instant Direct) | 3.2m – 3.8m (Every Bay) | Pure FIFO/LIFO Universal | High-turnover multi-SKU FMCG fulfillment |
| Drive-In Storage Racks | 65% – 75% (High) | 15% – 20% (Lane Bound) | Internal Drive Lanes | Strict LIFO (FIFO with Drive-thru) | Bulk homogeneous goods, beverage plants |
| Radio Shuttle System | 75% – 85% (Very High) | Deep Lane Bound | Dedicated Transfer Aisles | Automated FIFO / LIFO | High-volume cold stores, dairy, food buffers |
| Very Narrow Aisle (VNA) | 60% – 70% (High Vertical) | 100% (Instant Direct) | 1.5m – 1.8m (Fixed Rail/Wire) | Universal Fast Turnover | High-bay warehouses with extreme ceiling height |
Manufacturer Credibility: Guangzhou Heda Shelves Co., Ltd.
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized roll-forming facility into a globally renowned manufacturer and exporter of heavy-duty industrial storage racks, automated radio shuttle systems, structural mezzanines, and CE certified mobile shelving systems. Our manufacturing complex spans over 30,000 square meters in Guangzhou, South China, staffed by over 300 experienced engineers, structural designers, precision welders, and export quality-assurance specialists.
In-House 10-Stage Precision Manufacturing Workflow
Raw Steel Auditing
Certified prime Q235B/Q355B coil testing for tensile yield strength and chemical composition.
CNC Roll-Forming
Continuous cold roll-forming with multi-station precision profile tooling for structural uprights.
Robotic Welding
Automated MIG welding fixtures for beam end connectors, carriage frames, and base plates.
Surface Pretreatment
Multi-stage immersion: degreasing, acid pickling, rust removal, phosphating, and deionized rinses.
Powder Coating & QC
Electrostatic thermoset polyester curing at 200°C for superior corrosion and scratch resistance.
To assist international EPC contractors, factory owners, and logistics directors, HEDA Shelves provides comprehensive, complimentary engineering deliverables prior to contract execution: full 2D CAD warehouse layout blueprints, 3D structural BIM models, pallet position optimization calculations, and certified slab point-load distribution charts. Our container packing protocols utilize custom steel strapping, dense bundle blocking, and waterproof shrink film wrap to guarantee zero shipping deformation upon ocean arrival across major discharge hubs including Nhava Sheva (JNPT), Mundra, Chennai, Colombo, Chattogram, Karachi, and Rotterdam.
Frequently Asked Questions: Technical Sourcing & Compliance
Key technical, structural, and logistical questions answered directly by HEDA Shelves senior applications engineering team.
Accelerate Your Storage Efficiency with CE Certified Engineering
Connect directly with HEDA Shelves application engineers. Submit your warehouse dimensions, clear ceiling heights, and pallet specifications to receive a complimentary custom 2D CAD layout, 3D parametric rendering, and formal project quotation within 24 hours.