CE · ISO 9001
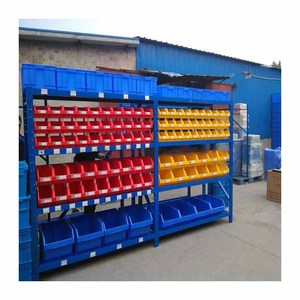
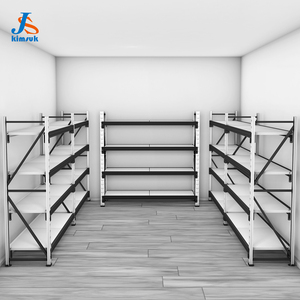
Mracking Popular Multi-level Light Duty Storage Bin Rack
Load: 100-300 kg/tier
Manual Picking
Discover factory-direct, CE-certified storage configurations precision-manufactured for high-bay operations, 3PL logistics hubs, cold chain facilities, and automated distribution centres.
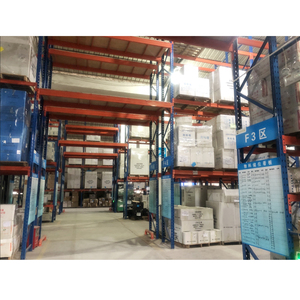
Guangzhou HEDA Shelves Co., Ltd. controls the entirety of downstream steel cold-roll forming, robotic automated welding, and specialized surface passivations. We ensure complete metallurgical integrity from coil unrolling to containerized dispatch.
Factory audits are backed by independent CE marking (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 registration (18624Q00169R0M). Every batch is tested for yield point deflection and cyclic stress capacity.
Established in 2001, our facility encompasses over 30,000 m² of smart shop-floor manufacturing in Guangzhou, staffed by 300+ structural engineers, precision mechanics, and certified QA technicians.
Equipped with continuous cold-roll forming profile lines, high-speed CNC punching presses, and multi-axis welding robots, our operations guarantee consistent delivery timelines for mega-scale industrial hubs globally.
Our in-house design office delivers compliant warehouse layout calculations, 3D structural visualisations, and finite element analyses (FEA) within 24 hours, optimizing volumetric space before contract signing.
Structural rack failures stem from inferior strip steel and sub-standard surface passivations. Discover how our proprietary 10-stage manufacturing sequence guarantees structural stability under intense cyclical loading.
Certified high-tensile Q235B / Q355B hot-rolled coils undergo spectral chemical and yield analysis.
Automated uncoiling, flattening, and high-precision cross-slitting with dimensional tolerances under ±0.5mm.
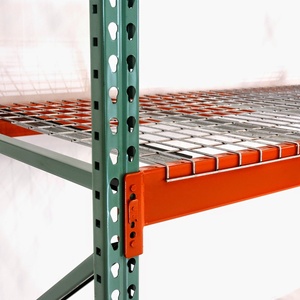
Automated continuous multi-station punching for exact 50mm, 75mm, or 76.2mm teardrop hole pitches.
18-to-24 station roll-forming tooling beds gradually fold steel without inducing internal residual stresses.
Precision calibration of omega profiles, double-C box beams, and step-beam geometries for tight tolerance seating.
Mechanical edge rounding and robotic deburring eliminate micro-cracks and rough contact edges.
Multi-axis MIG/MAG robotic welding workstations bond beam end-connectors with uniform weld penetration.
Pre-treatment with acid pickling and immersion phosphating removes all scale to ensure permanent coating adhesion.
Electrostatic powder deposition cured in continuous 200°C tunnels creates a resilient, anti-scratch 60–80μm film.
Destructive batch testing, pallet-bundling, and export sea-container loading optimization.
Modern warehousing has shifted from static square footage to dynamic, automated volume utilization. Strategic supply chain planners must account for these three structural disruptions when procuring industrial storage.
Rising labor expenses, occupational health regulations, and the expansion of SKU profiles are rapidly rendering manual forklift aisle transits obsolete. Modern fulfillment networks favor deep-lane automated pallet shuttles and Automated Storage & Retrieval Systems (ASRS).
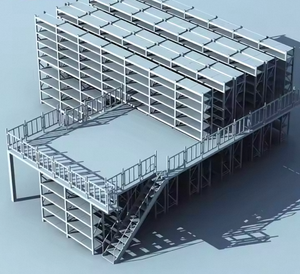
Escalating industrial real estate rents and tight land availability are driving facility operators to expand upwards rather than outwards. Rack-supported mezzanine platforms leverage vertical clear heights without requiring municipal building permits for new construction.
Global logistics hubs in coastal regions, high-humidity climates, and active seismic fault zones demand sophisticated engineering calculations. Specifiers are moving away from light-duty catalogue racks toward certified, site-specific structural designs.
Compare our main industrial storage racking systems across key engineering parameters, including selectivity, storage density, required material handling equipment (MHE), and capital expenditure ratings.
| Storage System Type | Pallet Selectivity | Volumetric Density | Stock Rotation | Typical MHE Handling | Optimal Industry Application |
|---|---|---|---|---|---|
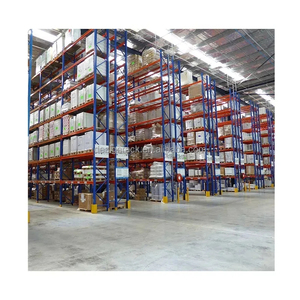
| Selective Pallet Racking | 100% Immediate Direct | Moderate (35-40%) | FIFO / LIFO Arbitrary | Counterbalance / Reach Truck | General Retail DCs, Multi-SKU 3PL, FMCG |
| Drive-In / Drive-Through | Low (Lane-Restricted) | High (65-75%) | LIFO (Drive-In) / FIFO | Counterbalance Forklift | Cold Storage, Seasonal Harvest, Beverage Bottlers |
| Radio Shuttle System | Medium (Channel-Based) | Very High (80-85%) | Programmed FIFO / LIFO | Reach Truck + Smart Cart | Pharmaceutical Cold Chain, Meat & Seafood Freezers |
| Push-Back Gravity Cart | Medium (2–6 Deep) | High (60-70%) | Strict LIFO | Standard Reach Forklift | Buffer Storage, Fast Moving Consumer Goods |
| Heavy-Duty Cantilever | 100% Frontal Open | High for Linear Goods | Direct Unrestricted | Side-Loader / Multi-Directional | Structural Steel, Extruded PVC Pipes, Timber, Coil |
| Rack-Supported Mezzanine | 100% Split-Level | Maximum Vertical Yield | Manual Batch Picking | Pallet Jacks, Goods Lifts, Chutes | Apparel, E-Commerce Parcel Sortation, Auto Spare Parts |
Clear, definitive technical answers to assist procurement committees, facility engineers, and compliance auditors in validating overseas industrial storage investments.
Our structural components are certified under CE Certificate No. 2435-CPR-8605159, complying with European standard EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design). We supply verified mill test certificates (MTC 3.1) with each shipment, confirming steel chemistry, tensile strength, and impact tests.
We require the concrete slab thickness (minimum 150mm–200mm recommended for heavy pallet racks), compressive characteristic strength (e.g., C20/25, C25/30, or C30/37), rebar grid layout, and the floor flatness rating (DIN 18202 or TR34 FM2). This ensures baseplates and mechanical or chemical anchor bolts do not compromise the slab's shear capacity.
All cold-formed components undergo an automated 8-stage immersion pre-treatment, including degreasing, acid descaling pickling, and micro-crystalline zinc phosphating, followed by 60–80μm thermosetting polyester electrostatic powder coating. For deep cold stores or coastal open sheds, we provide hot-dip galvanizing conforming to ISO 1461.
Yes. Our teardrop pallet rack profile is engineered to match standard North American RMI (Rack Manufacturers Institute) pitch patterns. Upright punchings and beam end connectors feature standard pin-lock safety catches, ensuring full compatibility with existing teardrop installations.
Standard fabrication runs between 14 to 21 working days for typical 20GP/40HQ container loads. Uprights and beams are bundled with steel strapping, corner protectors, and heavy plastic wrap to prevent transit abrasion. We also provide container loading software diagrams to optimize unpack operations.
Yes. Along with complete component numbering, 3D exploded layout drawings, and step-by-step video installation guides, we deploy experienced overseas site installation supervisors for large-scale structural mezzanines and ASRS installations worldwide.